This short procedure reuses existing service step pages. Edit the referenced step pages to update this procedure everywhere.
WARNING
Read Safety instructions before starting. This is a full drivetrain teardown and rebuild.
- Remove the kill switch before starting any service procedure to prevent accidental motor start.
- Keep the motor shaft free of rotation during service.
- The rotor contains strong magnets — keep fingers clear of pinch points during removal and installation.
- The motor controller (PCBA) is ESD-sensitive. Handle it with care.
- Use thermal gloves when handling the heated bearing and heated motor housing.
- Follow specified torque values for all fasteners.
Required tools
See RemigoOne Go&DE2 Drivetrain Assembly and RemigoOne Go&DE2 Drivetrain Service Manual for the complete tool and part reference. This procedure uses effectively the full drivetrain tool set, including:
- 19mm Socket, T20 Torx driver, T10 Torx driver
- Die grinder (with cutting disc) (only if the shear pin is bent)
- Motor Rear Cover Remover tool (900040007)
- Radial shaft seal press (p-2401_0005_2), Radial shaft seal sleeve (p-2401_0005_1)
- Axial bearing removal tool, Bearing press (p-2401_0002_02), Bearing press (With nut)
- 7mm Socket, Side cutters
- Rotor removal tool (250010009), Rotor pedestal (p-2401_0002_01)
- Heat sink removal tool (250010008), Heat sink press tool (250010011)
- Digital caliper, Pick, Circlip pliers, 17mm open-ended wrench, Parallel jaw pliers
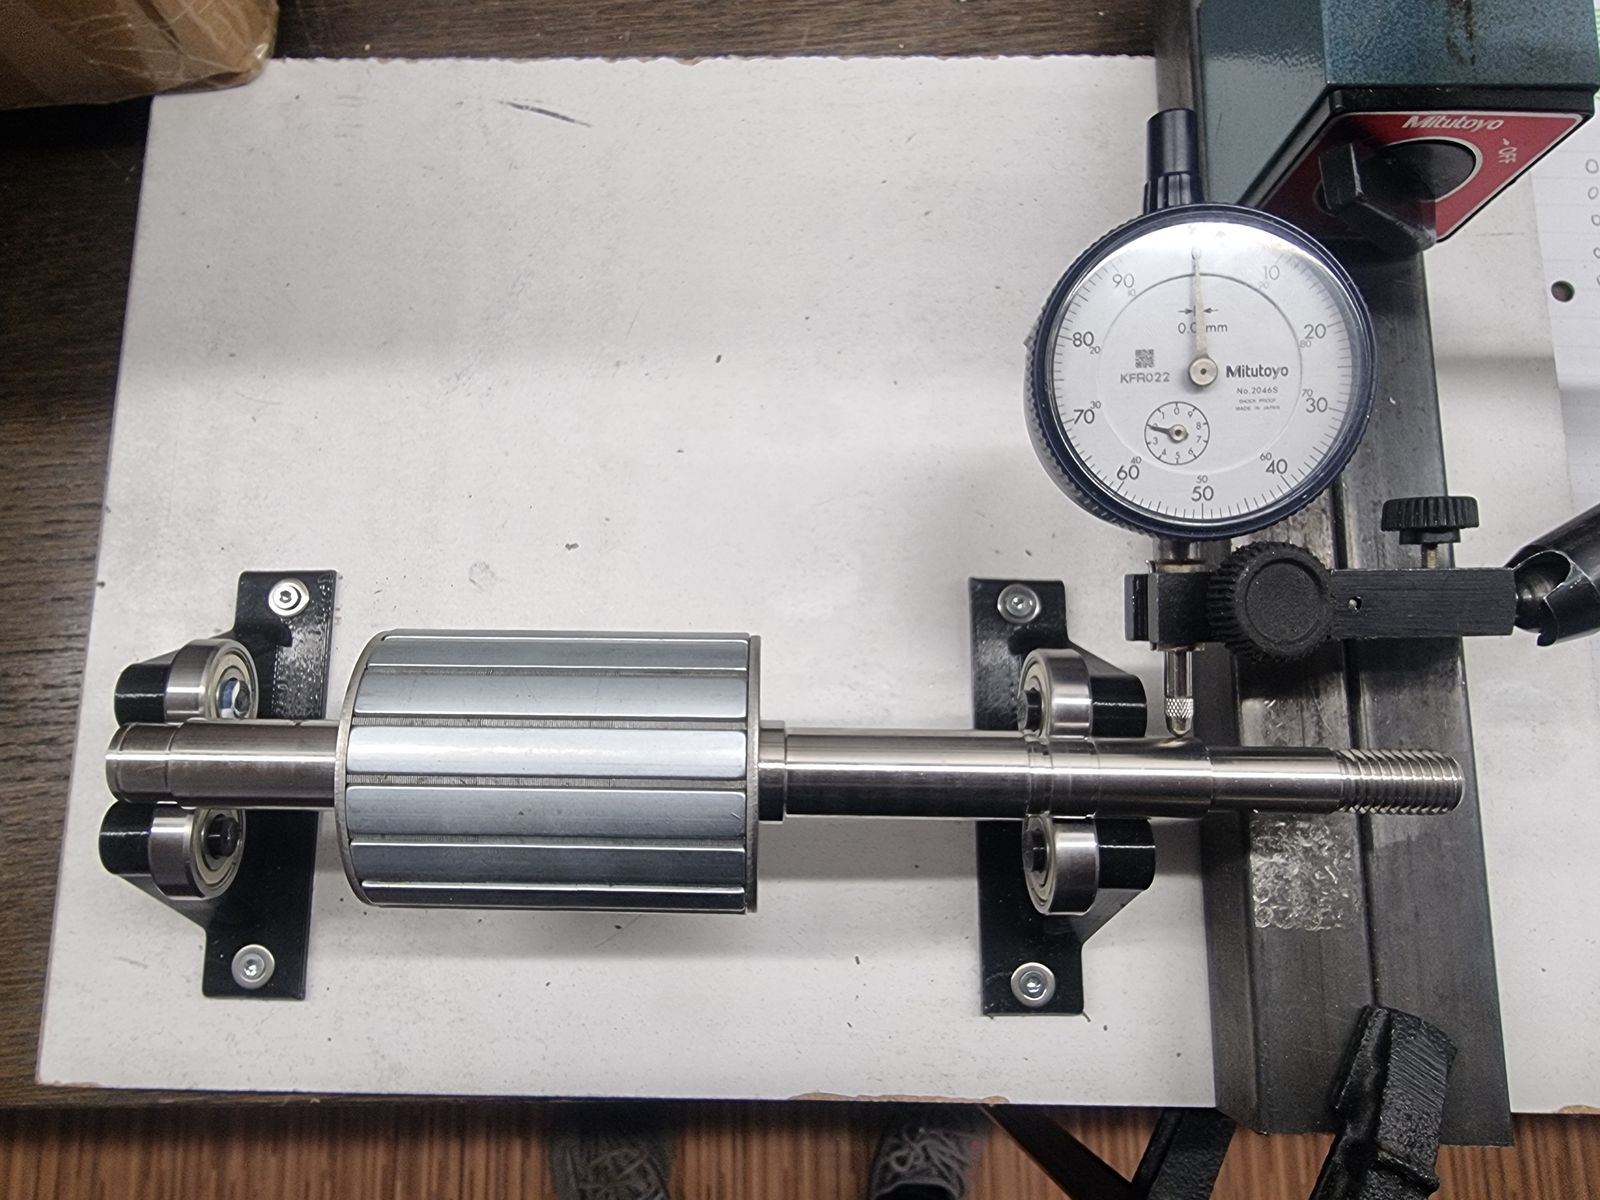
- Rotor radial tolerance gauge
Required parts and consumables
- 🗑 Bearing 6202 ZZ (013010001) (×2 — one in the housing, one on the rotor) — not reusable
- 🗑 Radial shaft seal 15x25x5 (017020001) — not reusable
- 🗑 O-ring 70x4 (017010001), O-ring 78x1 (017010004) — not reusable
- 🗑 External circlip 12 (012010004) — not reusable
- 🗑 Motor housing with stator — not reusable; new pre-assembled spare part (SKU not yet assigned, see part page)
- Rotor (100020002) — only if the removed rotor is damaged; otherwise the existing rotor is reused in the new housing
- 🗑 Wave spring washer LMKAS 35A (011030005) (RemigoOne Go) — not reusable
- 🗑 Wave spring washer 35 NSSB-0138-L2 (016040003) (RemigoOne DE2) — not reusable
- Fasteners per RemigoOne Go&DE2 Drivetrain Assembly (Screw M3/M4 series, washers)
- Permabond A130 (010010005)
- Thermal Paste Bergquist TGF 3600 (010080002)
- Silicone Dowsil 7091 (010010001), Silicone spray
- Molykote 111 Grease (010020001), Molykote O-ring grease 55 (010020003)
Disassembly
DT-DIS-001 DISASSEMBLY STEP 1 - Remove anode
Tools:
Removing parts:
Procedure:
Link to original
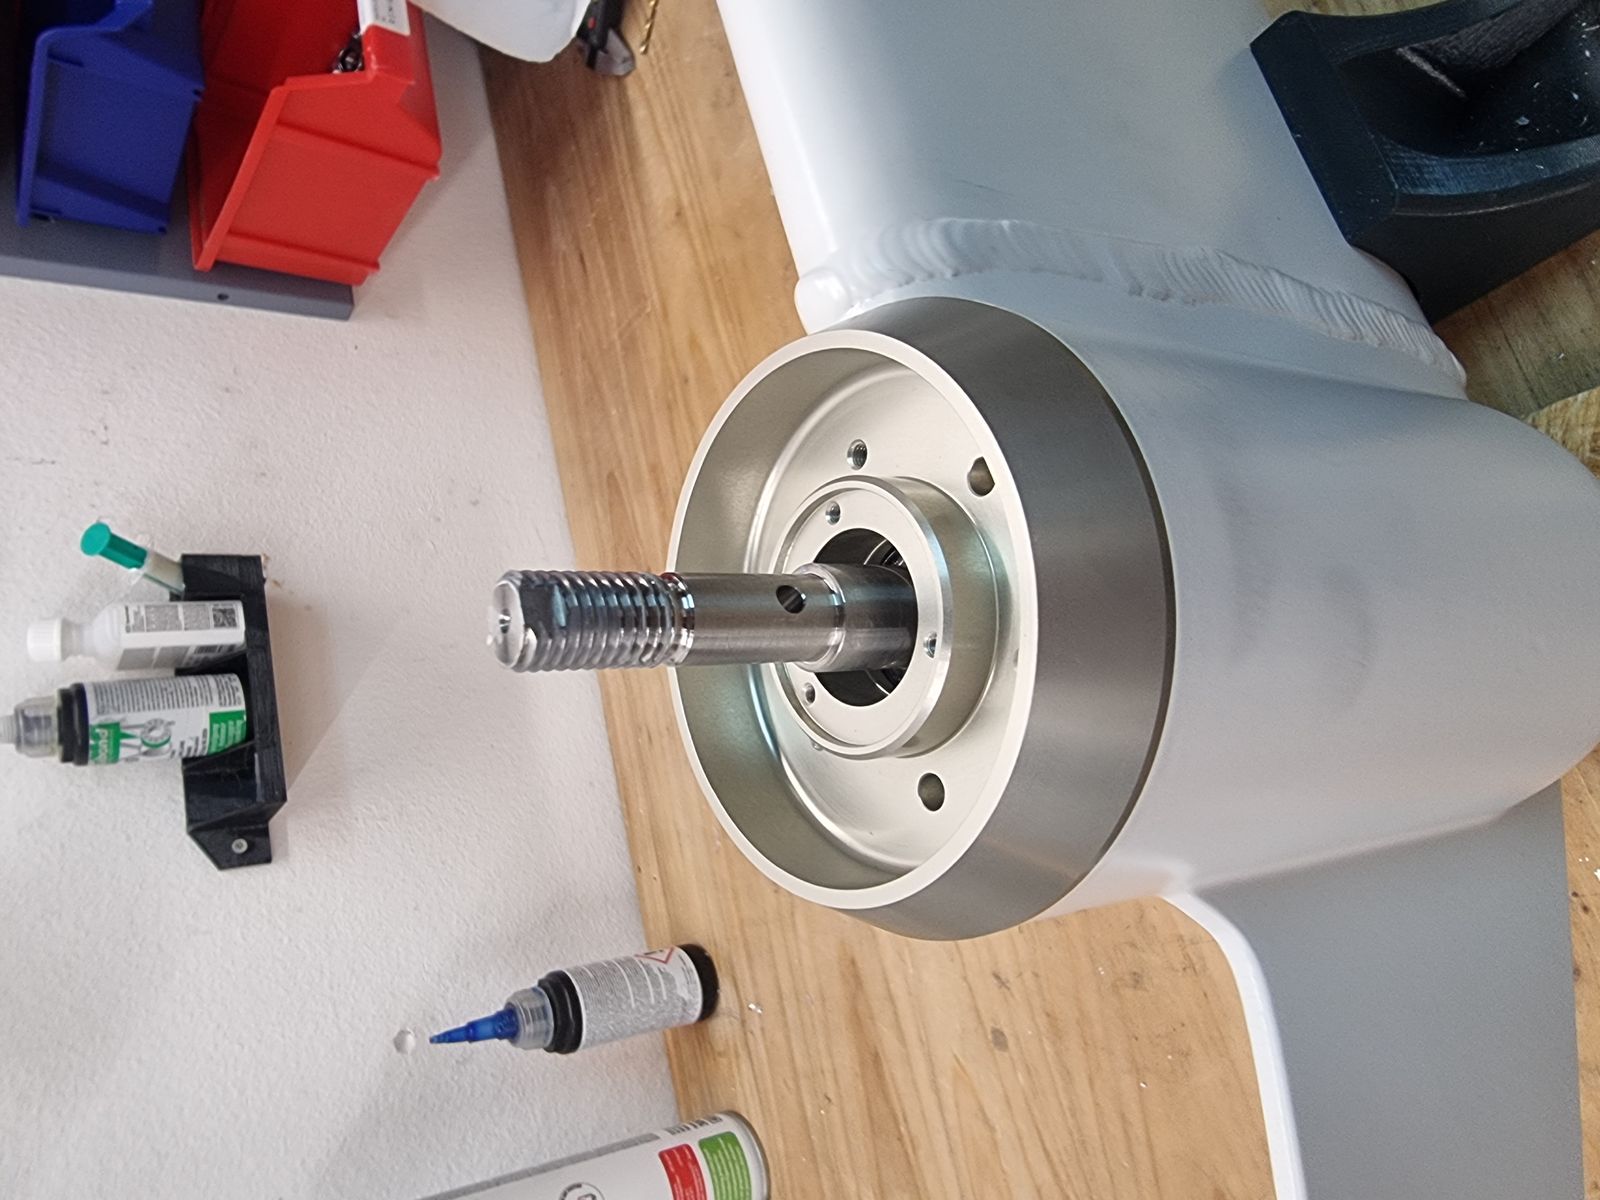
- Loosen the anode using a 19 mm socket.
- Remove the anode from the shaft.
DT-DIS-002 DISASSEMBLY STEP 2 - Remove safety nut
Tools:
Removing parts:
Procedure:
Link to original
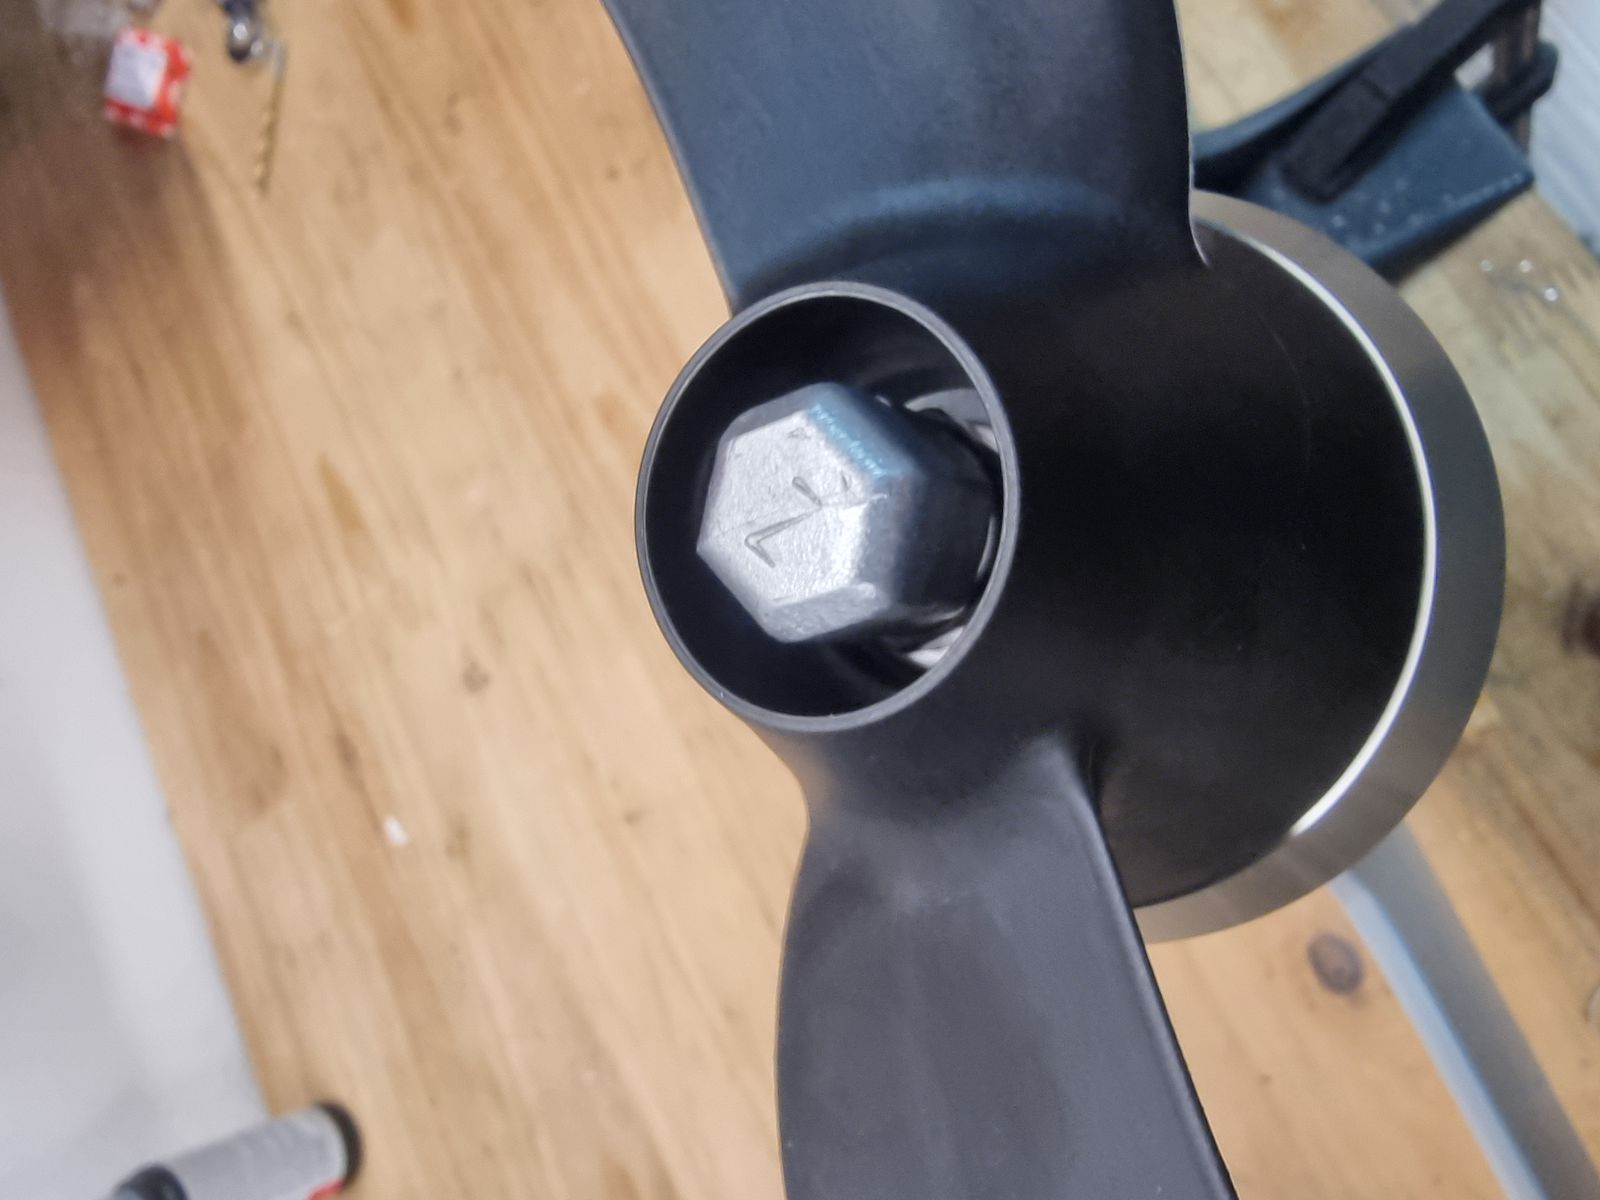
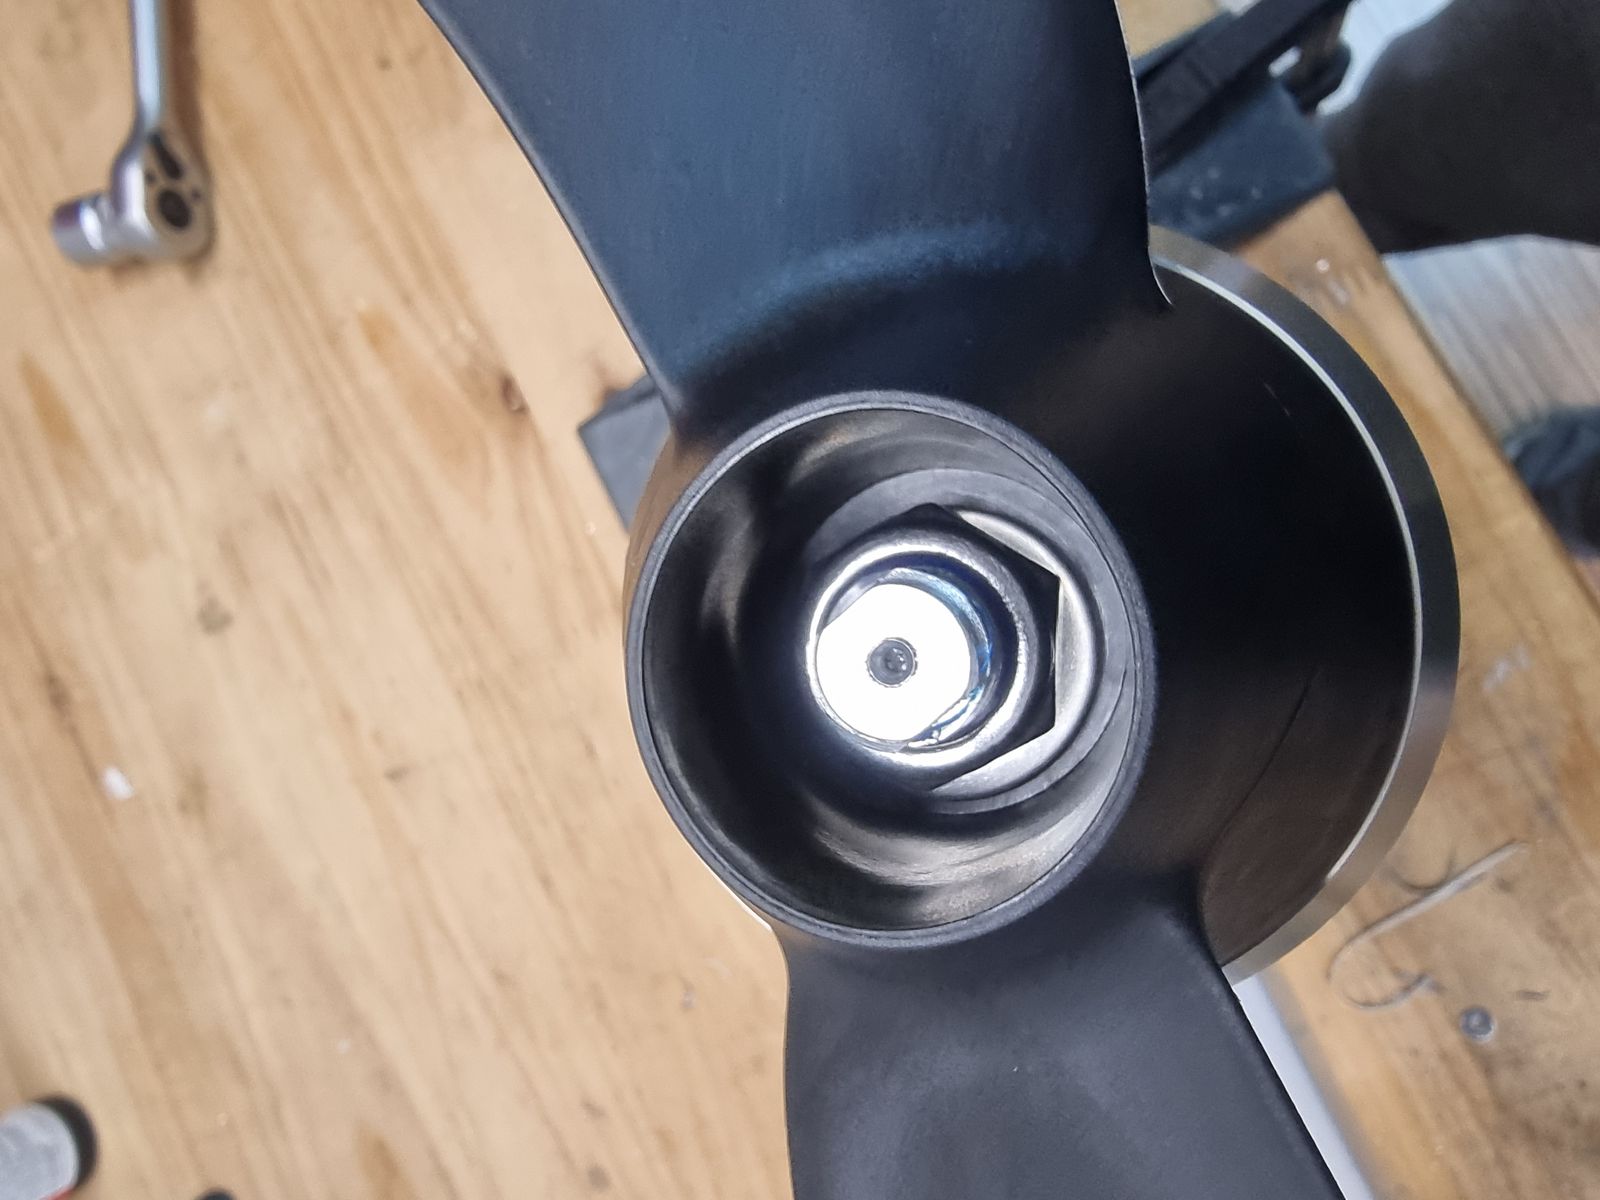
- Loosen the safety nut using a 19 mm socket.
- Remove the safety nut from the shaft.
DT-DIS-003 DISASSEMBLY STEP 3 - Remove washer and propeller
Tools:
- No tools required.
Removing parts:
Procedure:
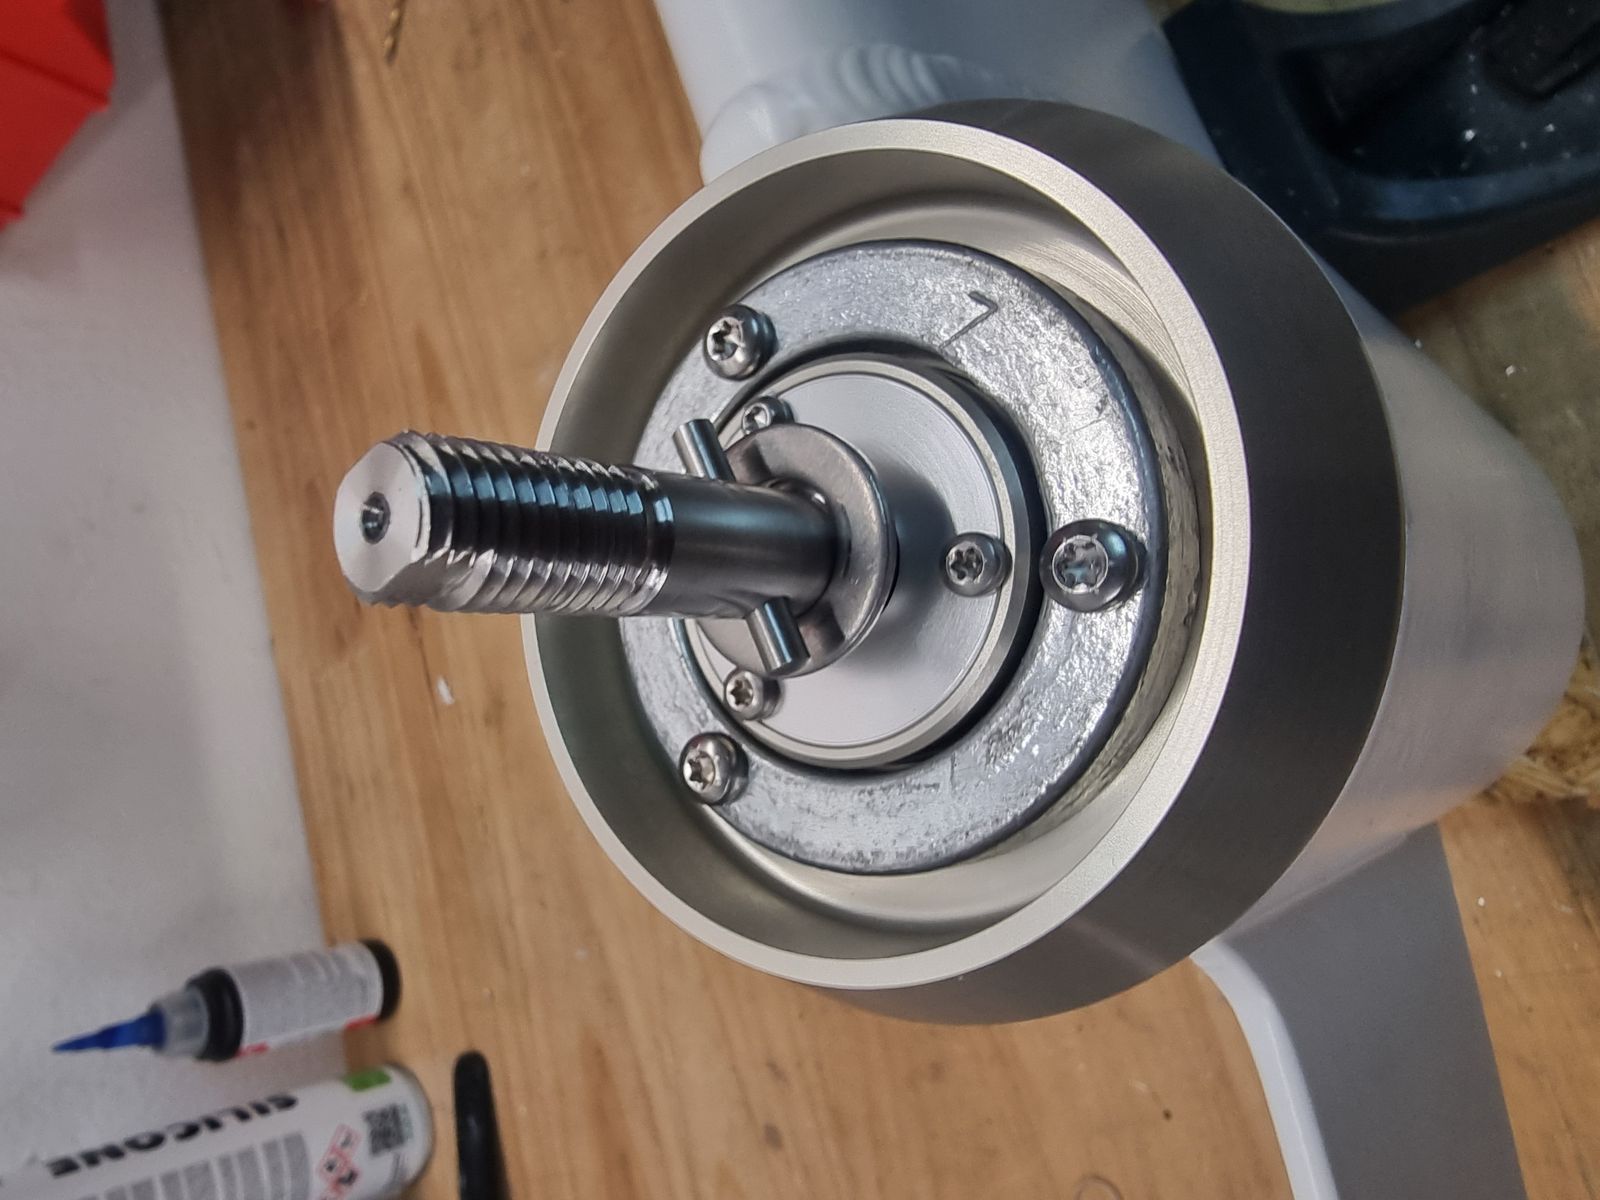
- Remove the washer from the shaft.
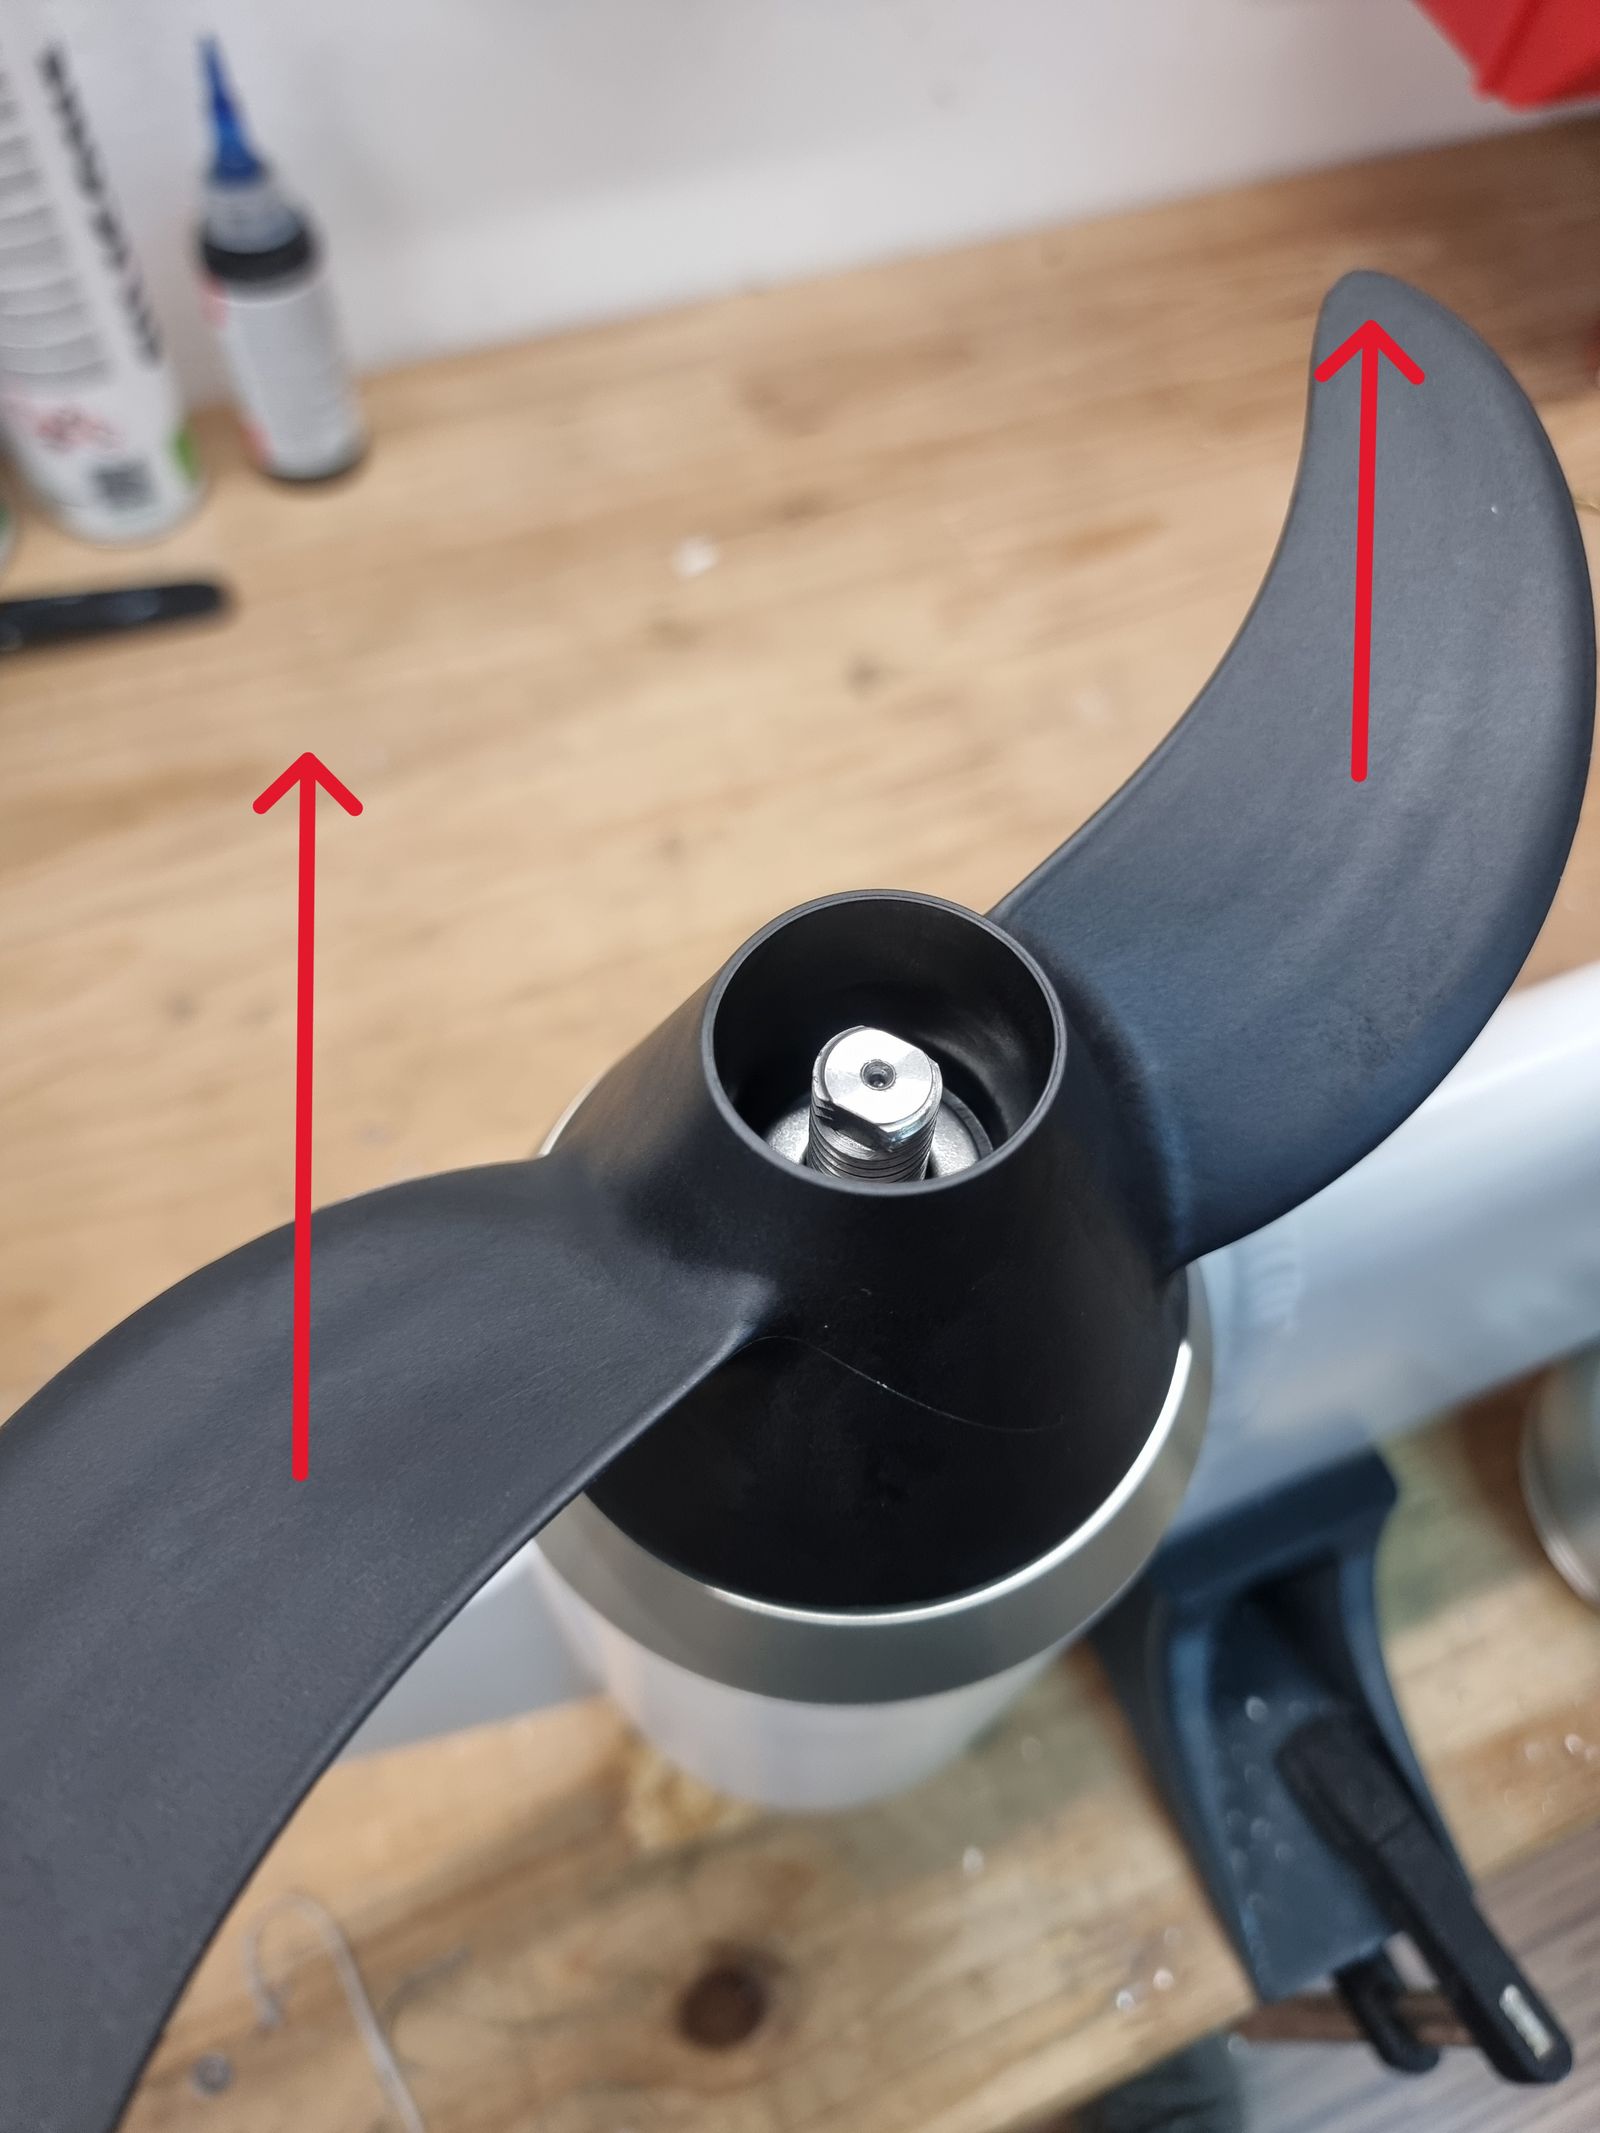
- Remove the propeller by pulling it from the propeller hub.
Link to originalCAUTION
Do not pull the propeller by only one fin. Pull evenly to avoid damaging the propeller or shaft.
DT-DIS-004 DISASSEMBLY STEP 4 - Remove shear pin and washer
Tools:
- Die grinder (with cutting disc) (only if the shear pin is bent)
Removing parts:
Procedure:
- Push the shear pin out of the shaft.
- If the shear pin is bent — for example after a sudden propeller stop — it cannot simply be pushed out. In this case, cut the shear pin with a die grinder fitted with a cutting disc instead of forcing it out.
- Remove the washer from the shaft.
Link to originalCAUTION
When cutting a bent shear pin, take great care to protect the shaft. Do not let the cutting disc contact or damage the shaft surface.
DT-DIS-005 DISASSEMBLY STEP 5 - Remove housing anode
Tools:
Removing parts:
Procedure:
Link to original
- Unscrew the anode screws using a T20 Torx driver.
- Remove the housing anode.
DT-DIS-006 DISASSEMBLY STEP 6 - Remove seal cover
Tools:
Removing parts:
Procedure:
Link to original
- Unscrew the three M3 screws using a T10 Torx driver.
- Remove the seal cover.
DT-DIS-007 DISASSEMBLY STEP 7 - Remove housing lid
Tools:
Removing parts:
Procedure:
- Install the motor rear cover remover tool on the housing lid.
- Unscrew the housing lid anticlockwise.
- Remove the housing lid.
Link to originalCAUTION
Use only the correct removal tool to avoid damaging the housing lid.
DT-DIS-008 DISASSEMBLY STEP 8 - Remove radial shaft seals
Tools:
Removing parts:
Procedure:
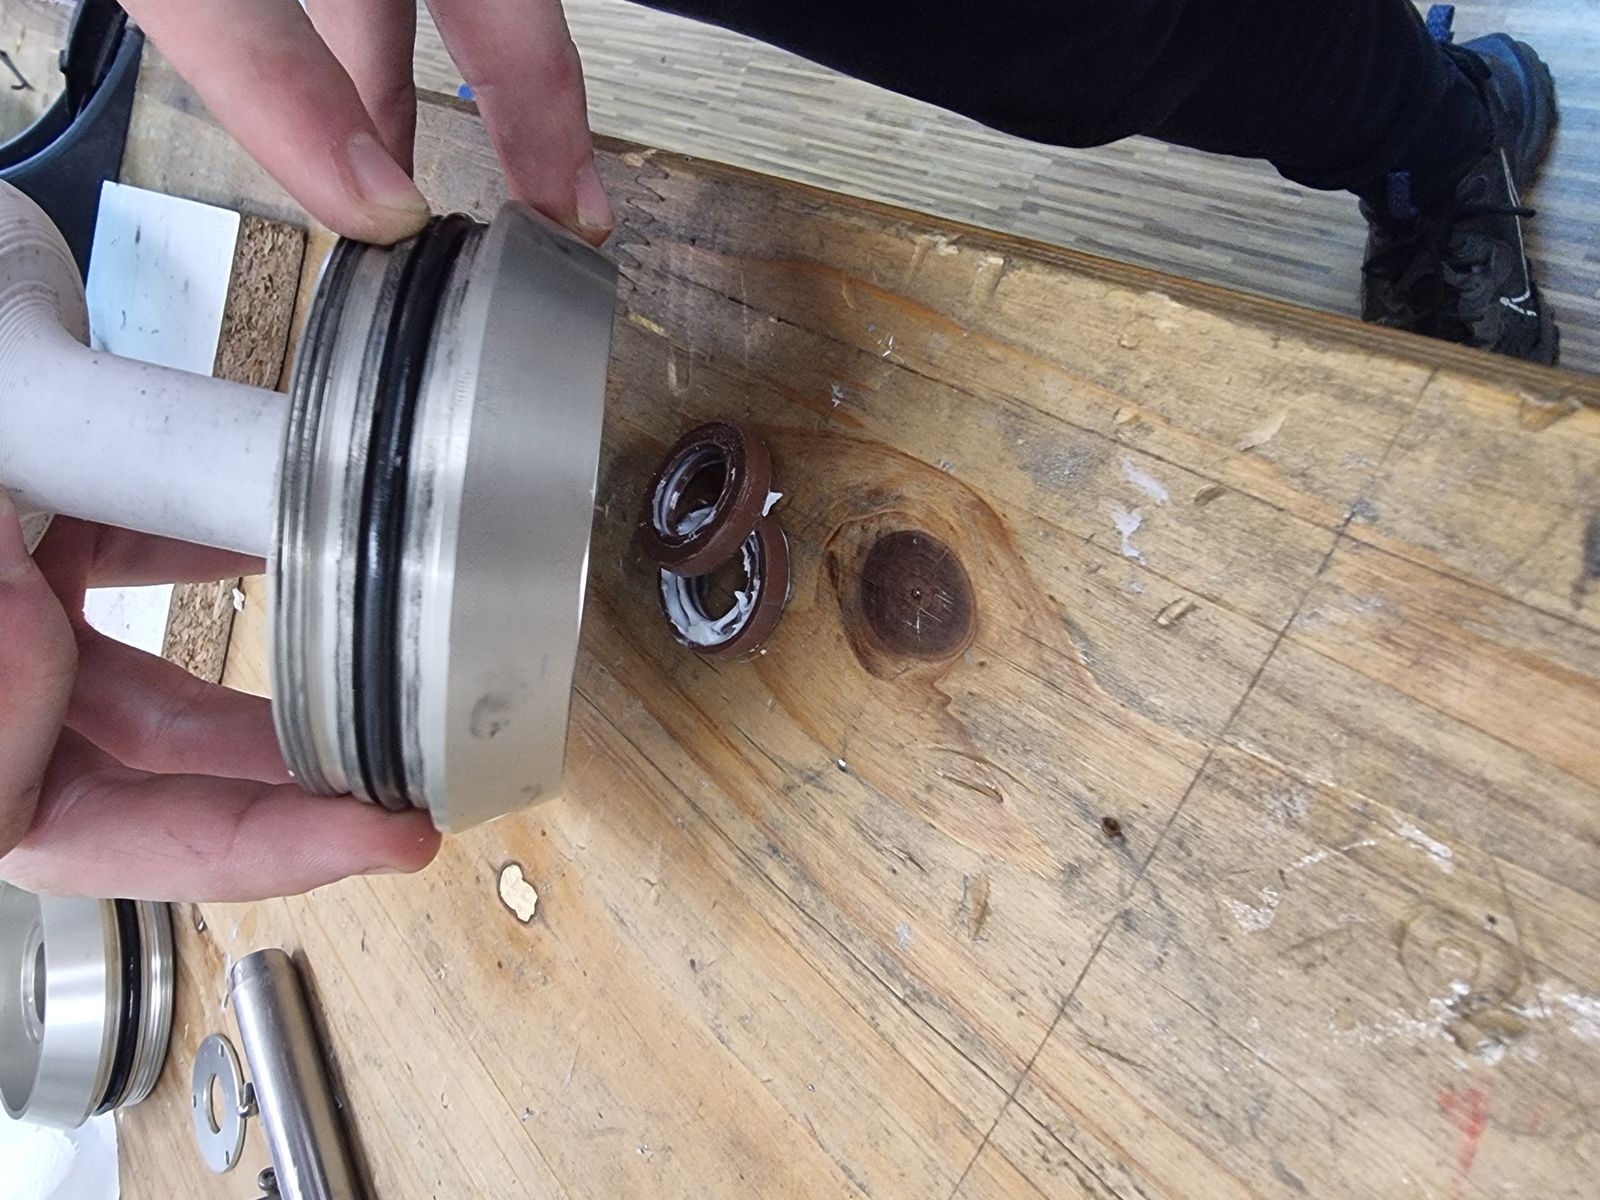
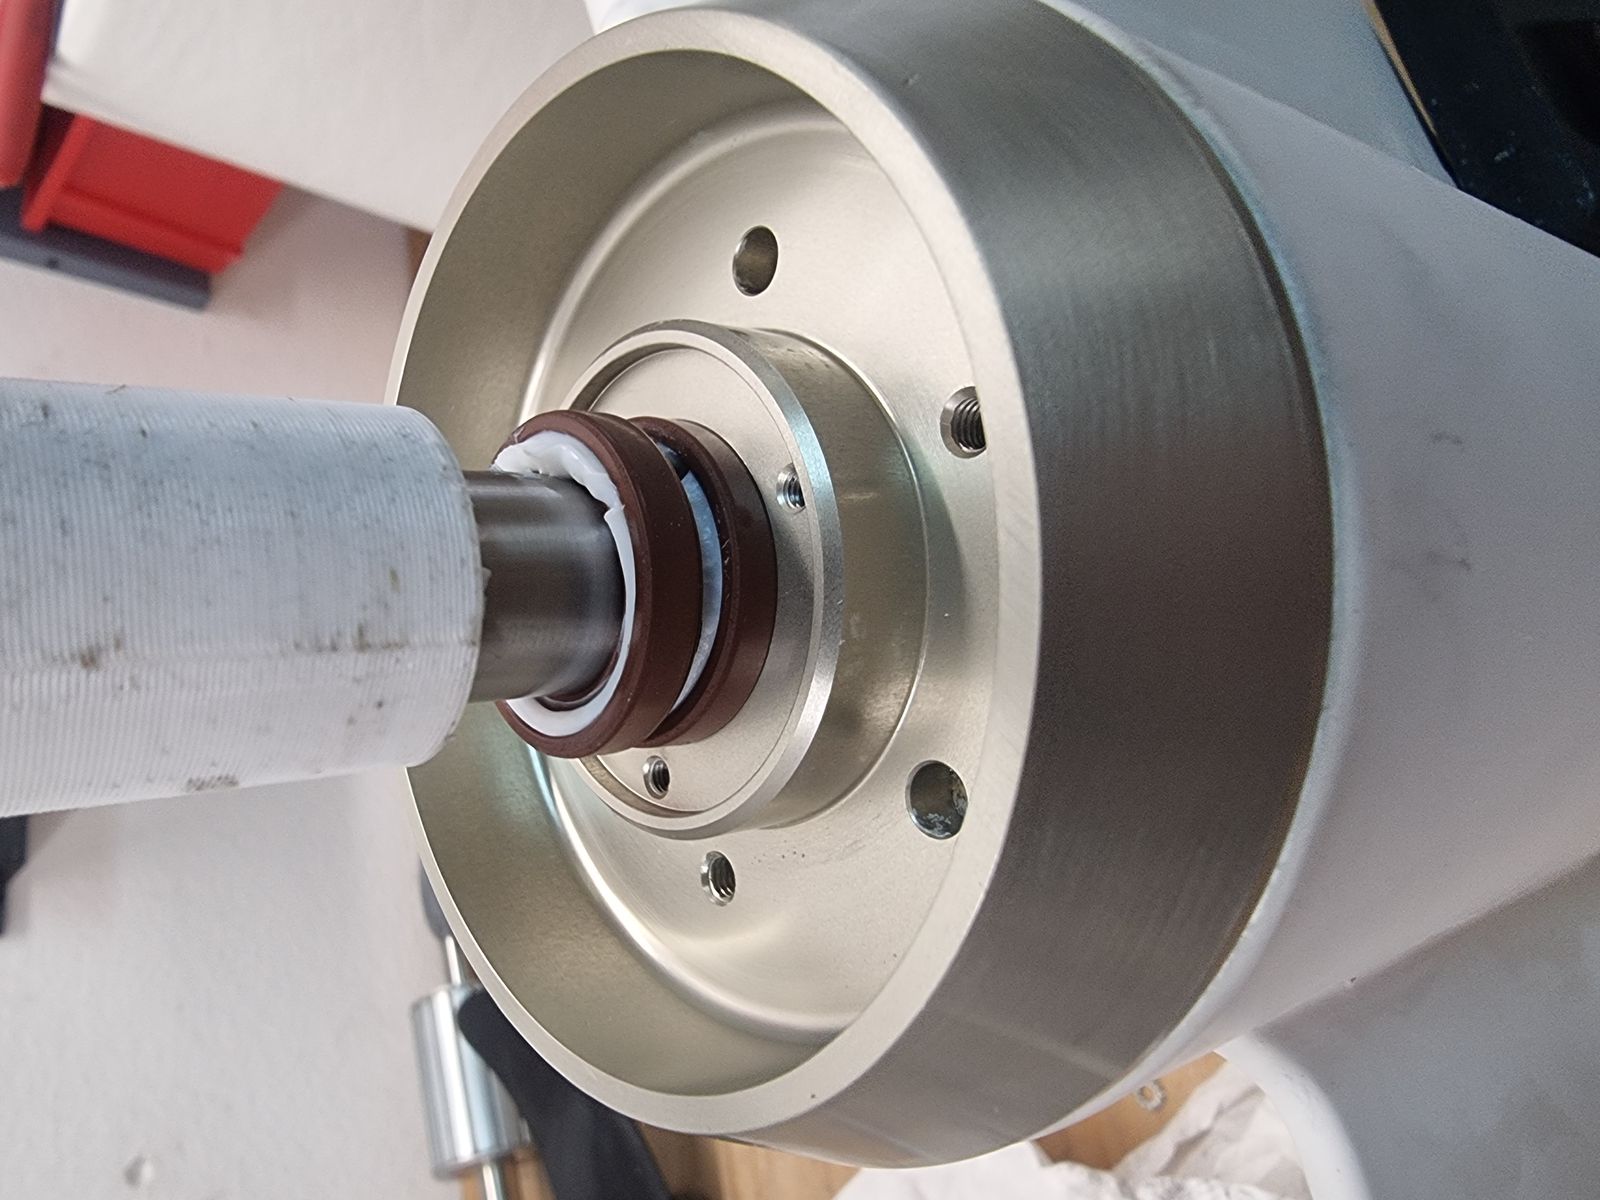
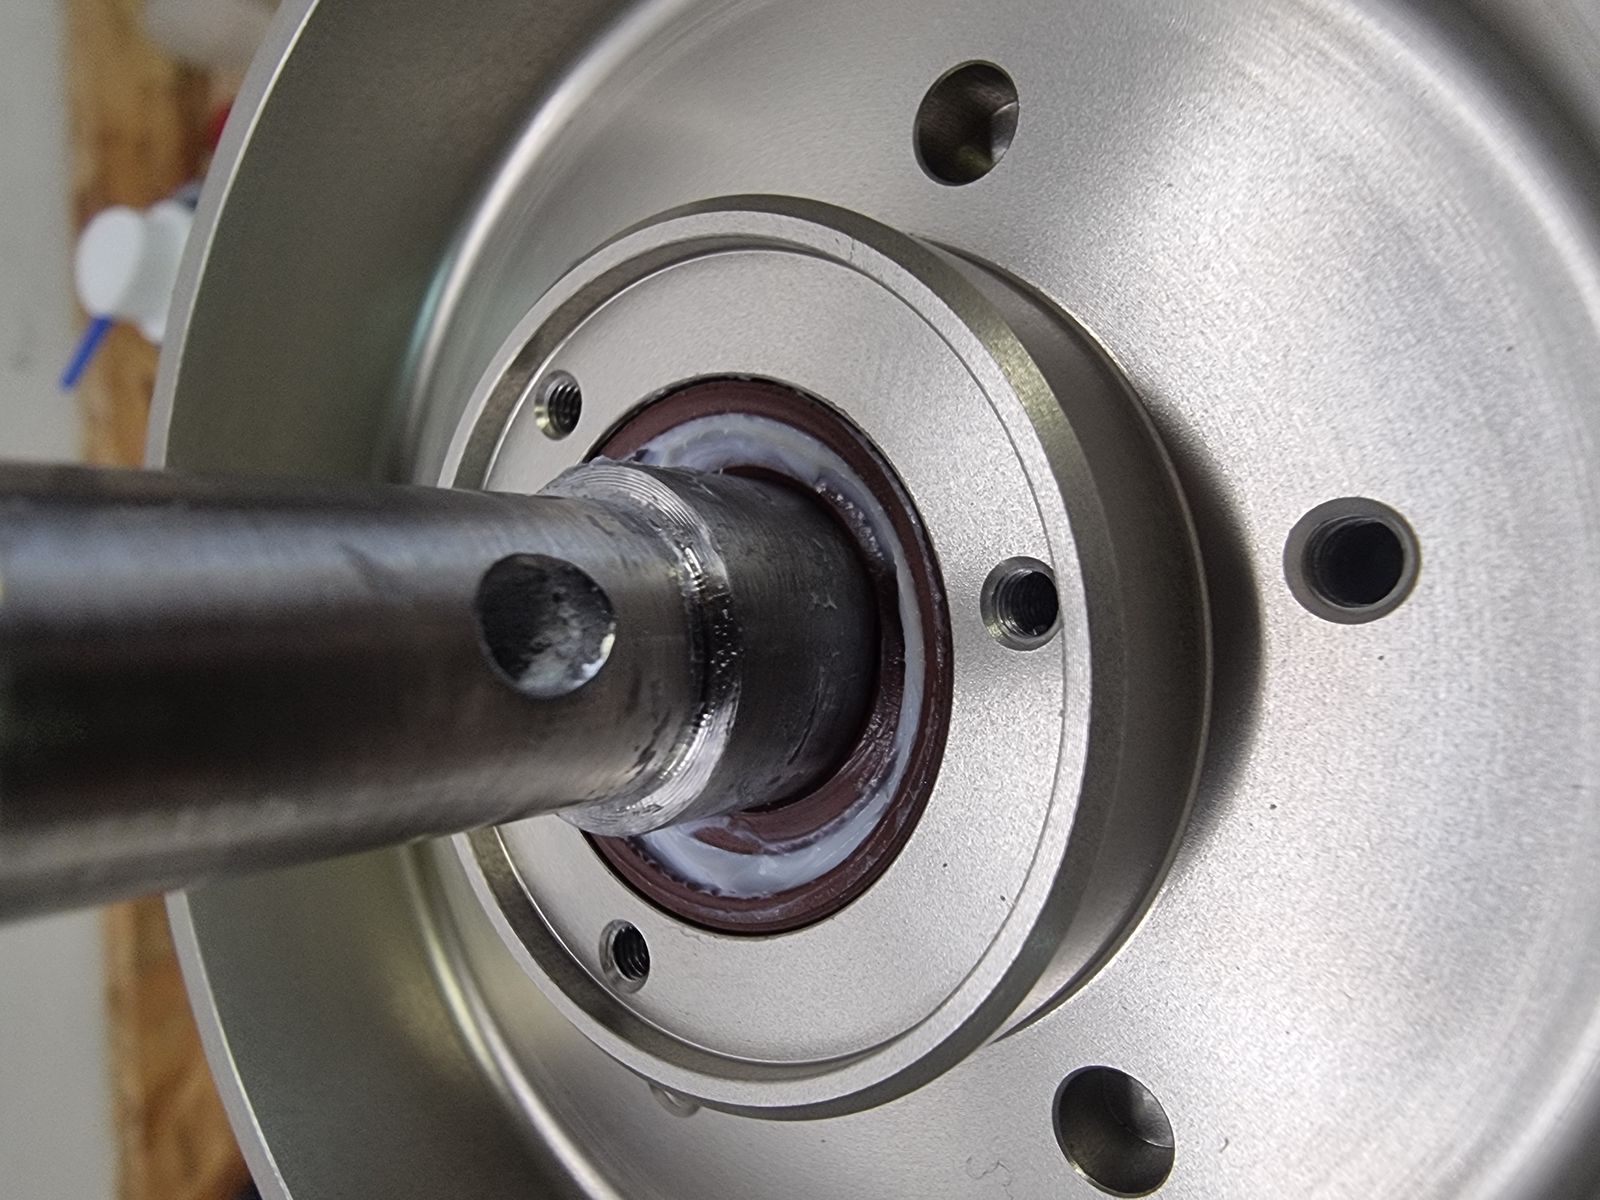
- Press on the radial shaft seals and push them out of the housing lid.
- Clean the housing lid with isopropanol.
Link to originalCAUTION
🗑 Do not reuse removed radial shaft seals. Always install new radial shaft seals during assembly.
DT-DIS-009 DISASSEMBLY STEP 9 - Remove wave spring washer
Tools:
- No tools required.
Removing parts:
- Wave spring washer LMKAS 35A (011030005) (RemigoOne Go)
- Wave spring washer 35 NSSB-0138-L2 (016040003) (RemigoOne DE2)
Procedure:
Link to original
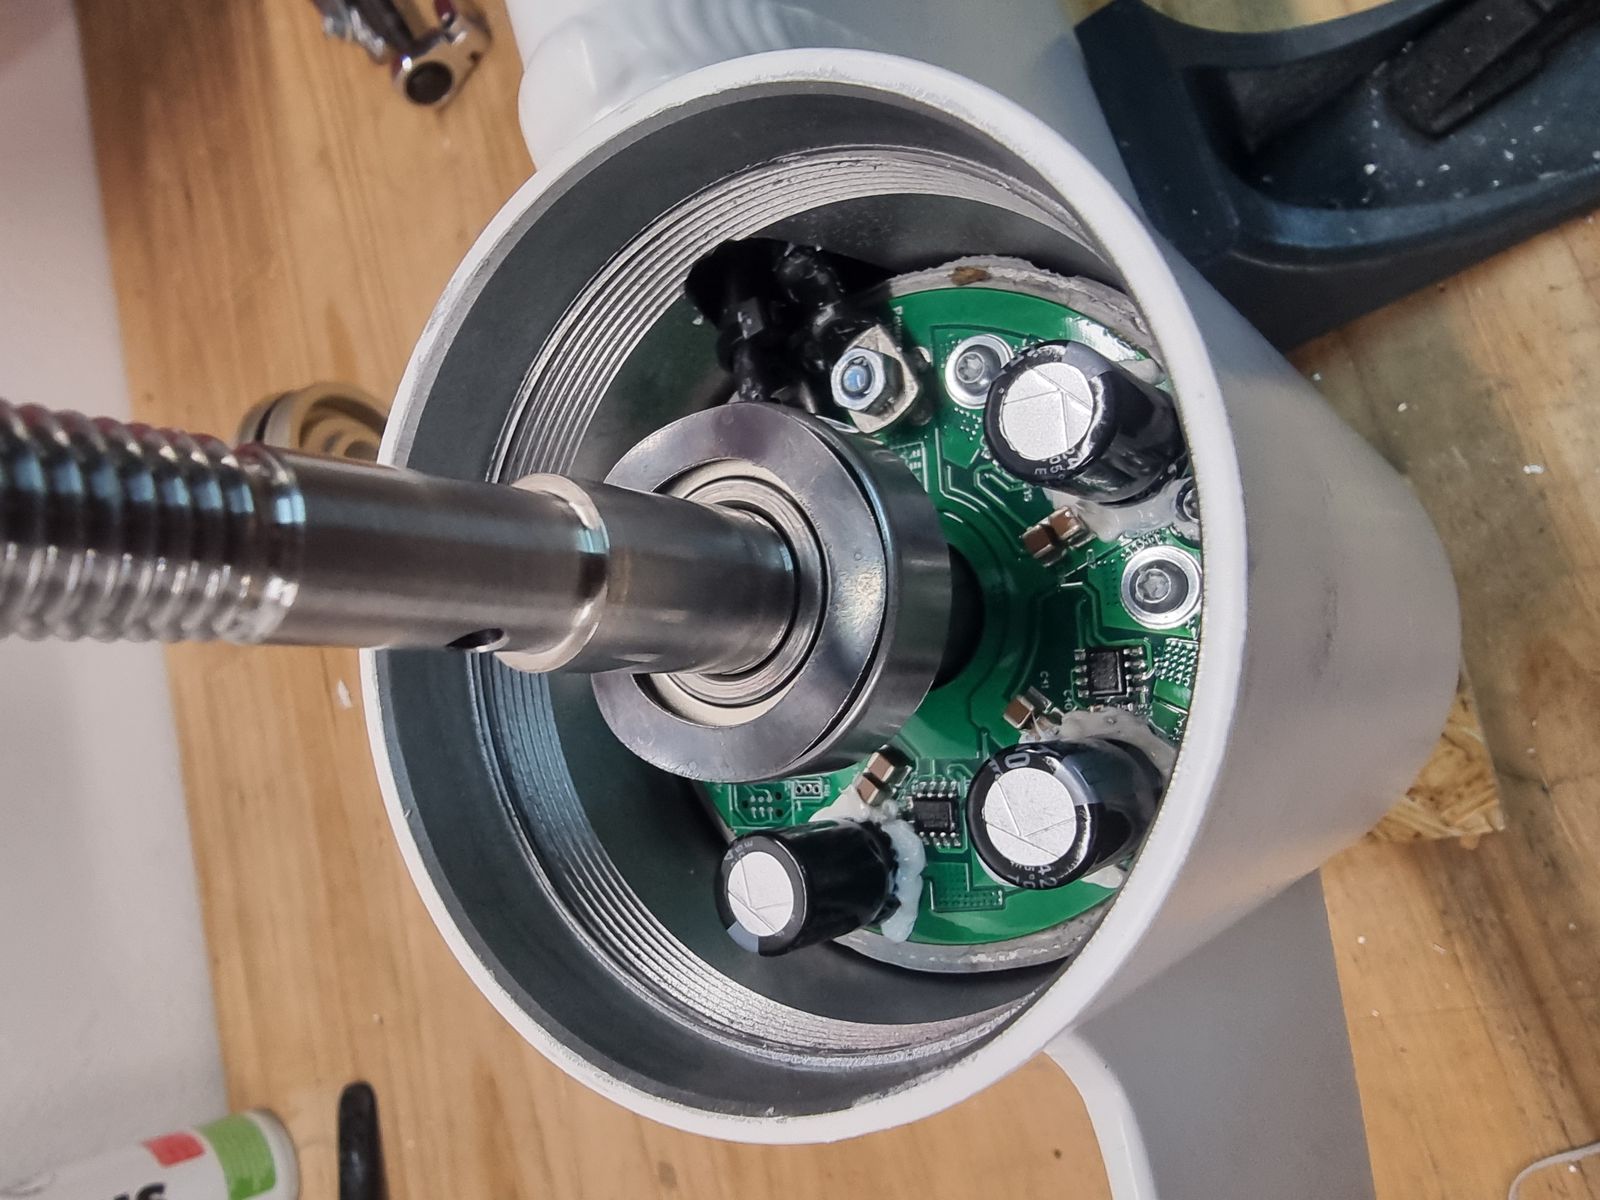
- Remove the wave spring washer.
DT-DIS-010 DISASSEMBLY STEP 10 - Remove bearing 6202 ZZ
Tools:
Removing parts:
Procedure:
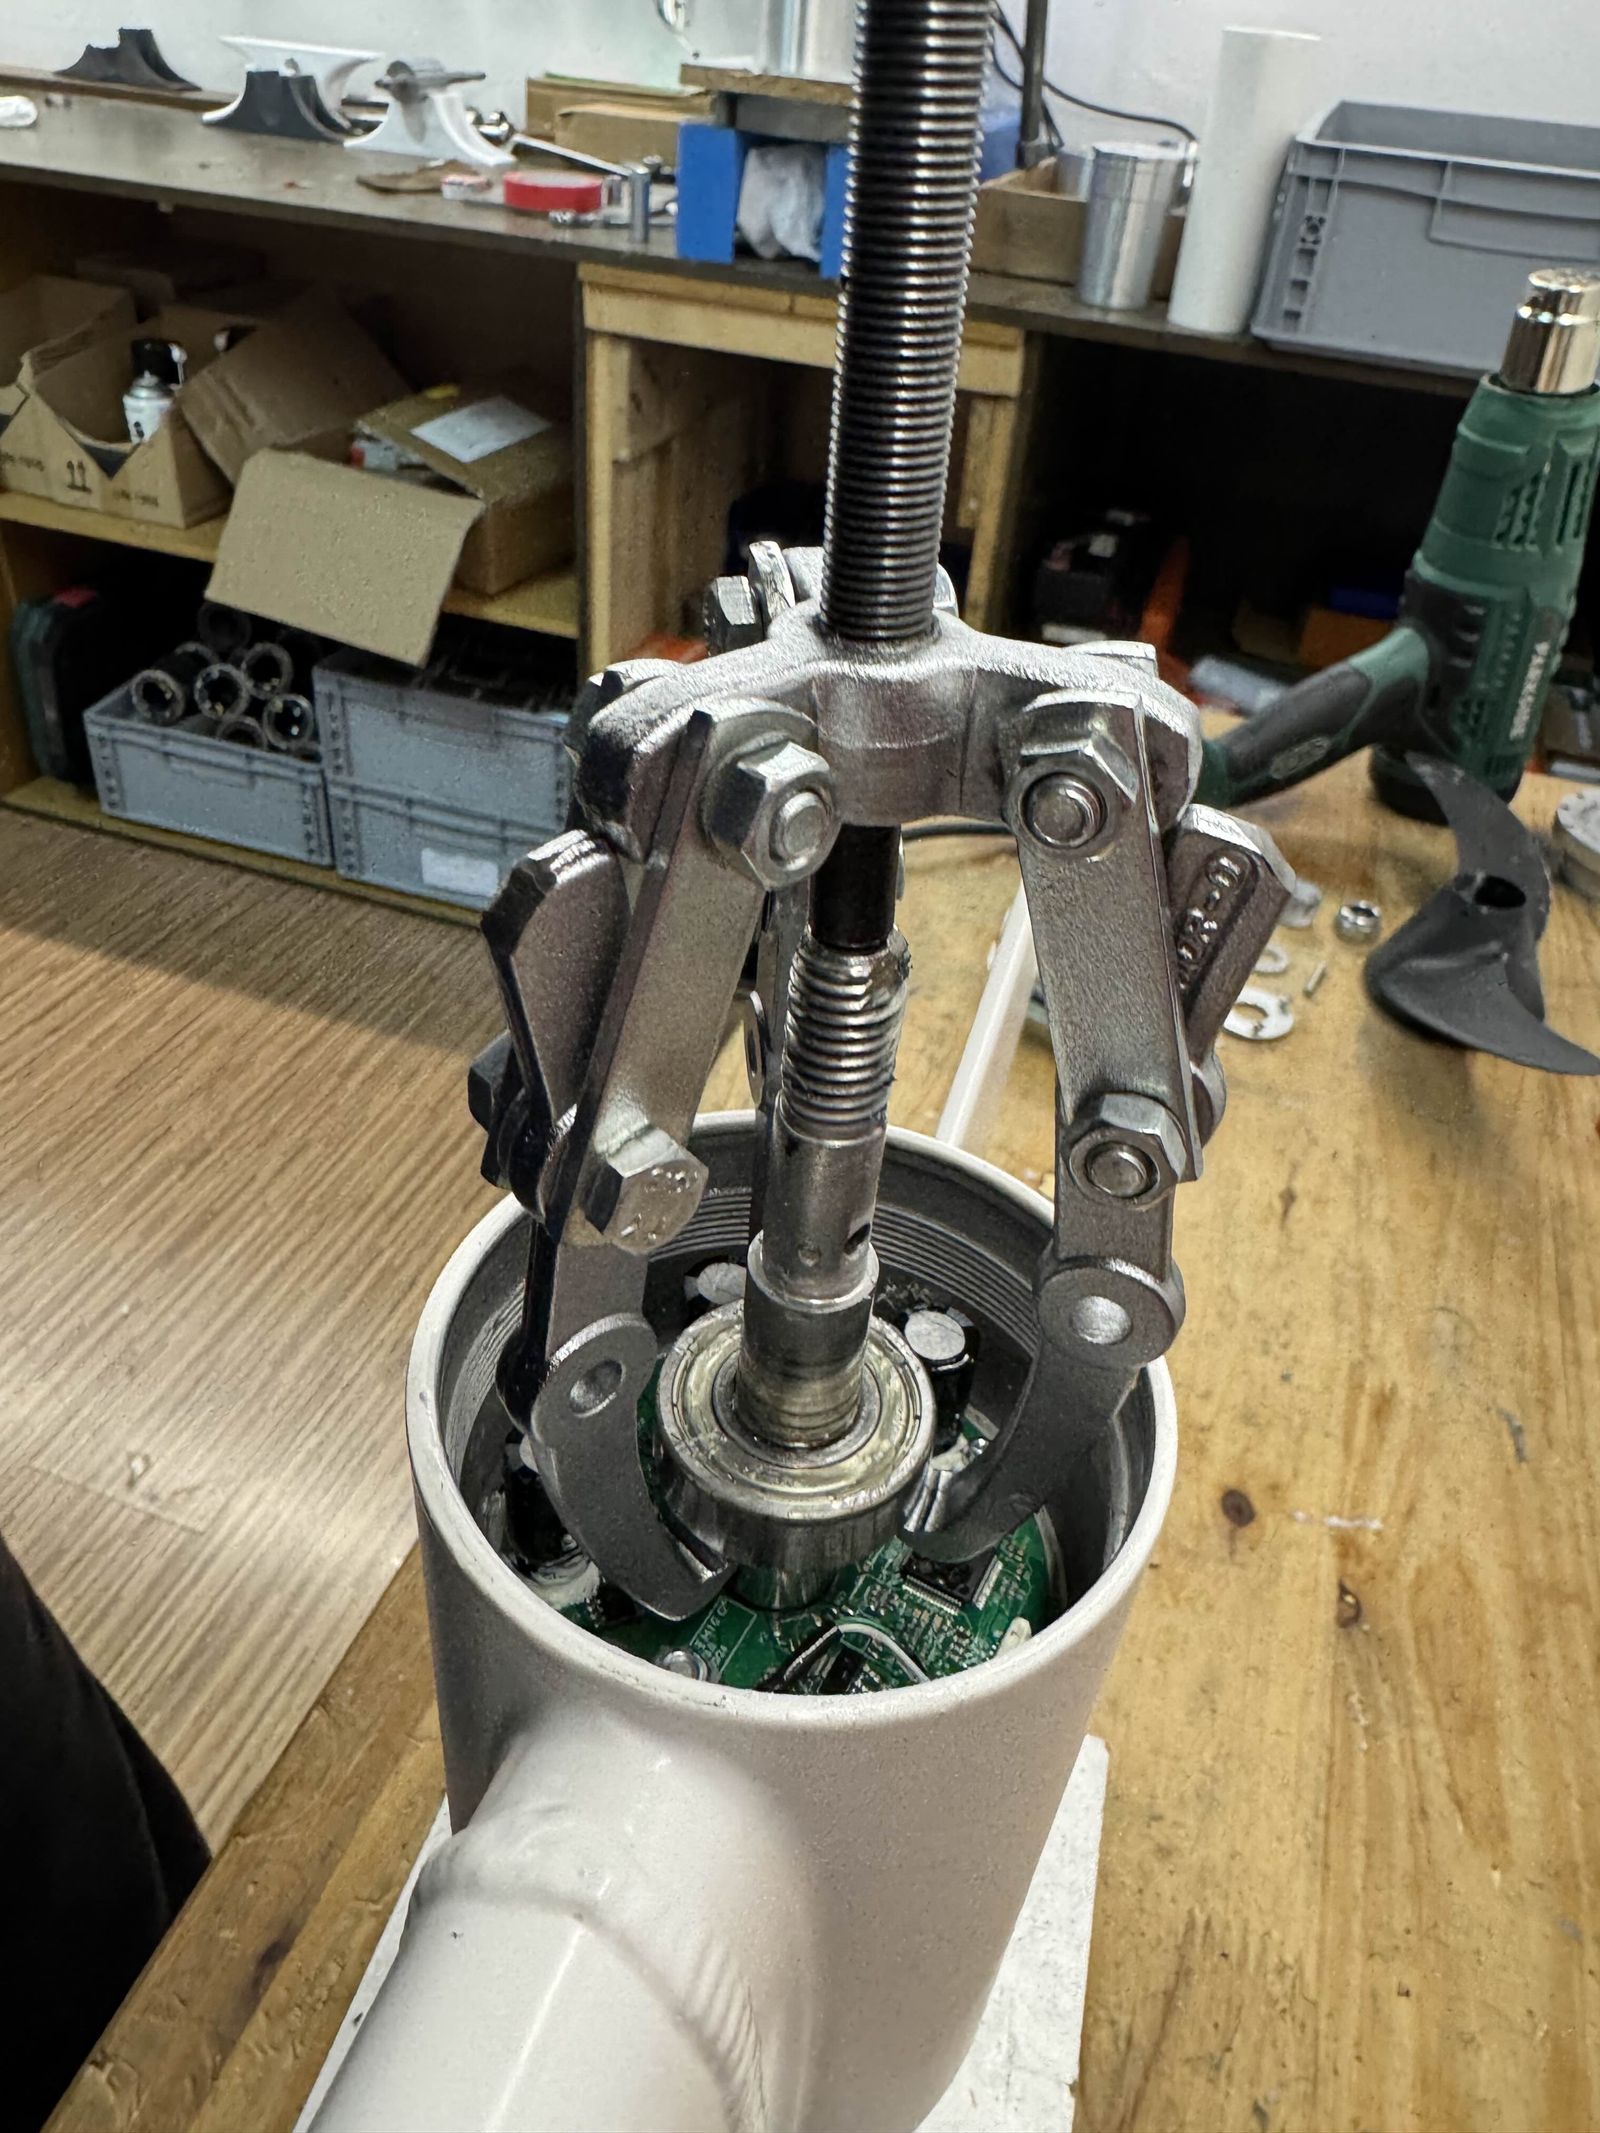
- Mount the axial bearing removal tool as shown.
- Apply torque on the forcing screw so that the claw legs grip the bearing evenly.
- Continue turning the forcing screw until the bearing is removed.
Link to originalCAUTION
🗑 Do not reuse the removed bearing. Always install a new bearing during assembly.
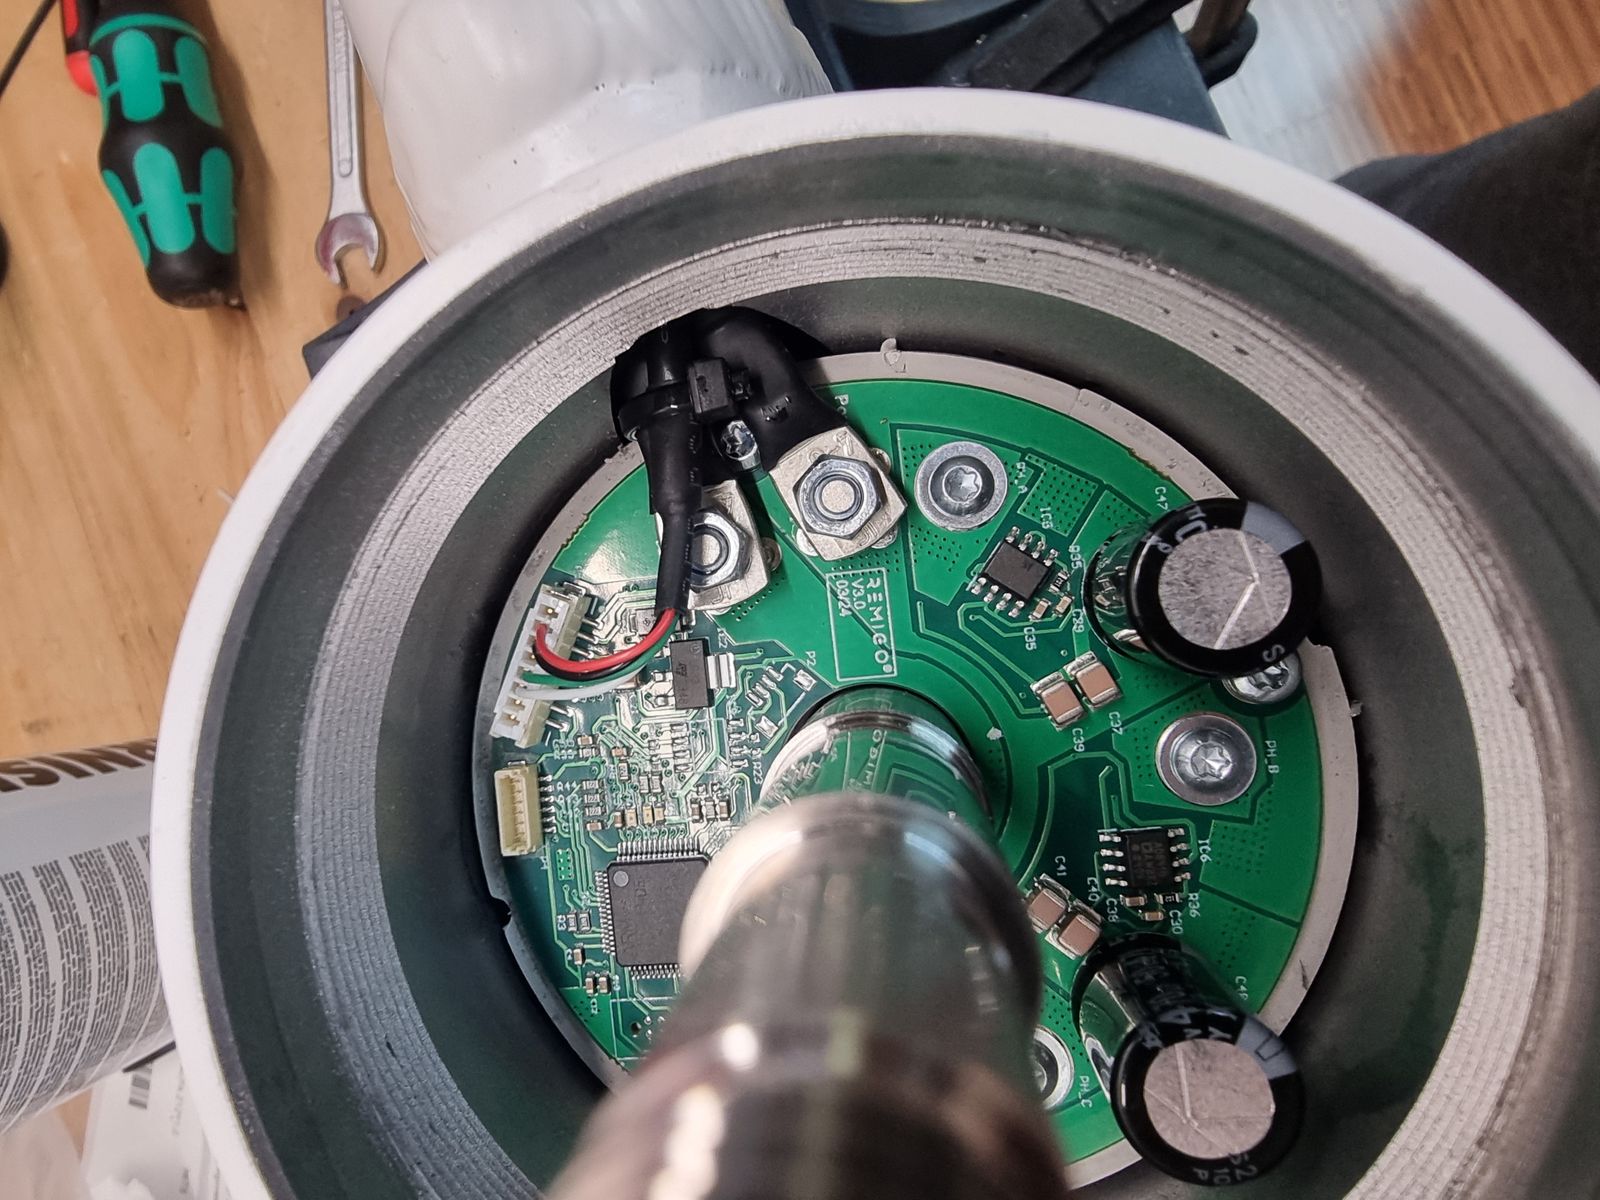
DT-DIS-011 DISASSEMBLY STEP 11 - Disconnect cables and prepare for heat sink removal
Tools:
Removing parts:
- No parts removed in this step.
Procedure:
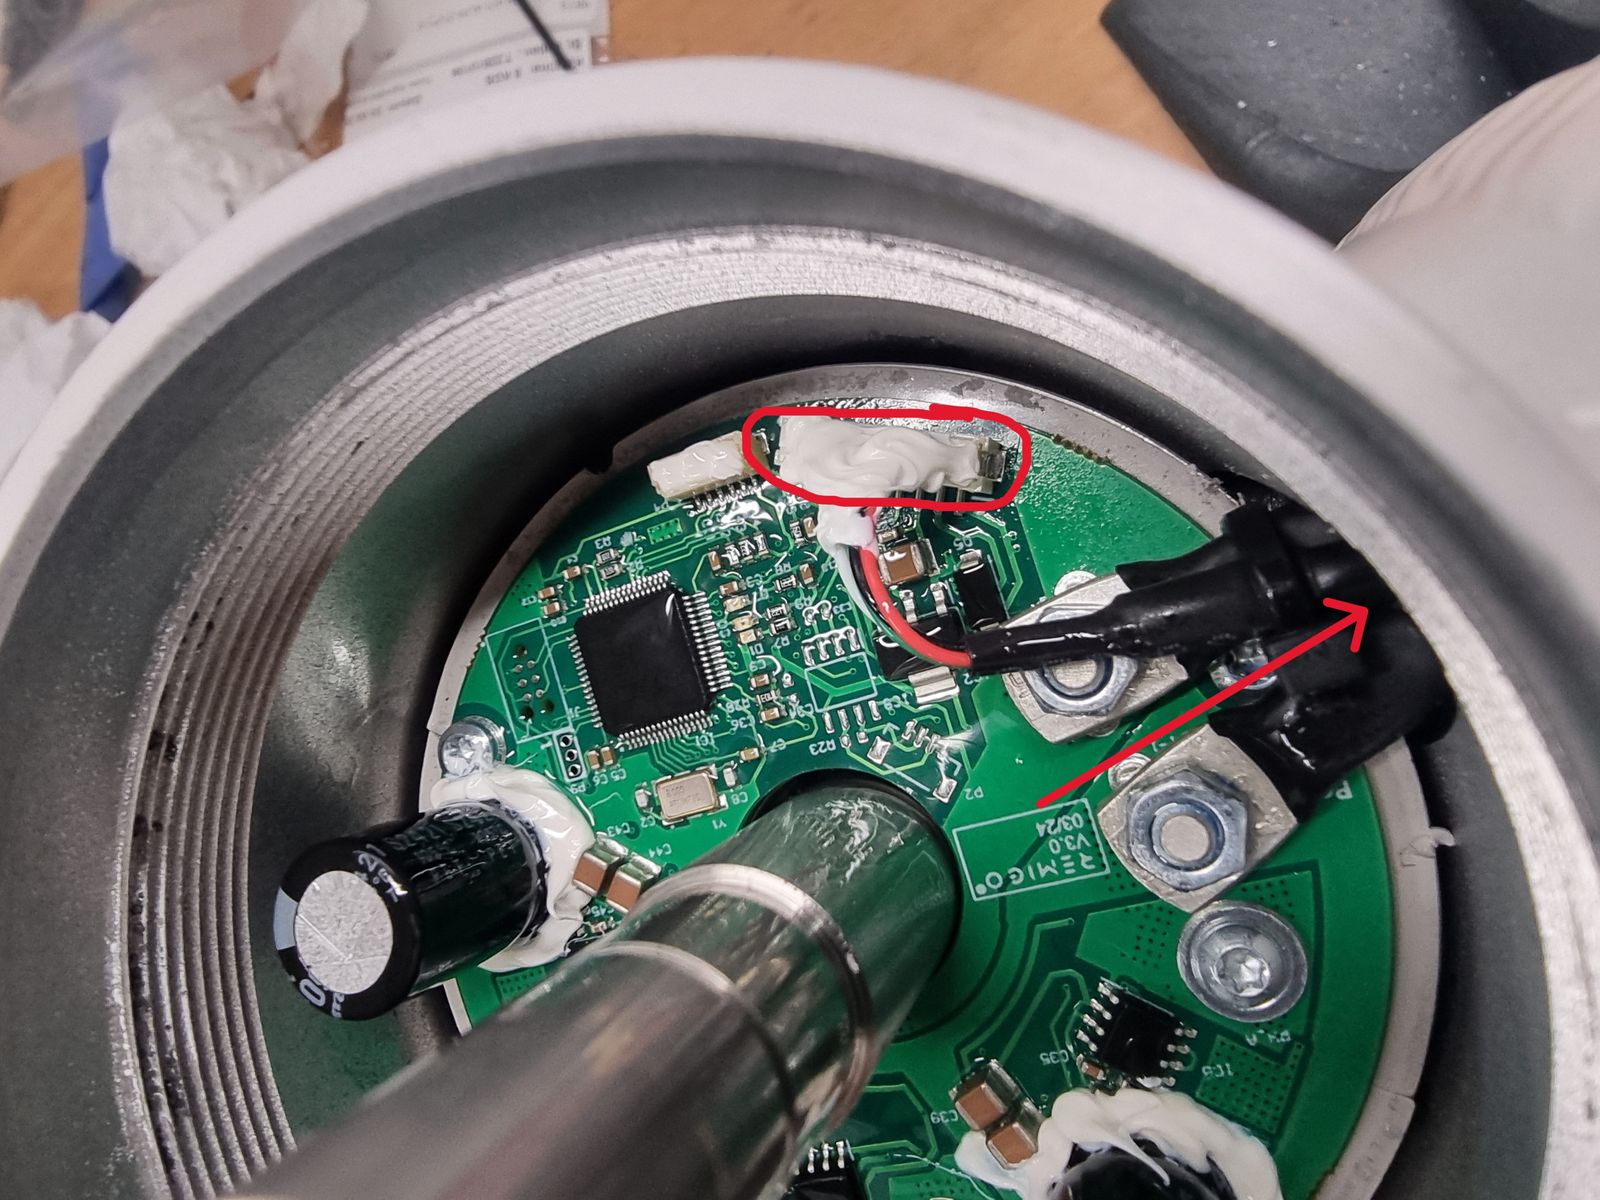
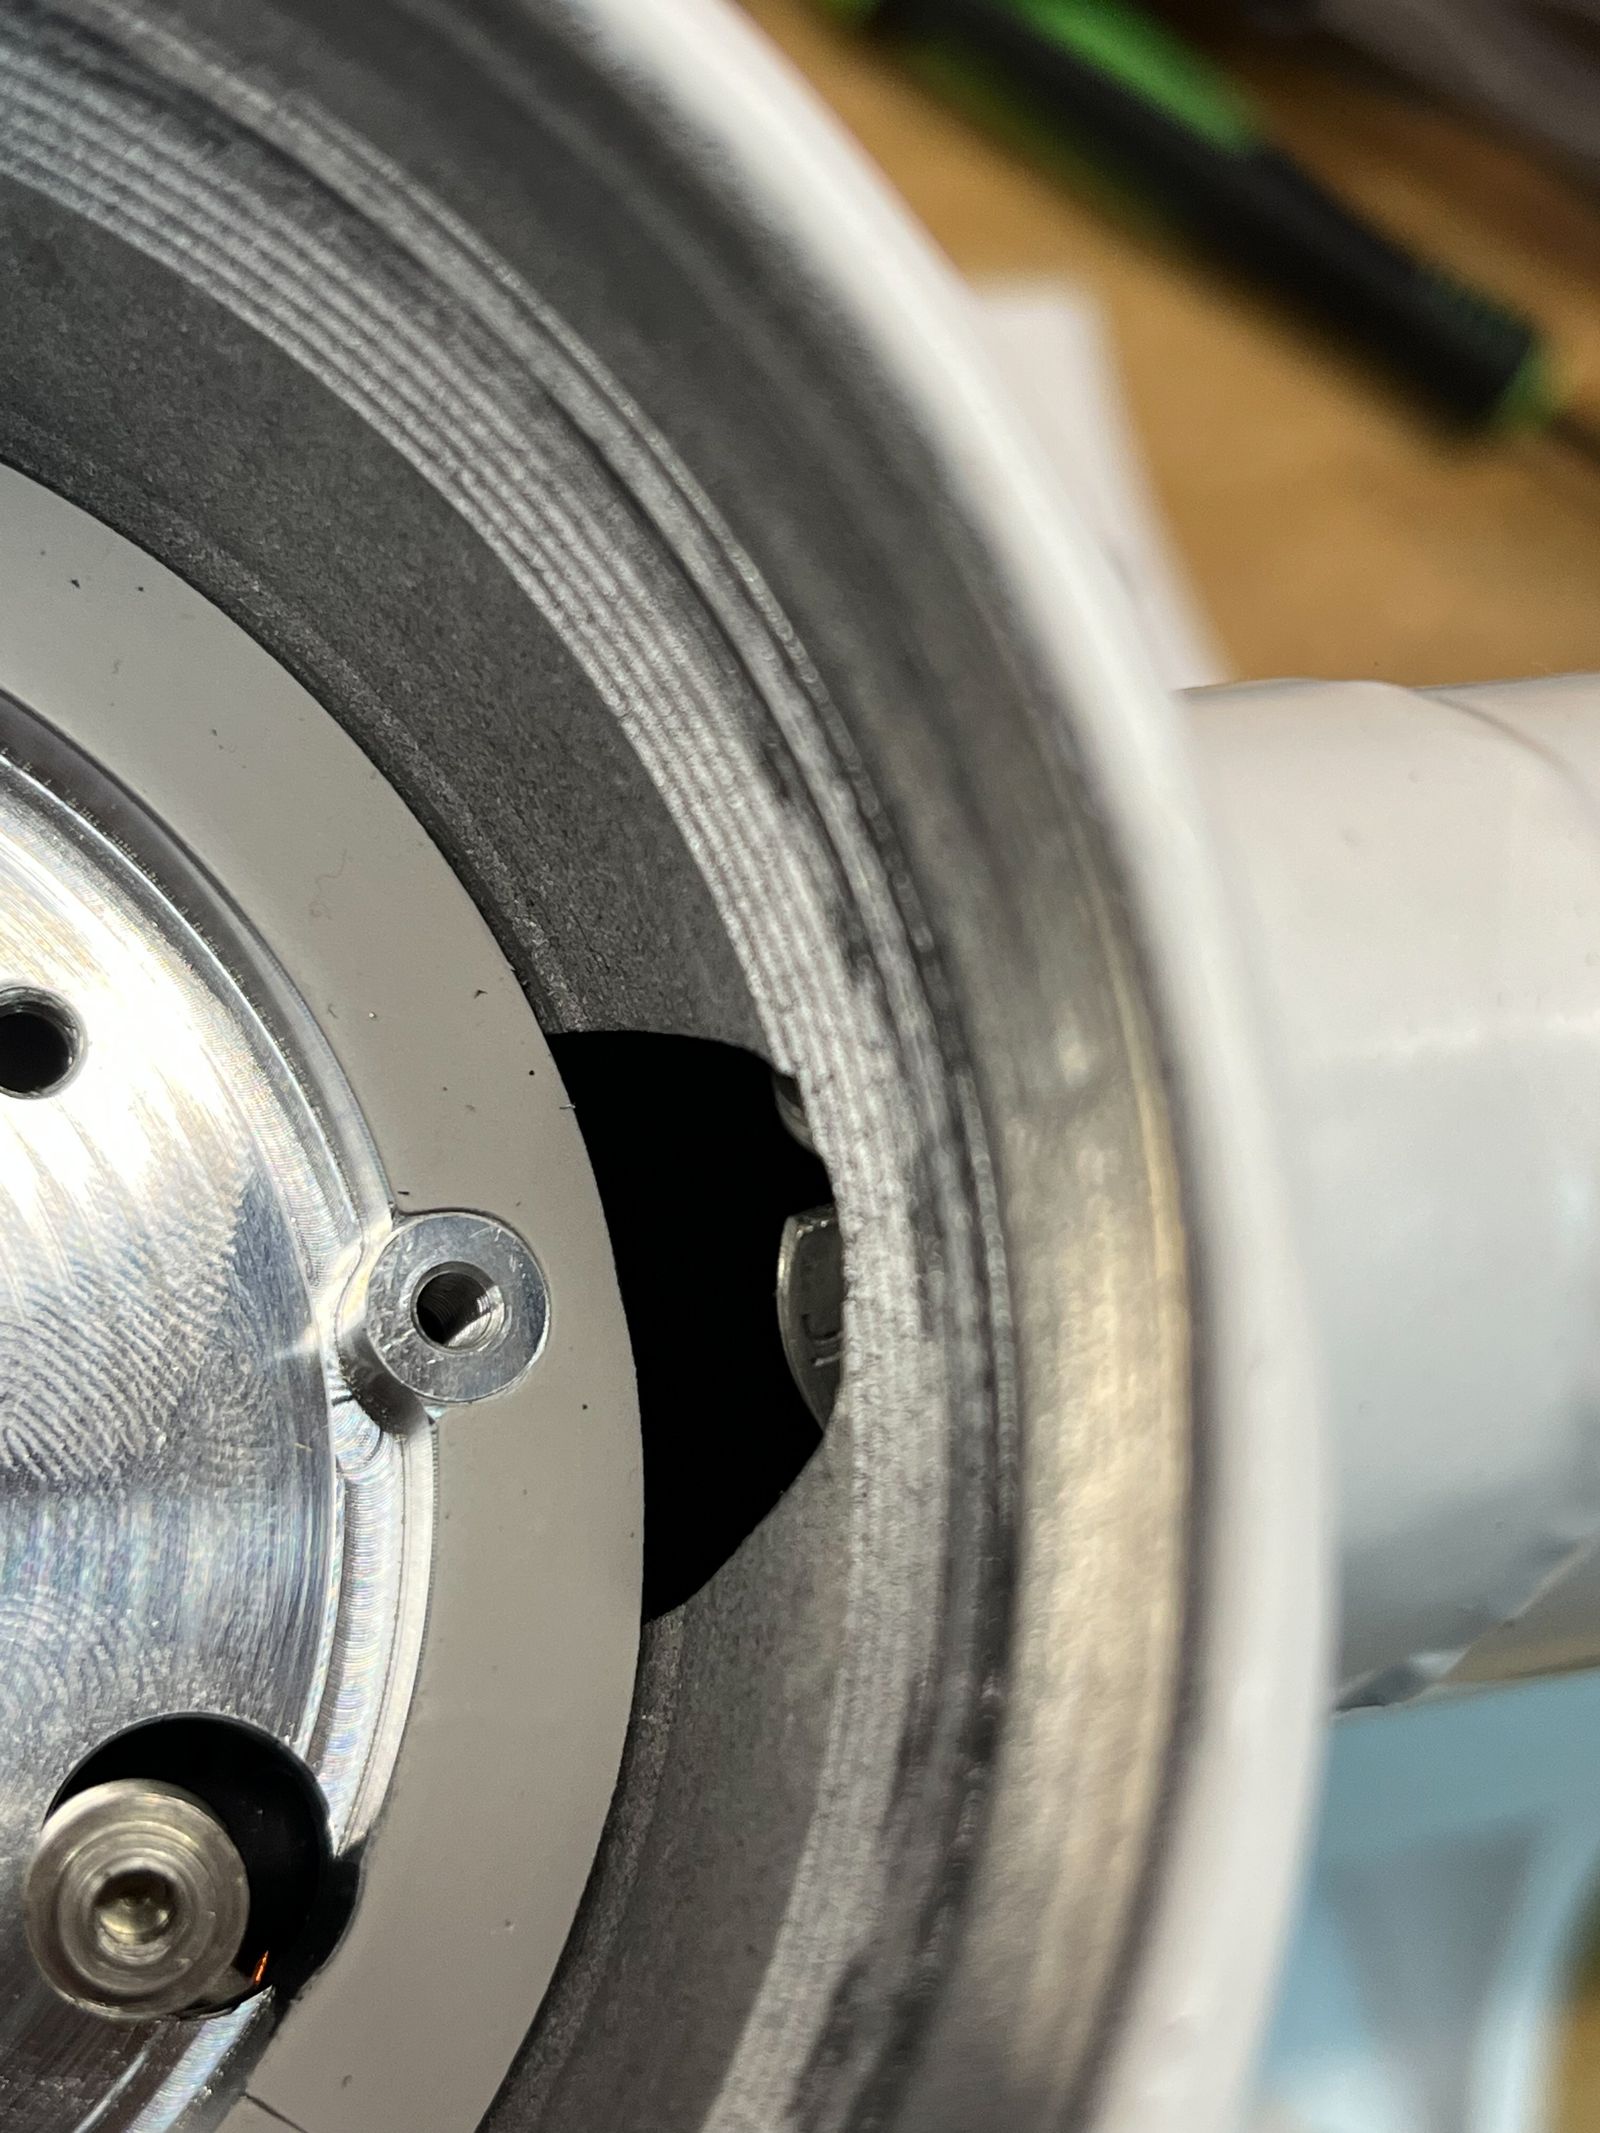
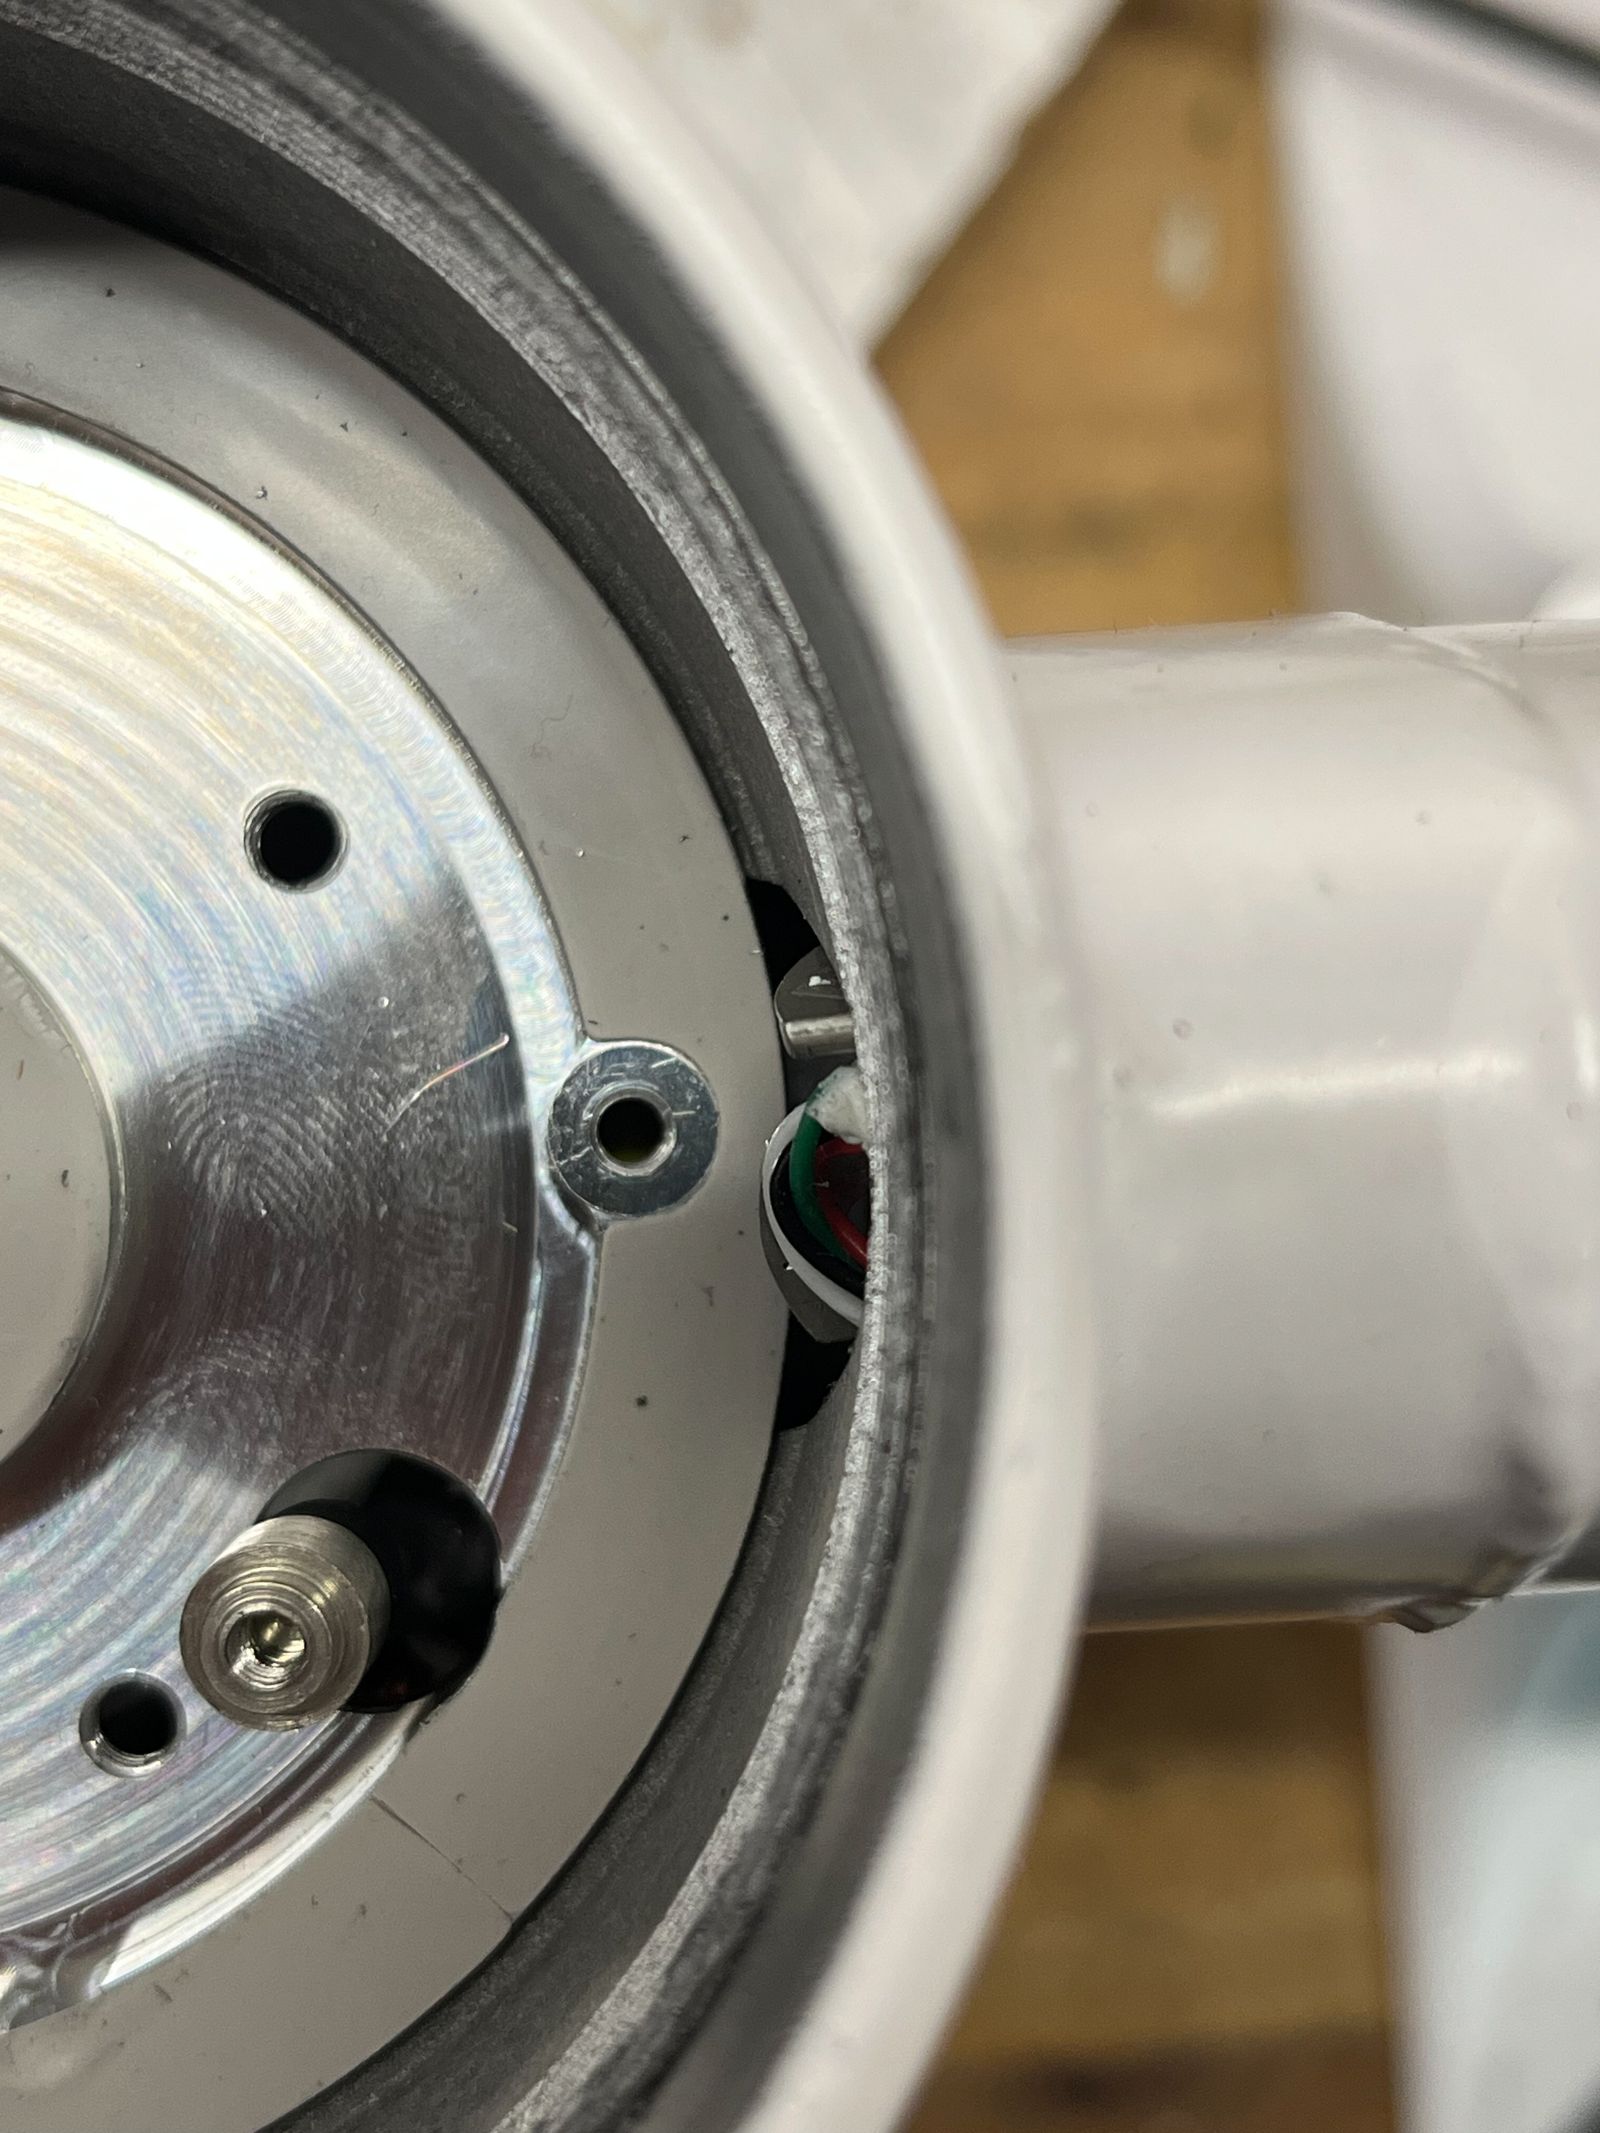
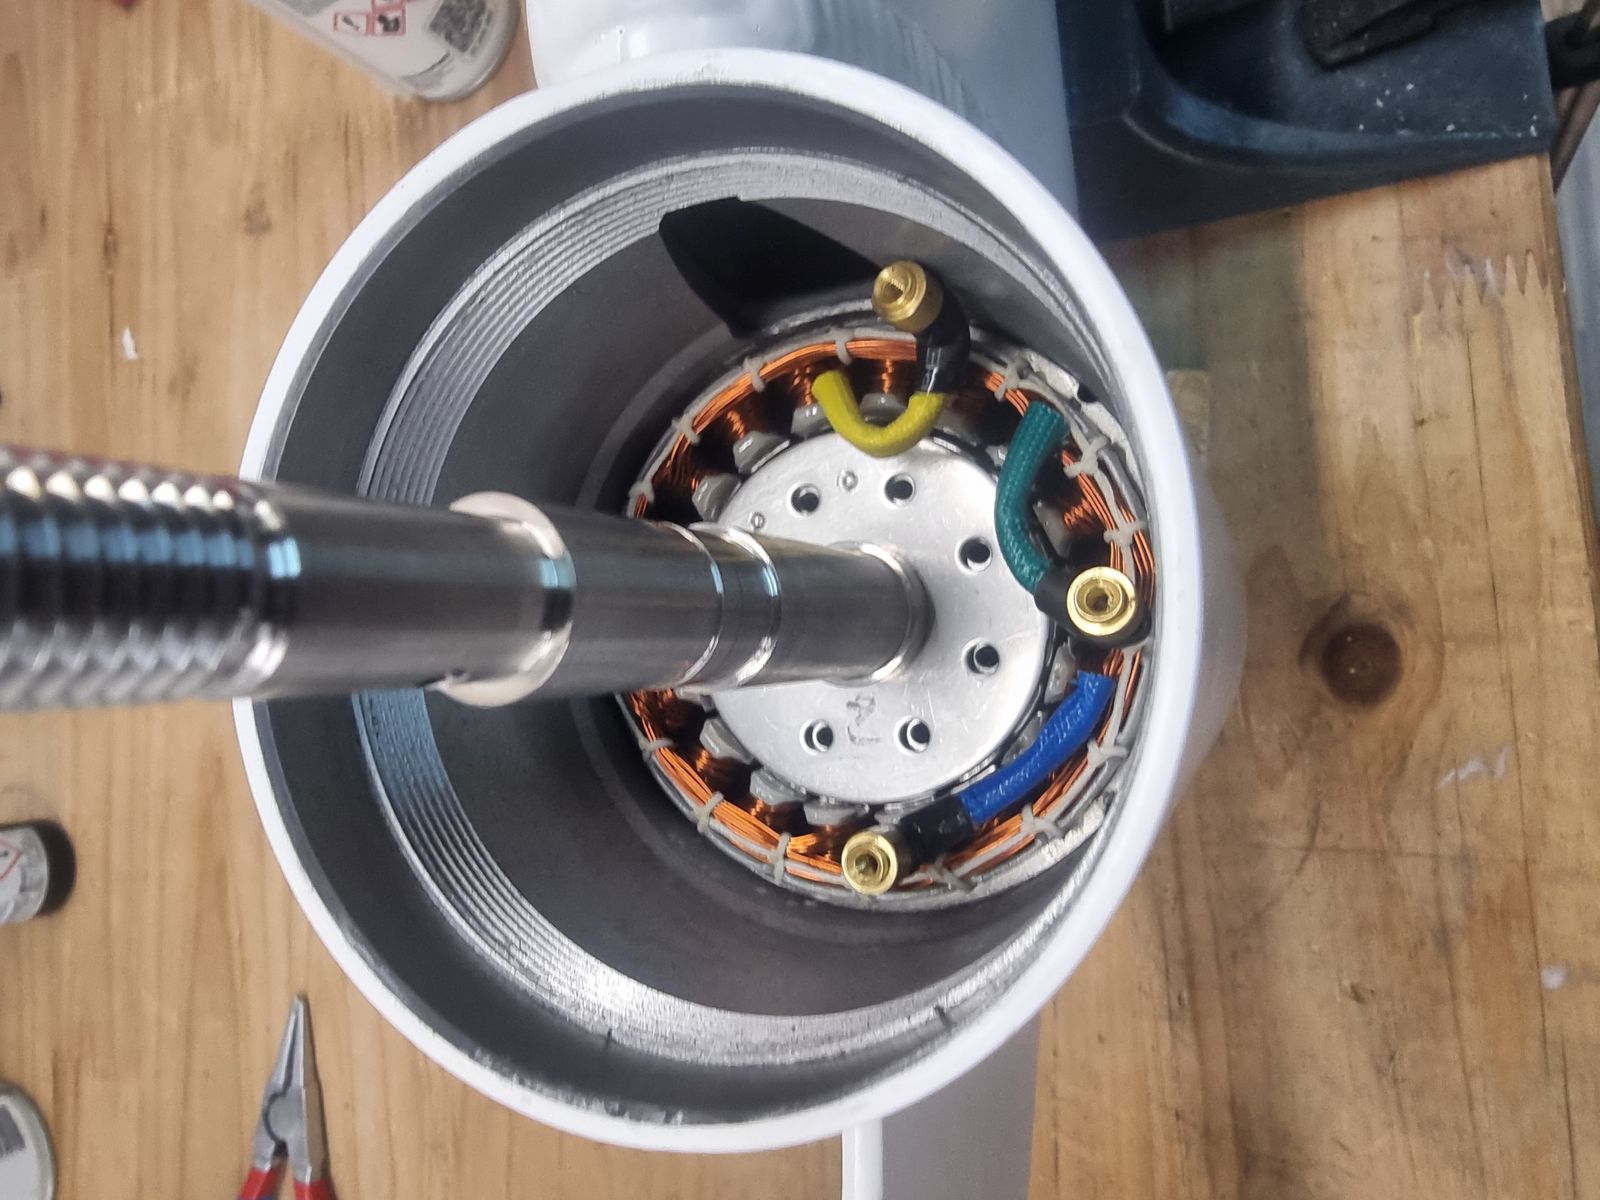
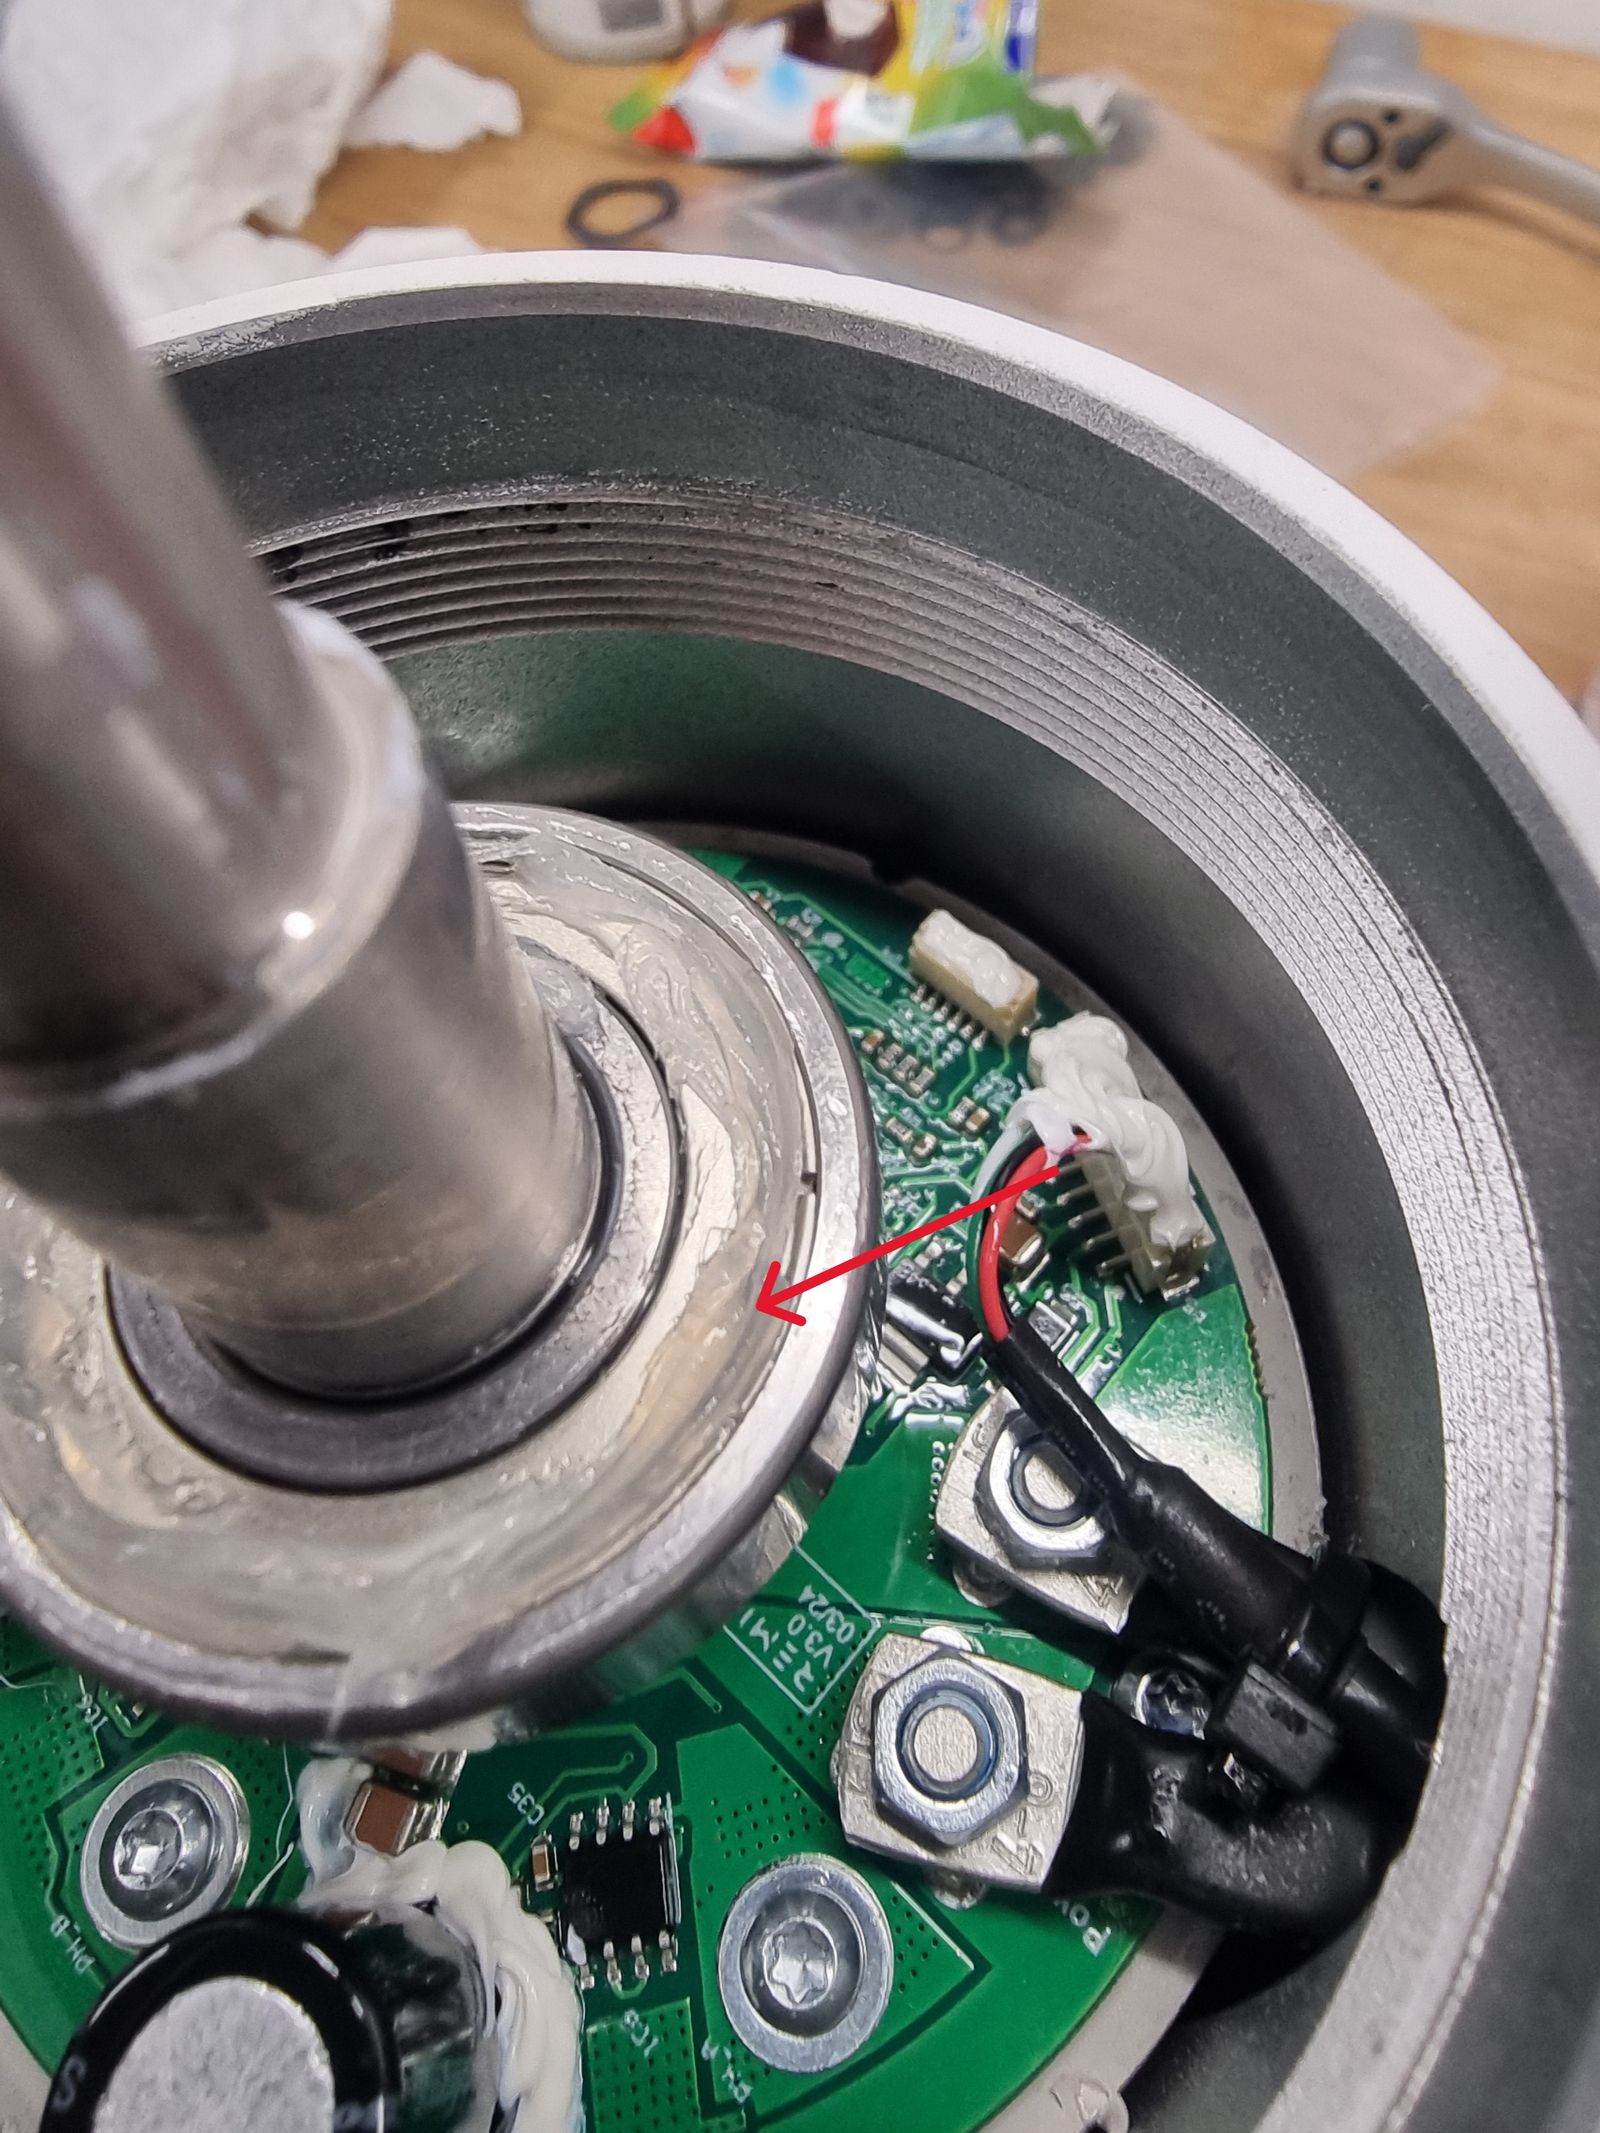
- Unplug the marked connector.
- Unscrew the two nuts.
- Tuck the cables inside the housing.
- Make sure that the cables do not protrude into the bore.
Correct cable position
Incorrect cable position
Link to originalWARNING
Cables can be sheared during heat sink removal if they are not tucked completely inside the housing bore.
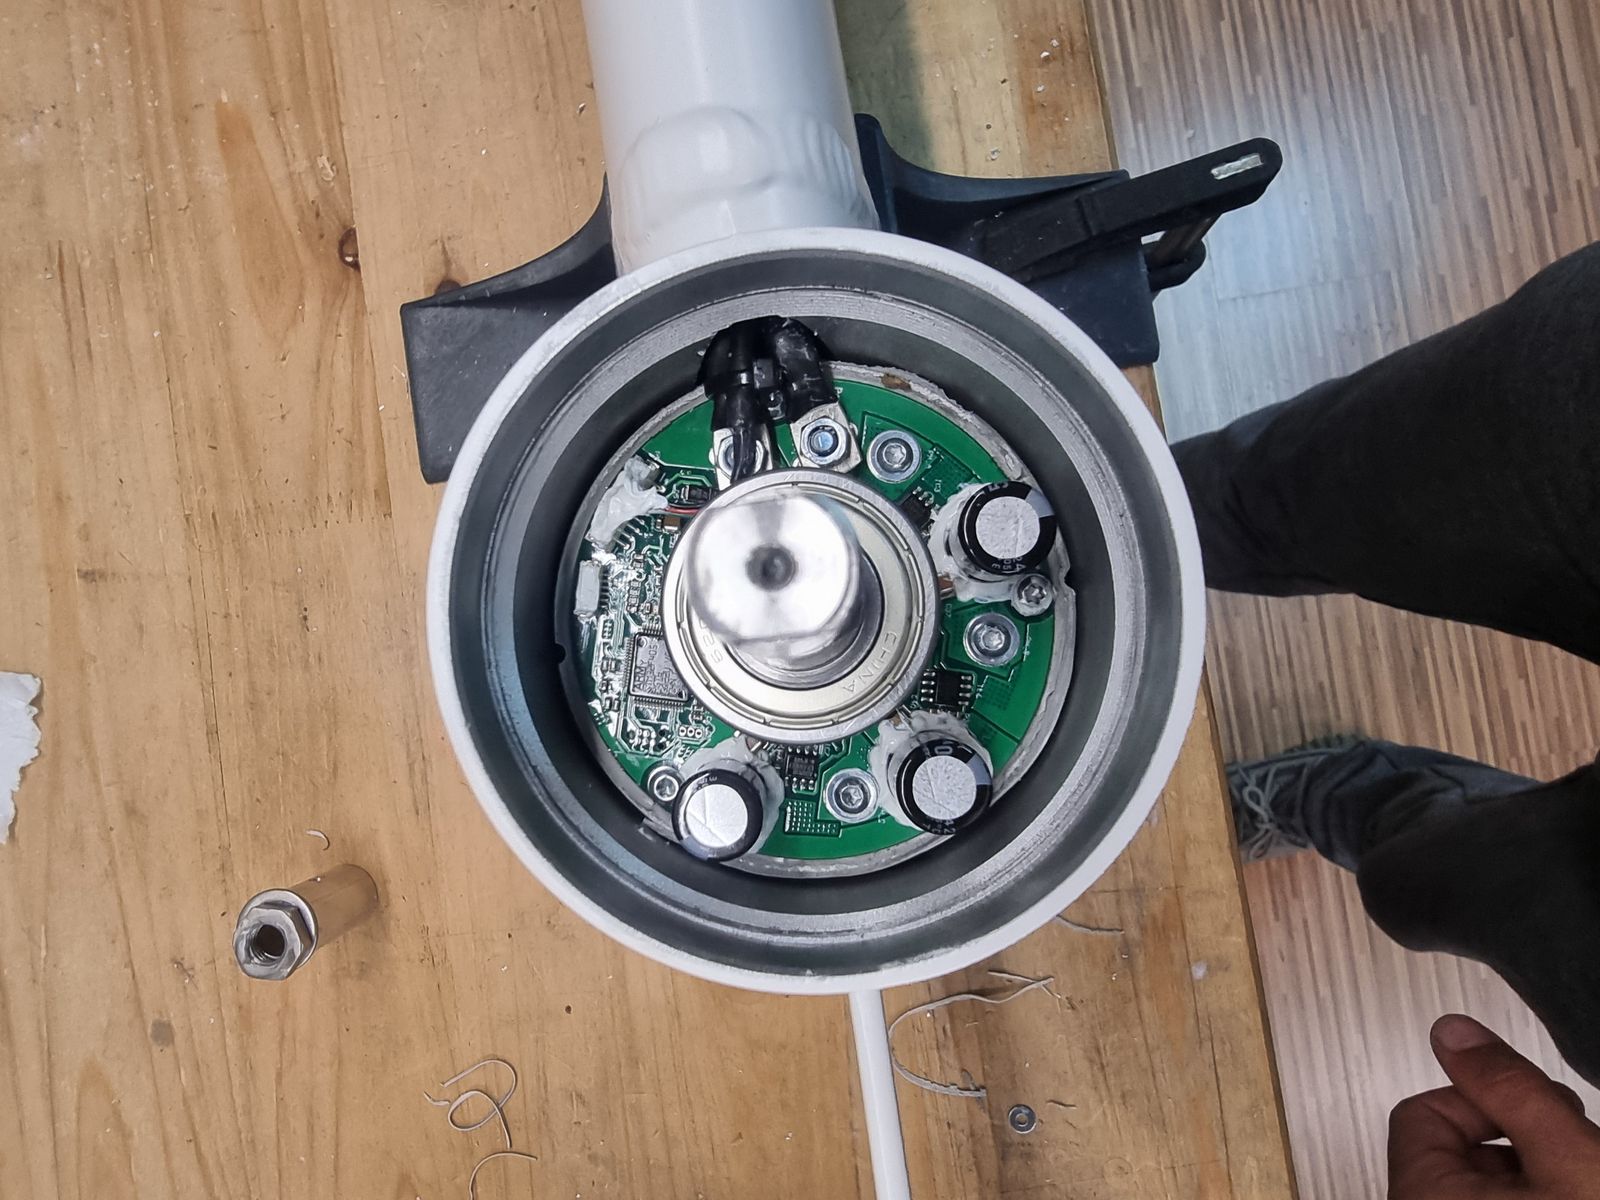
DT-DIS-012 DISASSEMBLY STEP 12 - Remove motor controller
Tools:
Removing parts:
Procedure:
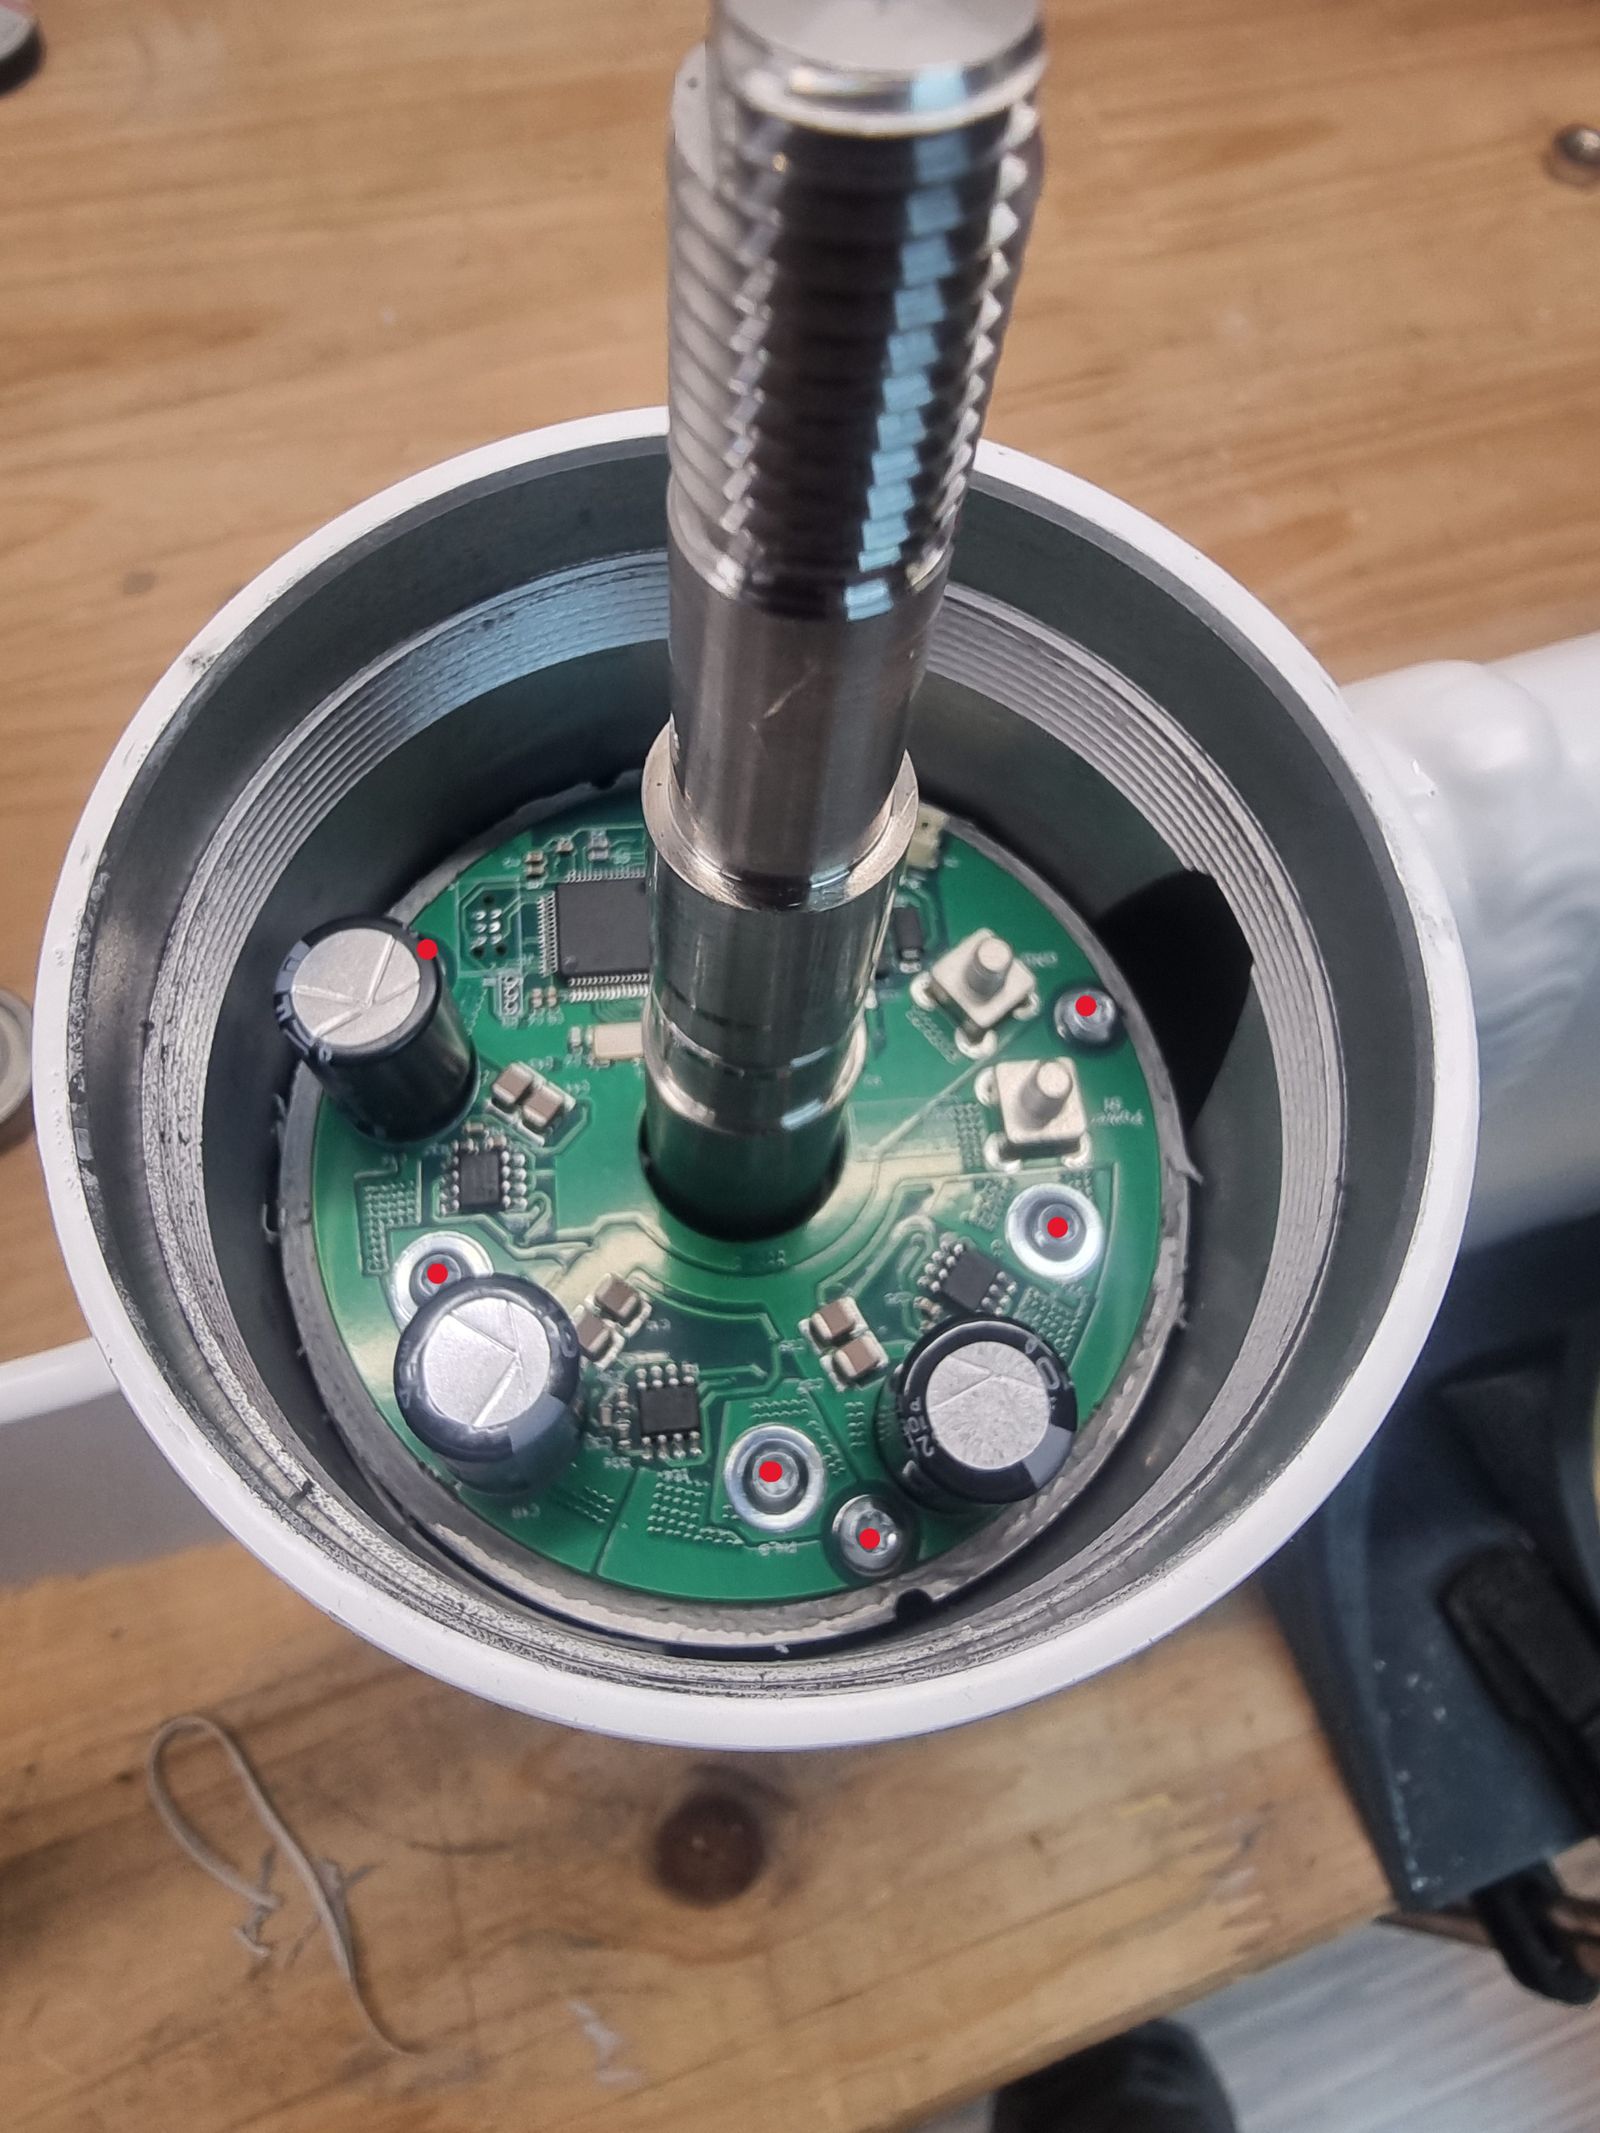
- Unscrew the marked screws.
- Remove the motor controller.
Link to originalCAUTION
The motor controller must only be handled in an ESD-protected environment. Use proper ESD protection before disconnecting or removing the controller.
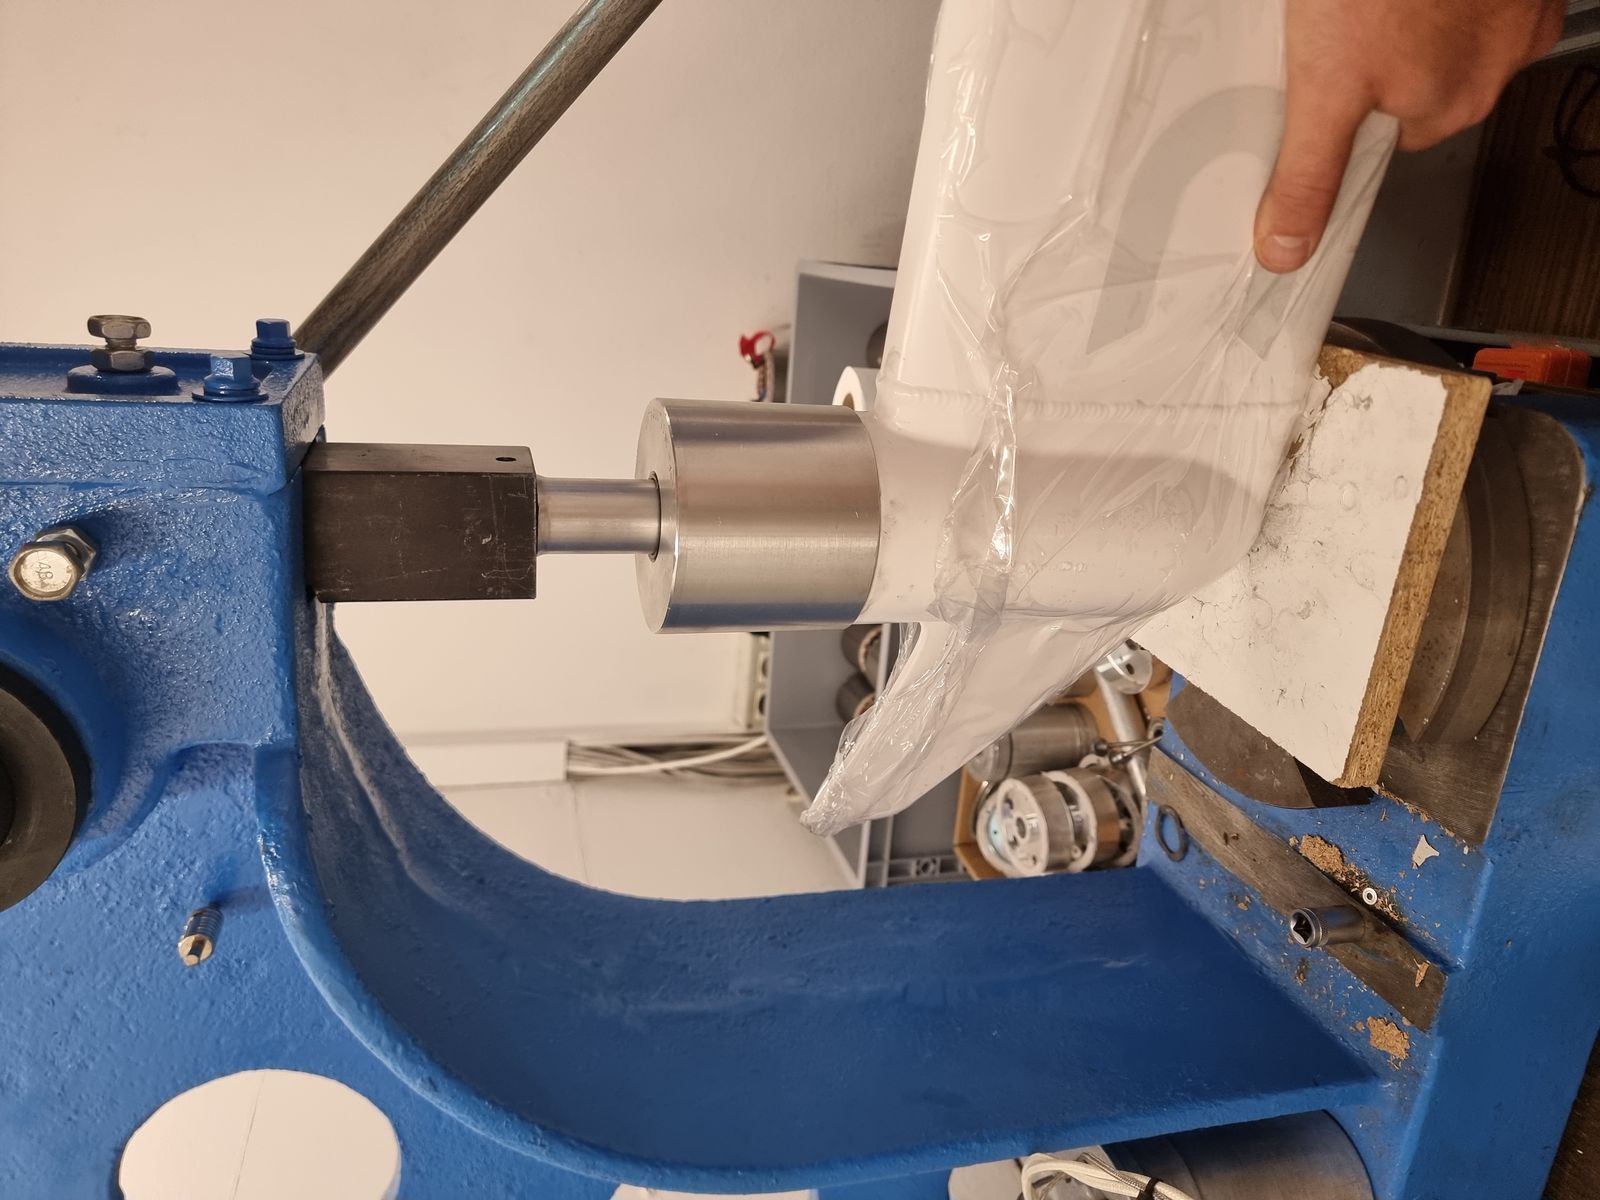
DT-DIS-013 DISASSEMBLY STEP 13 - Remove heat sink
Tools:
Removing parts:
Procedure:
Link to original
- Insert the tool base plate into the heat sink.
- Screw the mounting screws into the heat sink.
- Screw on the second part of the heat sink removal tool.
- Carefully rotate the lever clockwise (CW) until the heat sink starts to press out.
- Pull the heat sink out.
- Clean the thermal paste from the controller and heat sink.
DT-DIS-014 DISASSEMBLY STEP 14 - Remove rotor
Tools:
Removing parts:
Procedure:
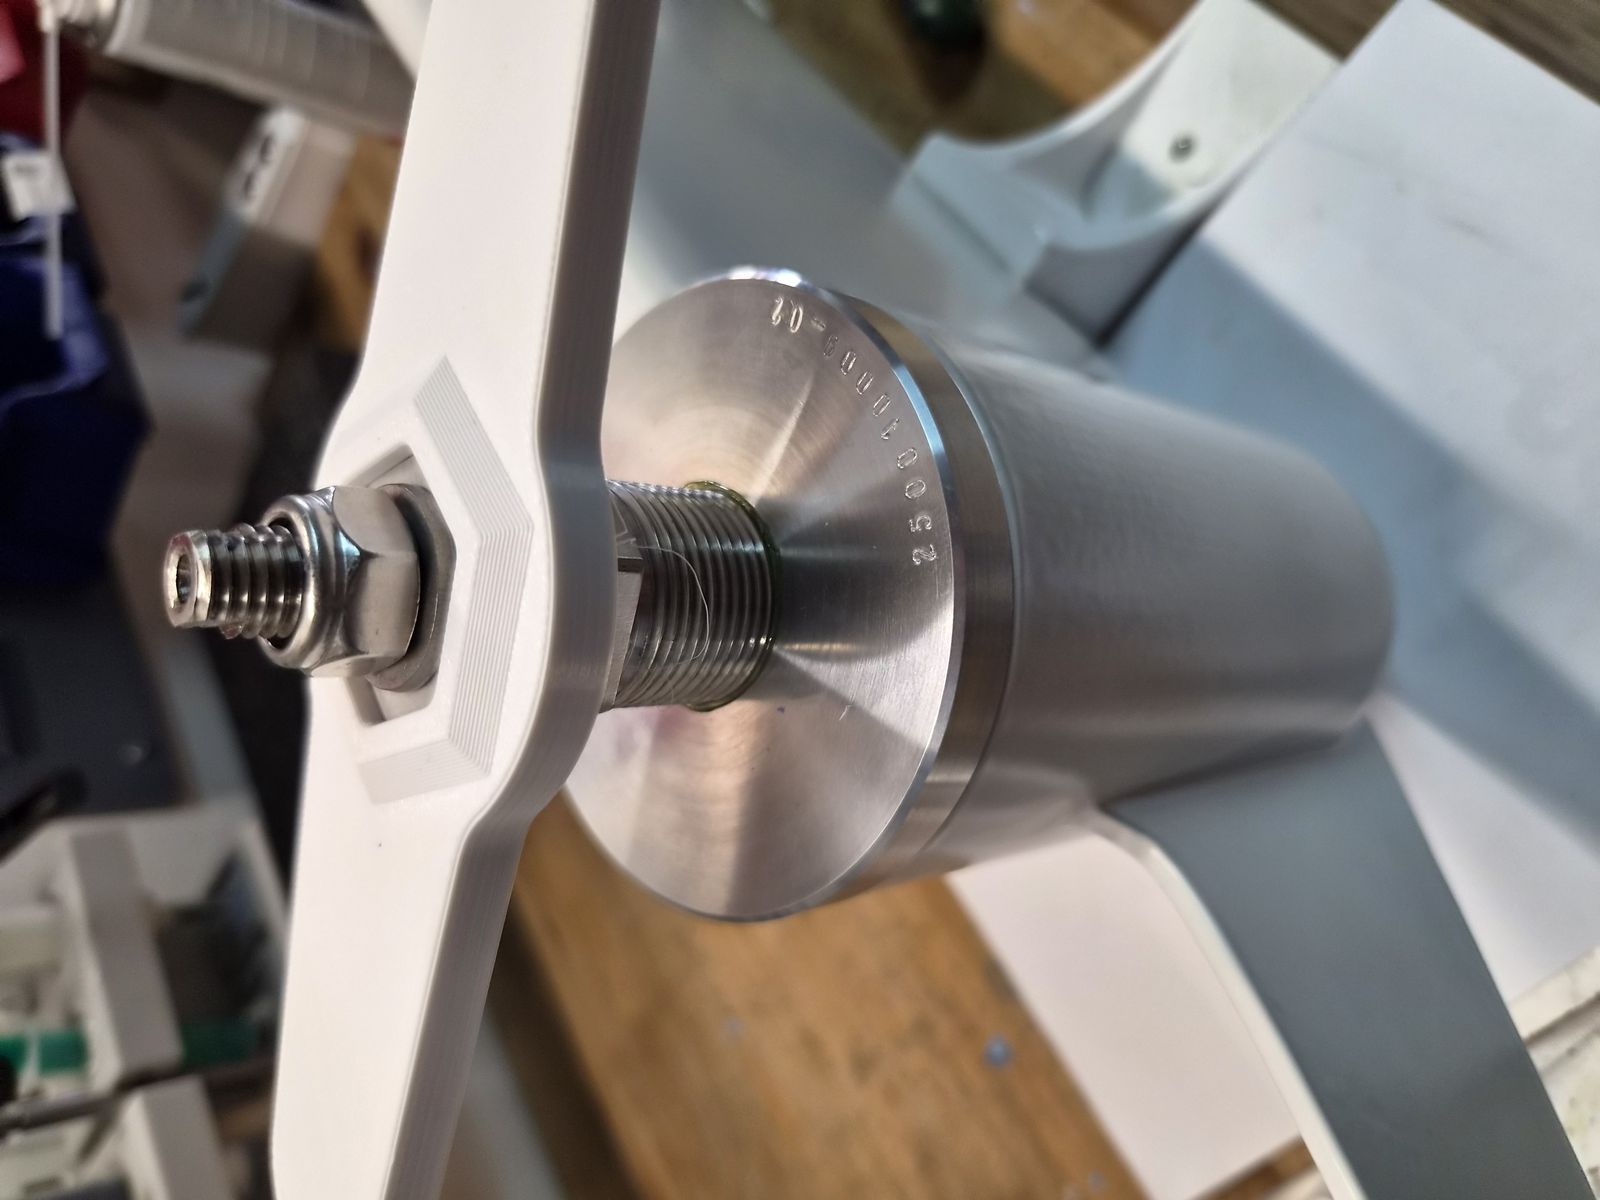
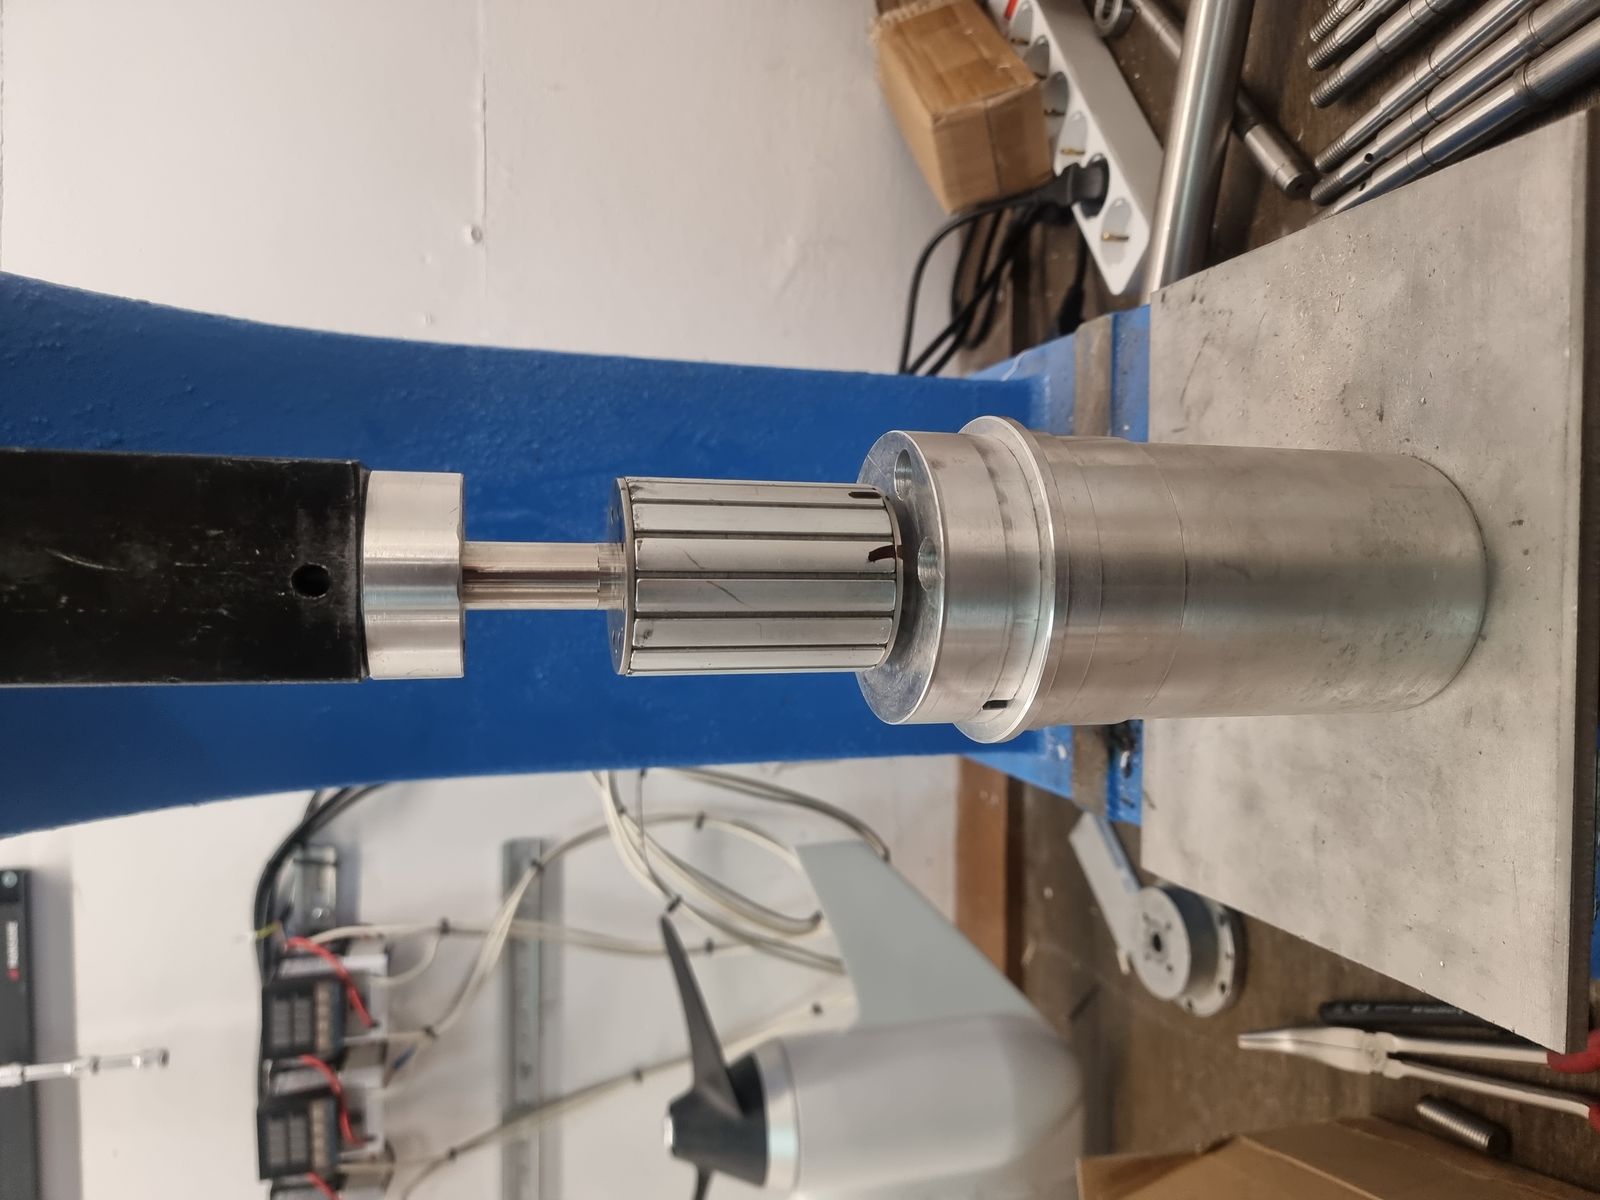
- Assemble the rotor removal tool onto the motor shaft.
- Screw the M12 nut onto the tool.
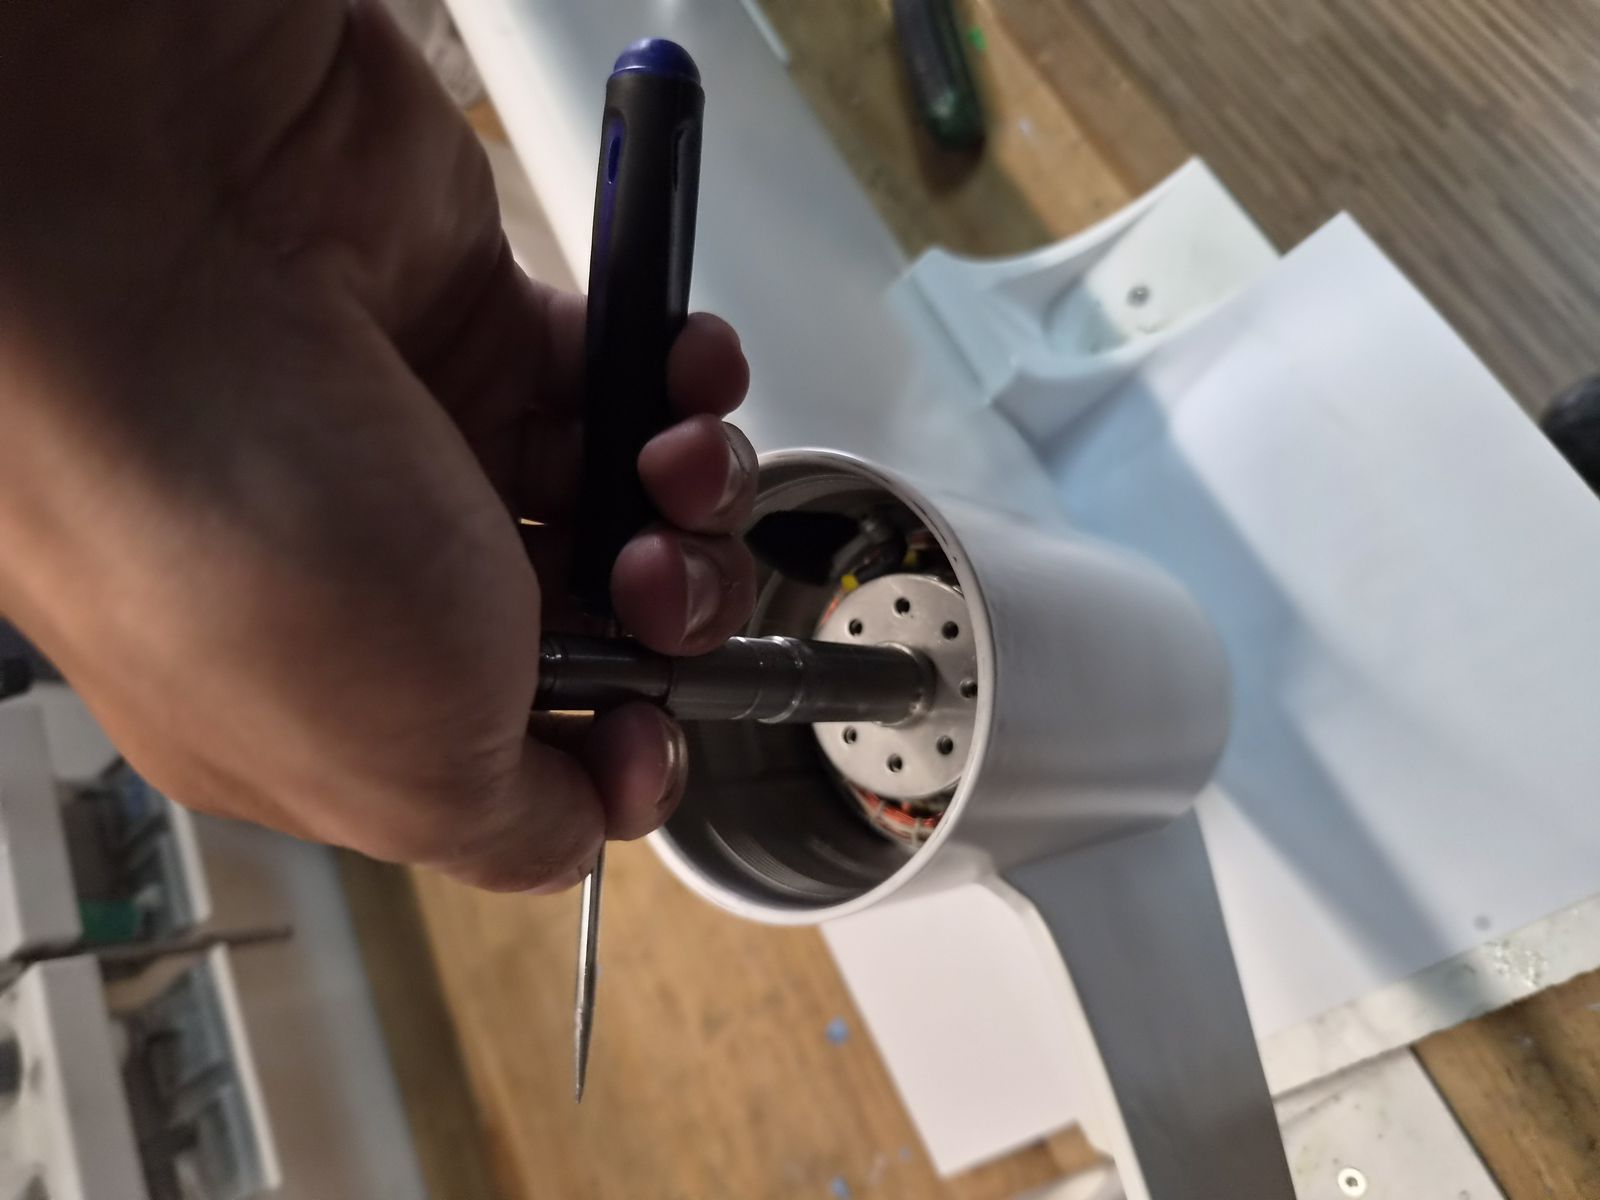
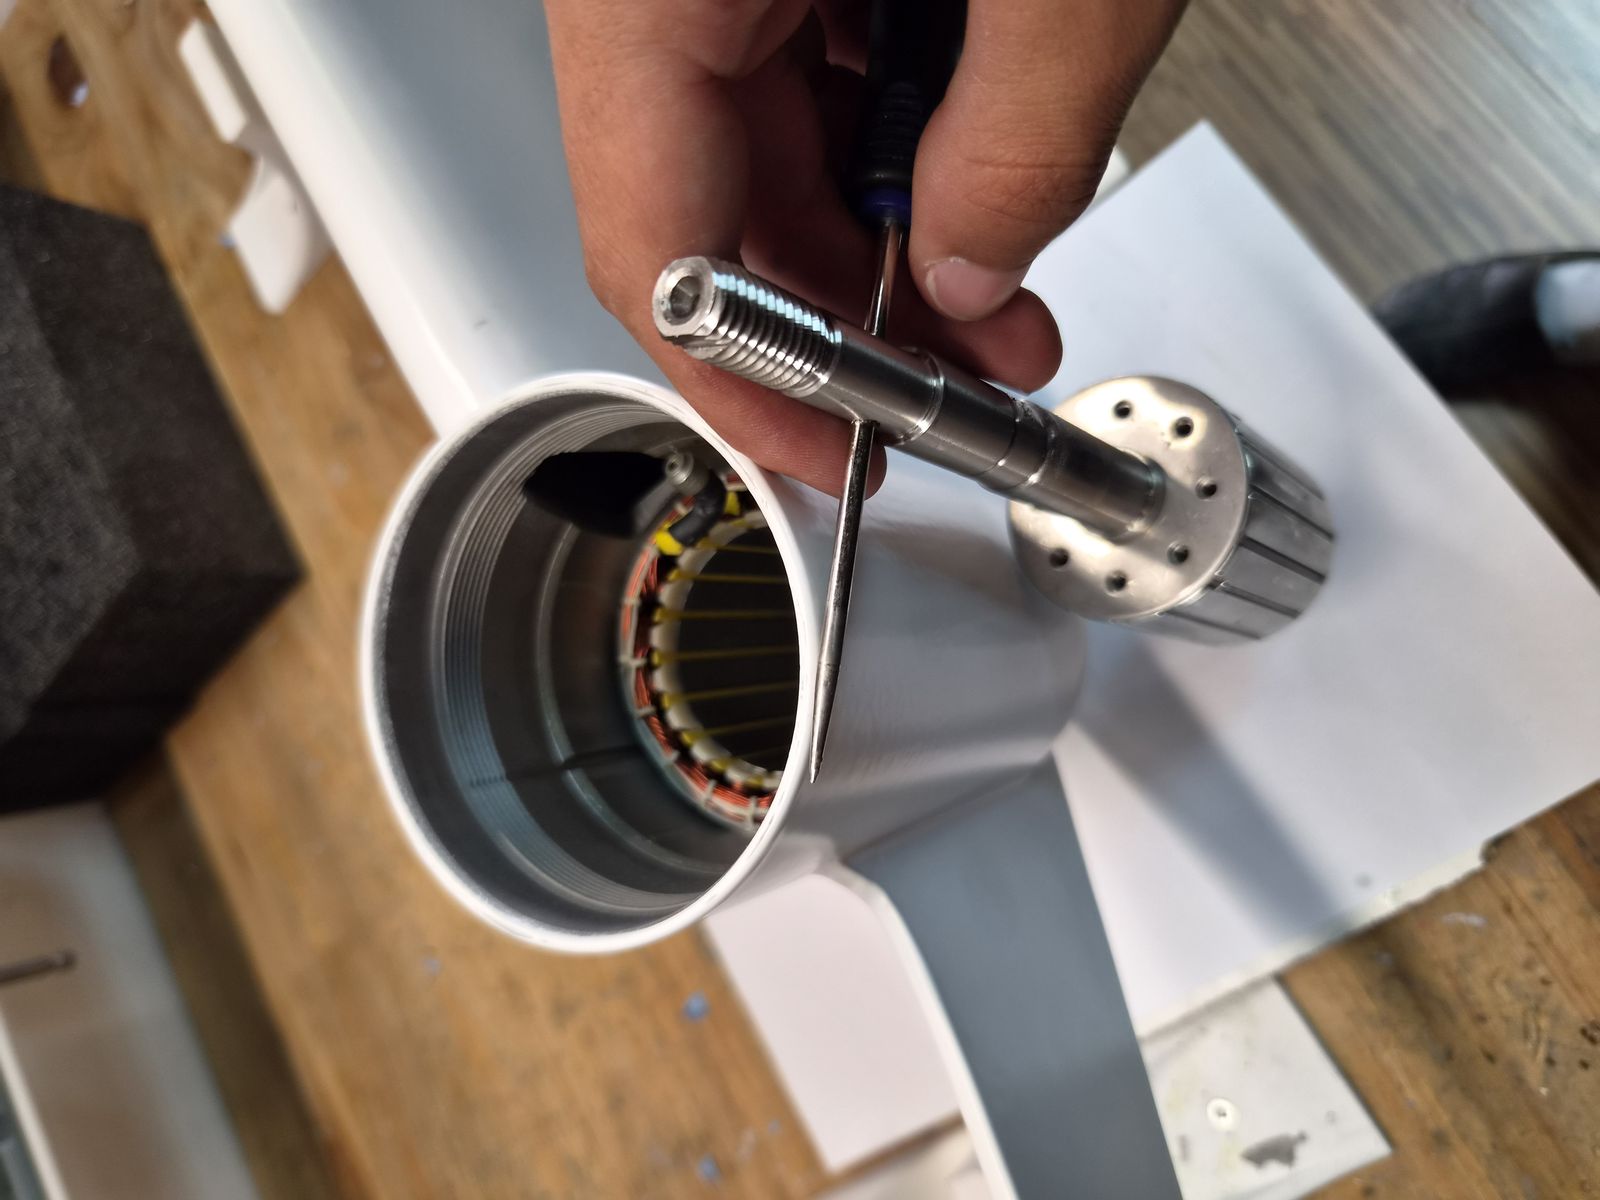
- Attach the lever and rotate it clockwise (CW). The tool will slowly lift the rotor out of the motor housing.
- Insert a screwdriver through the radial hole in the rotor and use it to pull the rotor the rest of the way out.
Link to originalWARNING
The rotor contains strong magnets. Keep fingers clear of pinch points during removal.
DT-DIS-015 DISASSEMBLY STEP 15 - Clean motor housing
Tools:
- No tools required.
Removing parts:
- No parts removed in this step.
Procedure:
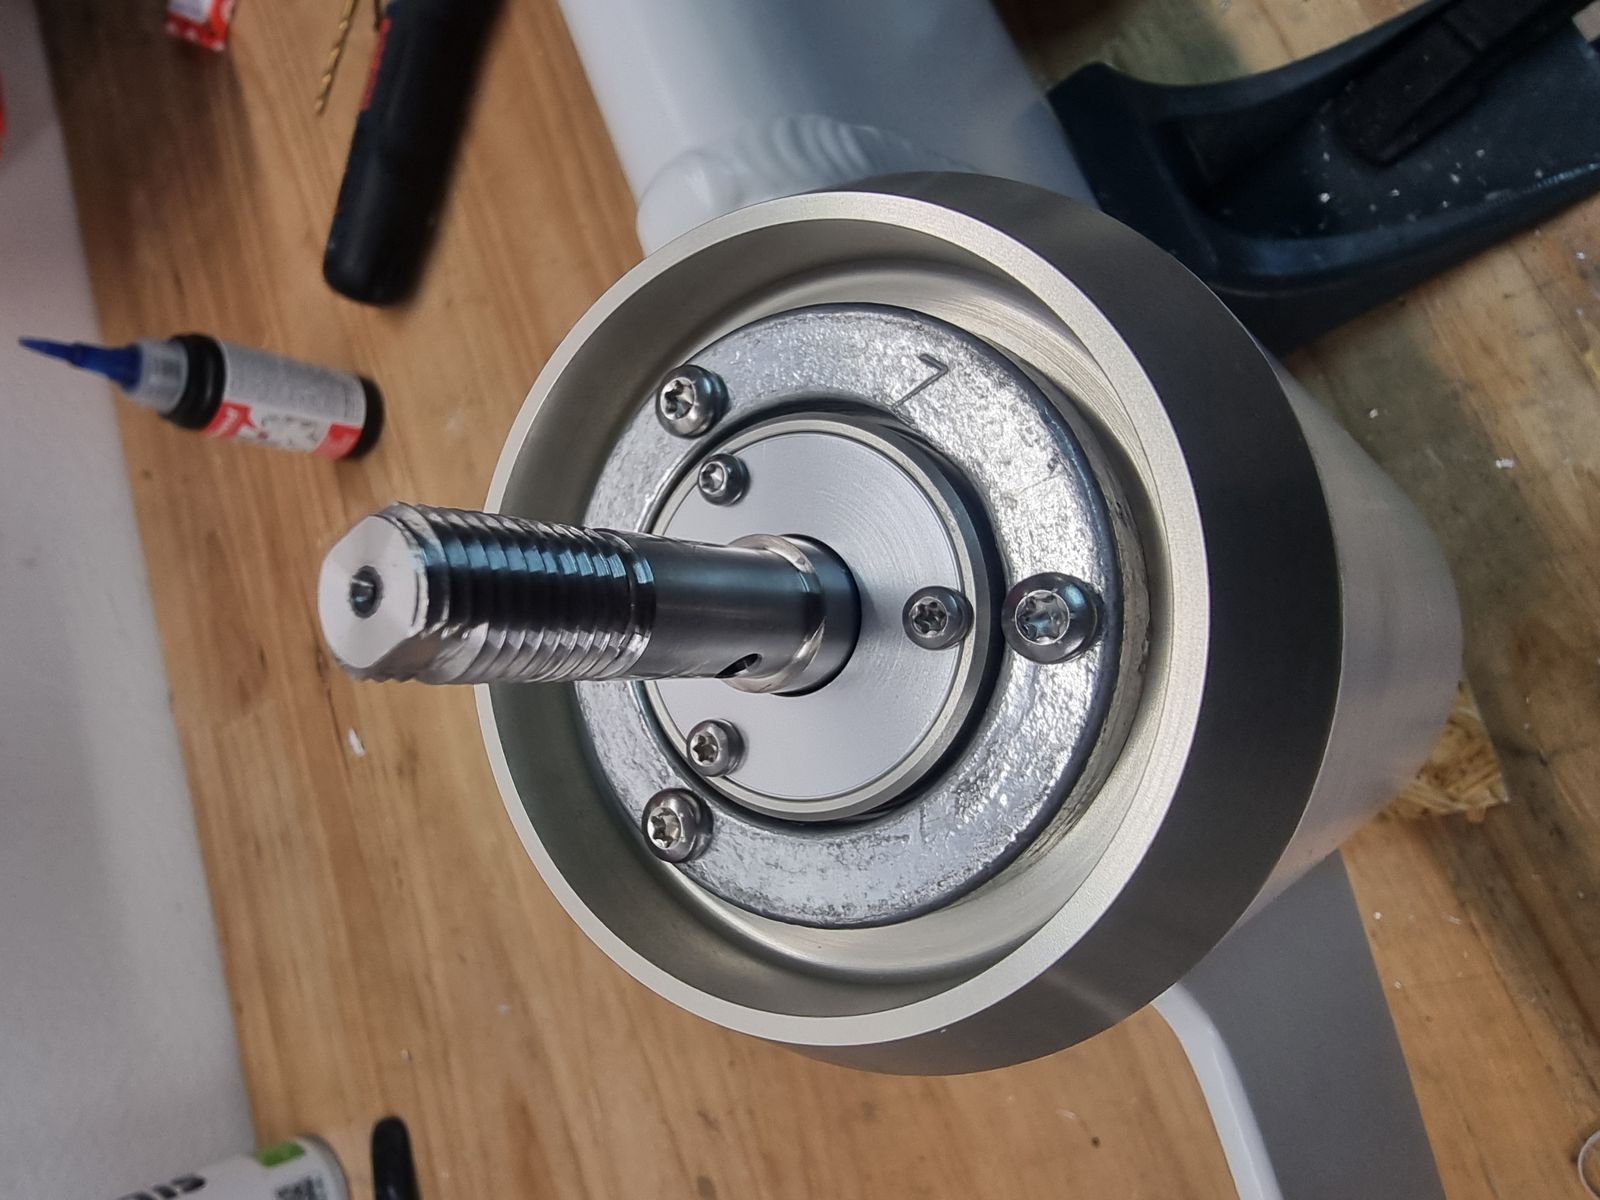
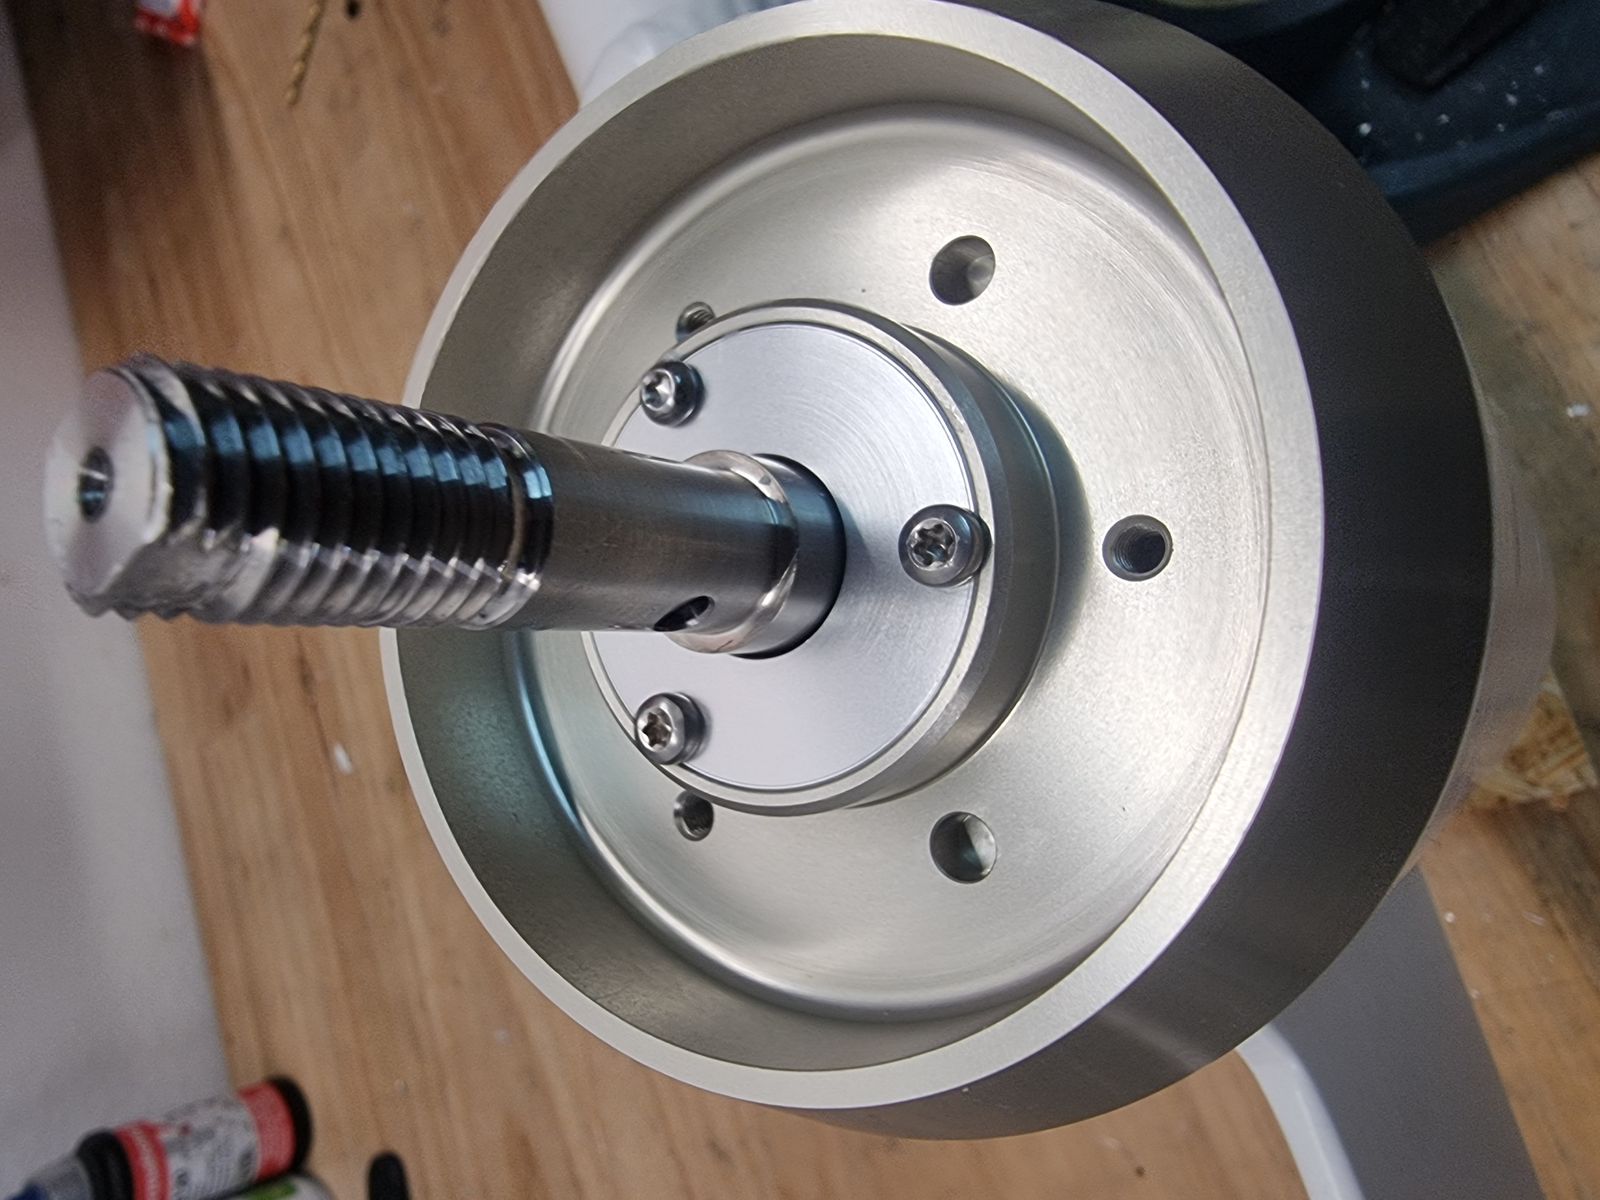
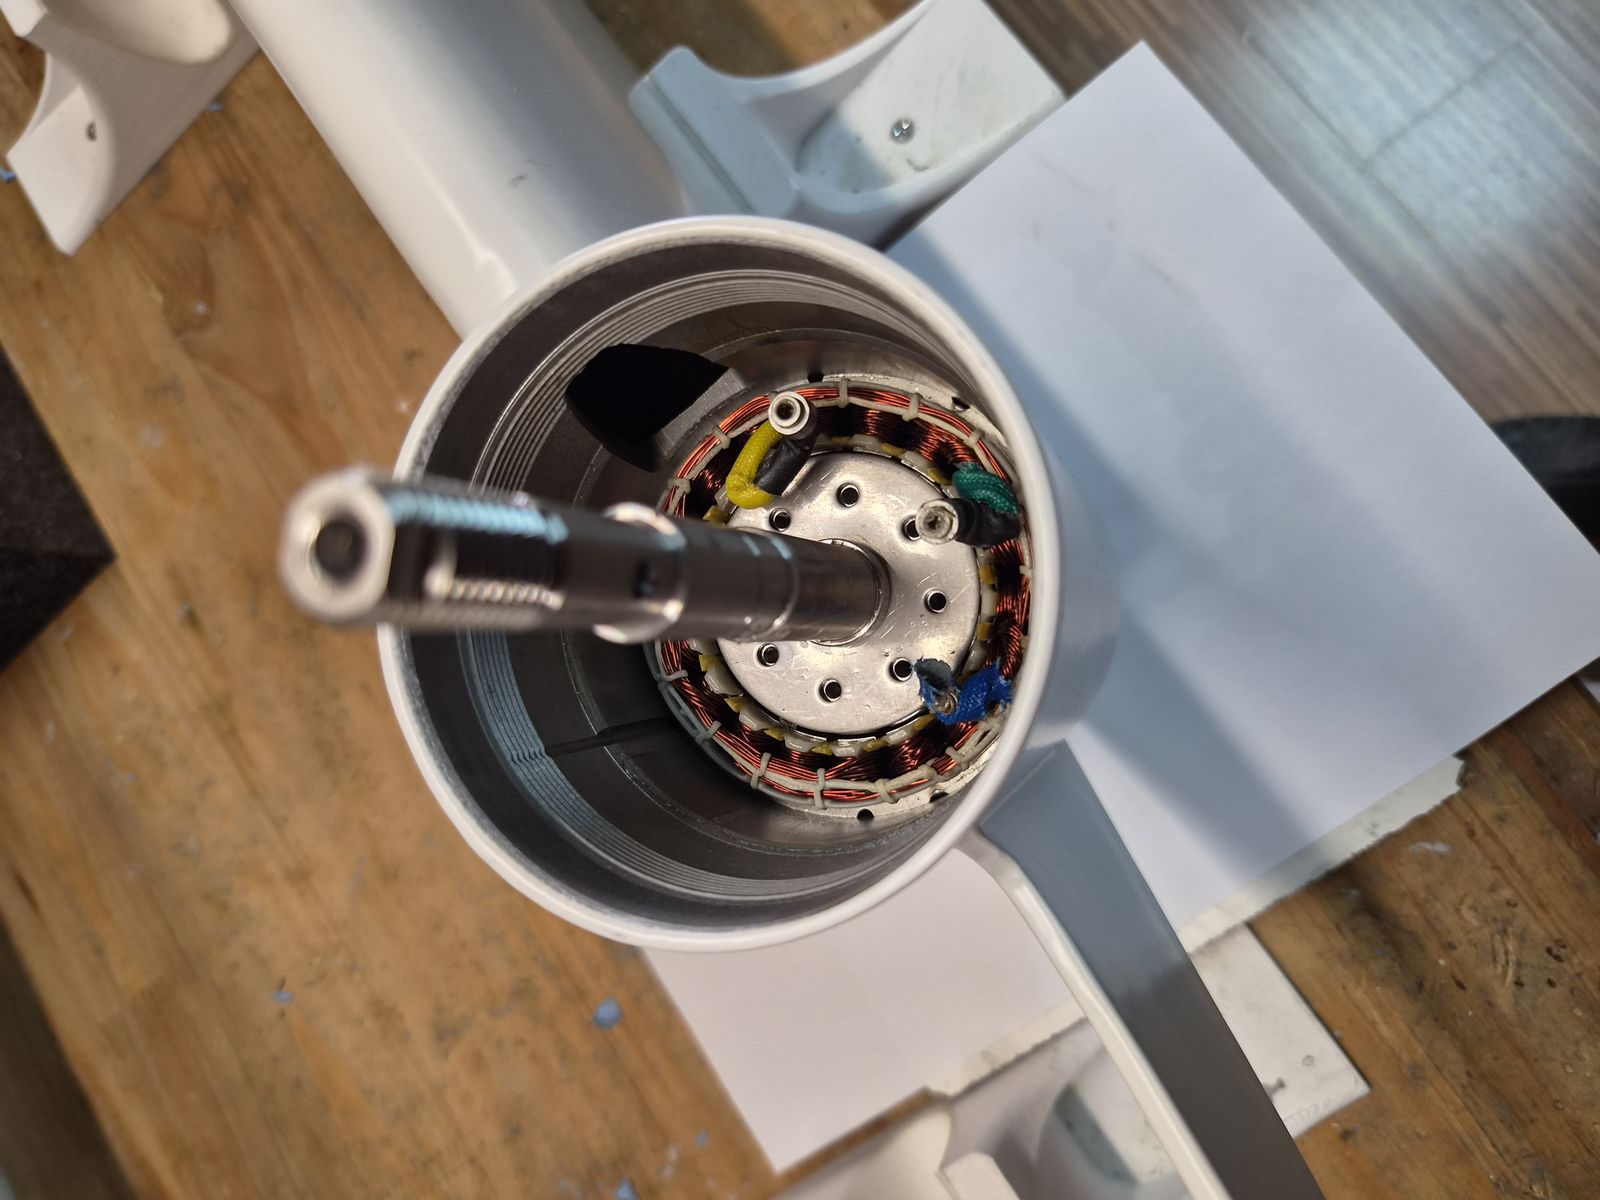
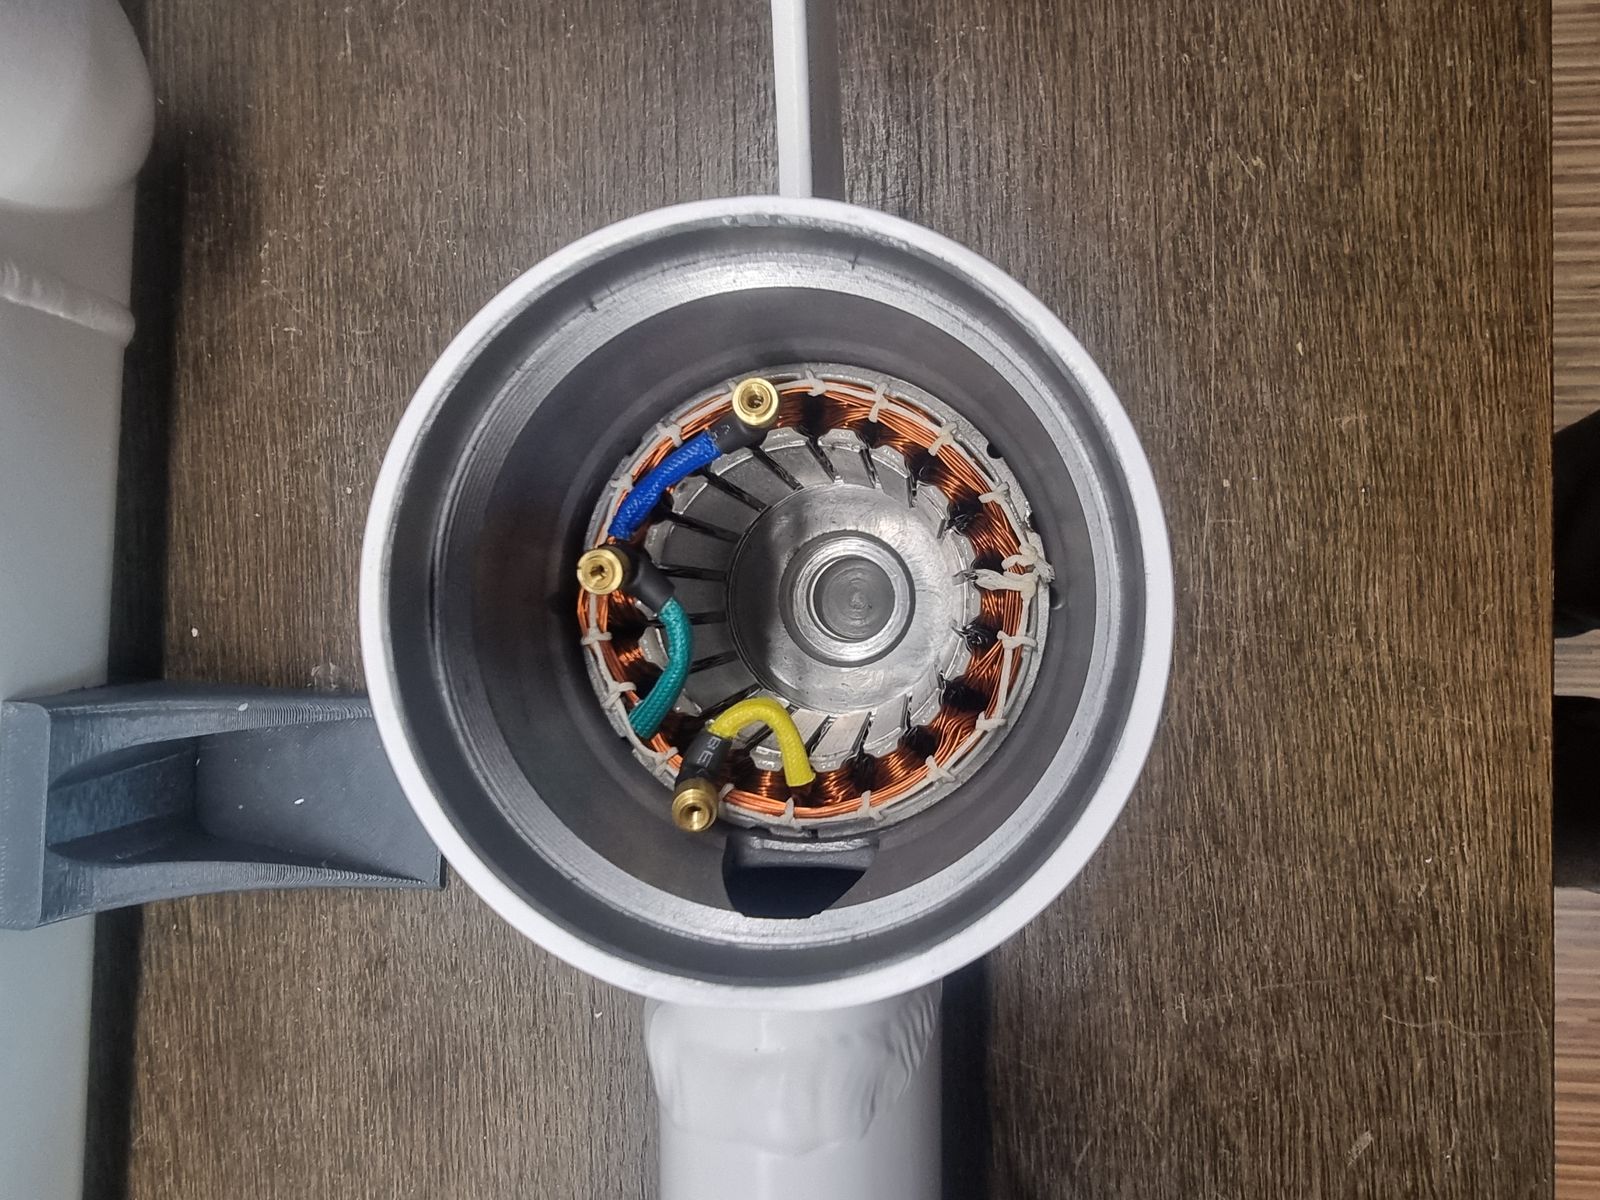
- Clean the motor housing of any debris.
Link to originalCAUTION
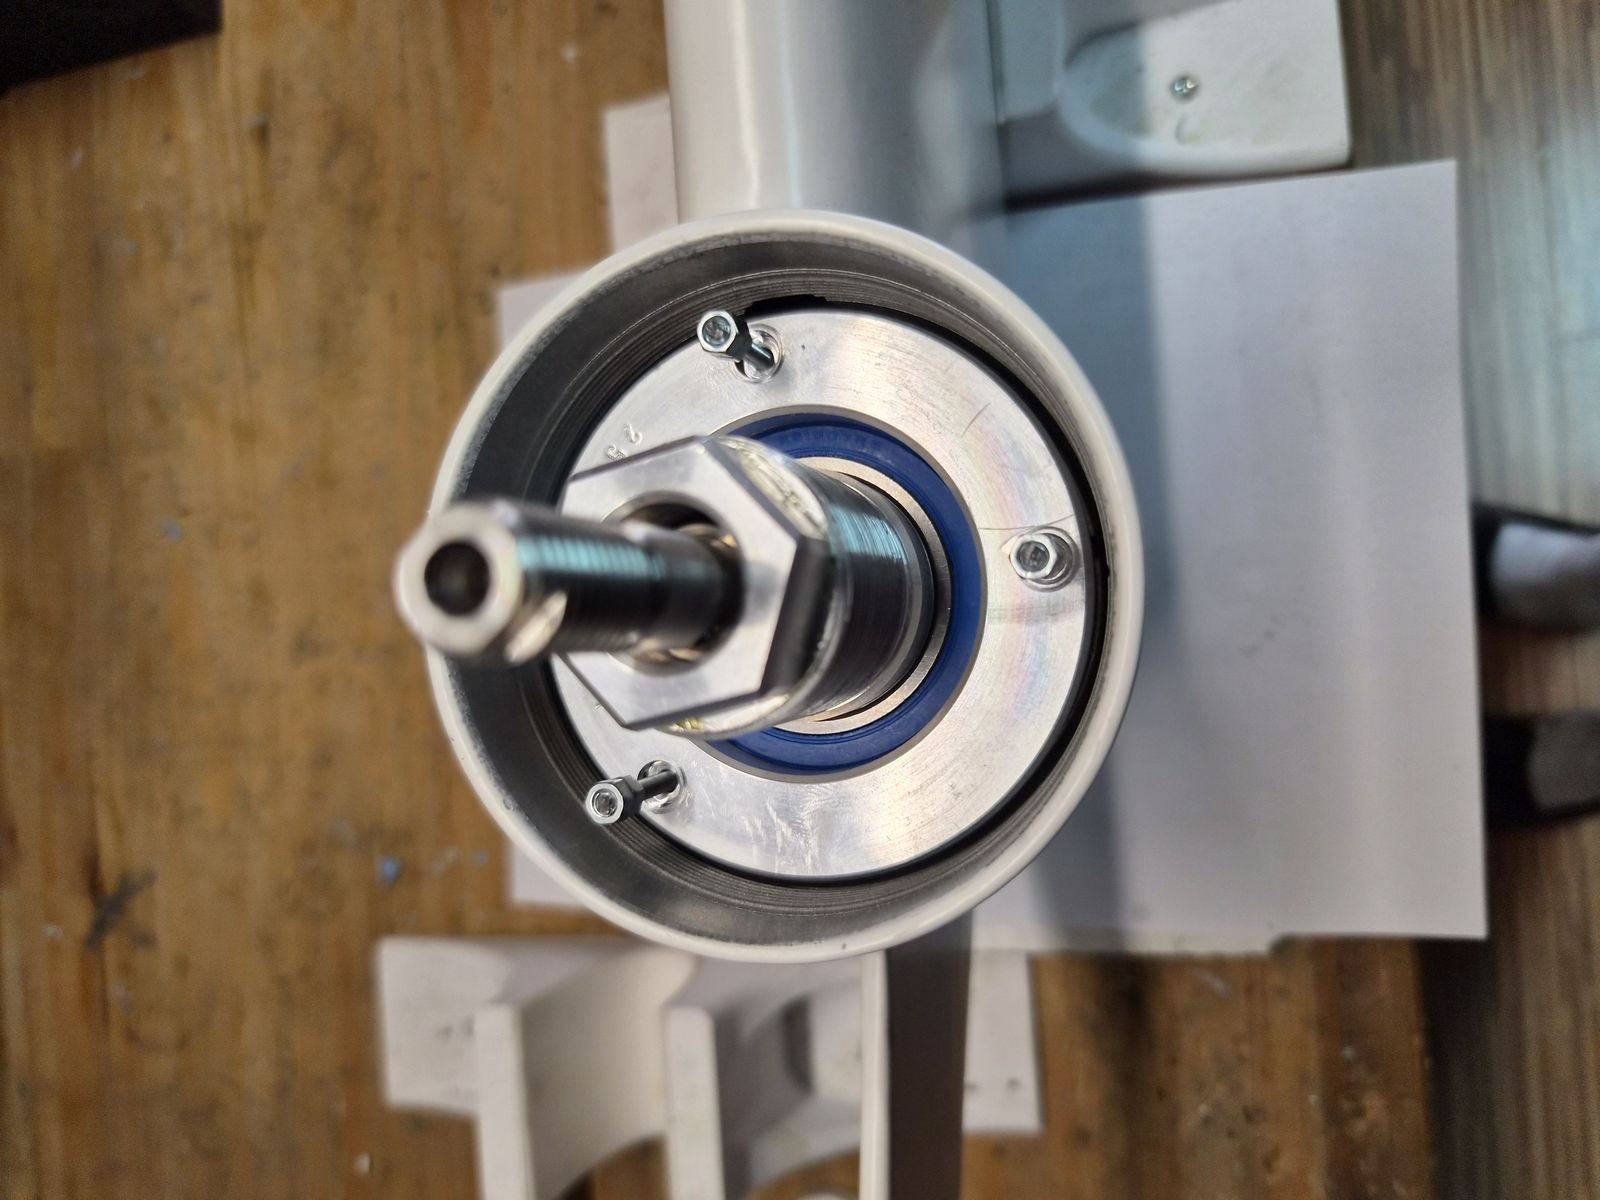
There may be a shim washer inside the bearing hole. Whether a shim is present is determined at initial manufacturing (based on the housing measurement) — it is not something to add or remove during service. If a shim is present, make sure it does not fall out during disassembly, and reinstall the same shim during assembly (see DT-ASM-002 ASSEMBLY STEP 2 - Install shim washer if required).
Check
DT-CHK-004 CHECK STEP 4 - Inspect stator and motor housing
Tools:
- No tools required.
Procedure:
- Inspect the motor housing bore for damage, corrosion or leftover adhesive after cleaning.
- Inspect the removed stator windings for damage, discoloration or signs of overheating.
- Inspect the rotor for damage to the magnets or shaft.
Link to originalTODO
Define the acceptance criteria for stator winding condition and motor housing bore wear, and confirm whether a stator with cosmetic damage can be reused.
DT-CHK-002 CHECK STEP 2 - Inspect bearings and radial shaft seals
Tools:
- No tools required.
Procedure:
- Inspect the rotor shaft and bearing seats for scoring, corrosion or damage.
- Inspect the wave spring washer for deformation or damage. Replace if damaged.
- Inspect the housing lid and O-ring contact surfaces for cuts, scratches or corrosion.
CAUTION
🗑 Do not reuse the removed Bearing 6202 ZZ (013010001) bearings, Radial shaft seal 15x25x5 (017020001) or O-ring 70x4 (017010001). Always install new bearings, seals and O-rings during assembly.
Link to originalTODO
Define the acceptance criteria for shaft/bearing seat wear (e.g. maximum scoring depth, corrosion limits) and the wave spring washer damage tolerance.
DT-CHK-001 CHECK STEP 1 - Inspect propeller, shear pin and anode
Tools:
- No tools required.
Procedure:
- Inspect the propeller for bent, cracked or missing blades and check the propeller hub for damage.
- Inspect the shaft for visual damage, especially in the area of the propeller and washer seat.
- Inspect the anode for wear. Replace if worn beyond the acceptance criteria.
CAUTION
🗑 The Shear pin (901050006) and Safety nut M12 A4 (011020005) must not be reused. The shear pin is designed to fail under overload and the safety nut loses its locking torque once removed — always install new ones.
Link to originalTODO
Define the anode wear acceptance criteria (e.g. minimum remaining material) and the propeller damage acceptance criteria (nick/bend limits before replacement is required).
NOTE
The current source manuals do not include a dedicated stator removal step. If the stator is replaced separately from the motor housing, add the approved removal method here.
Reassembly from motor housing and stator
Service always receives the motor housing with the stator already inserted and bonded — the stator cannot be separated from a shrink-fitted housing, so this spare part comes pre-assembled from production. No stator insertion/bonding is done in the field; reassembly starts by fitting the rotor into the new housing.
If the removed rotor is undamaged (see Check section), reuse it as-is and skip the rotor bearing steps below (Inspect rotor / Press bearing onto rotor / Check pressed bearing position / Install external circlip) — only fit a new Rotor (100020002) if the old one is damaged.
DT-ASM-007 STEP 7 - Inspect rotor
Tools:
Installing parts:
Procedure:
- Inspect the rotor sealing surface for damage.
- Inspect the magnets for visible imperfections.
- Measure the tolerance deviation: ø15, -0,00 / +0,06.
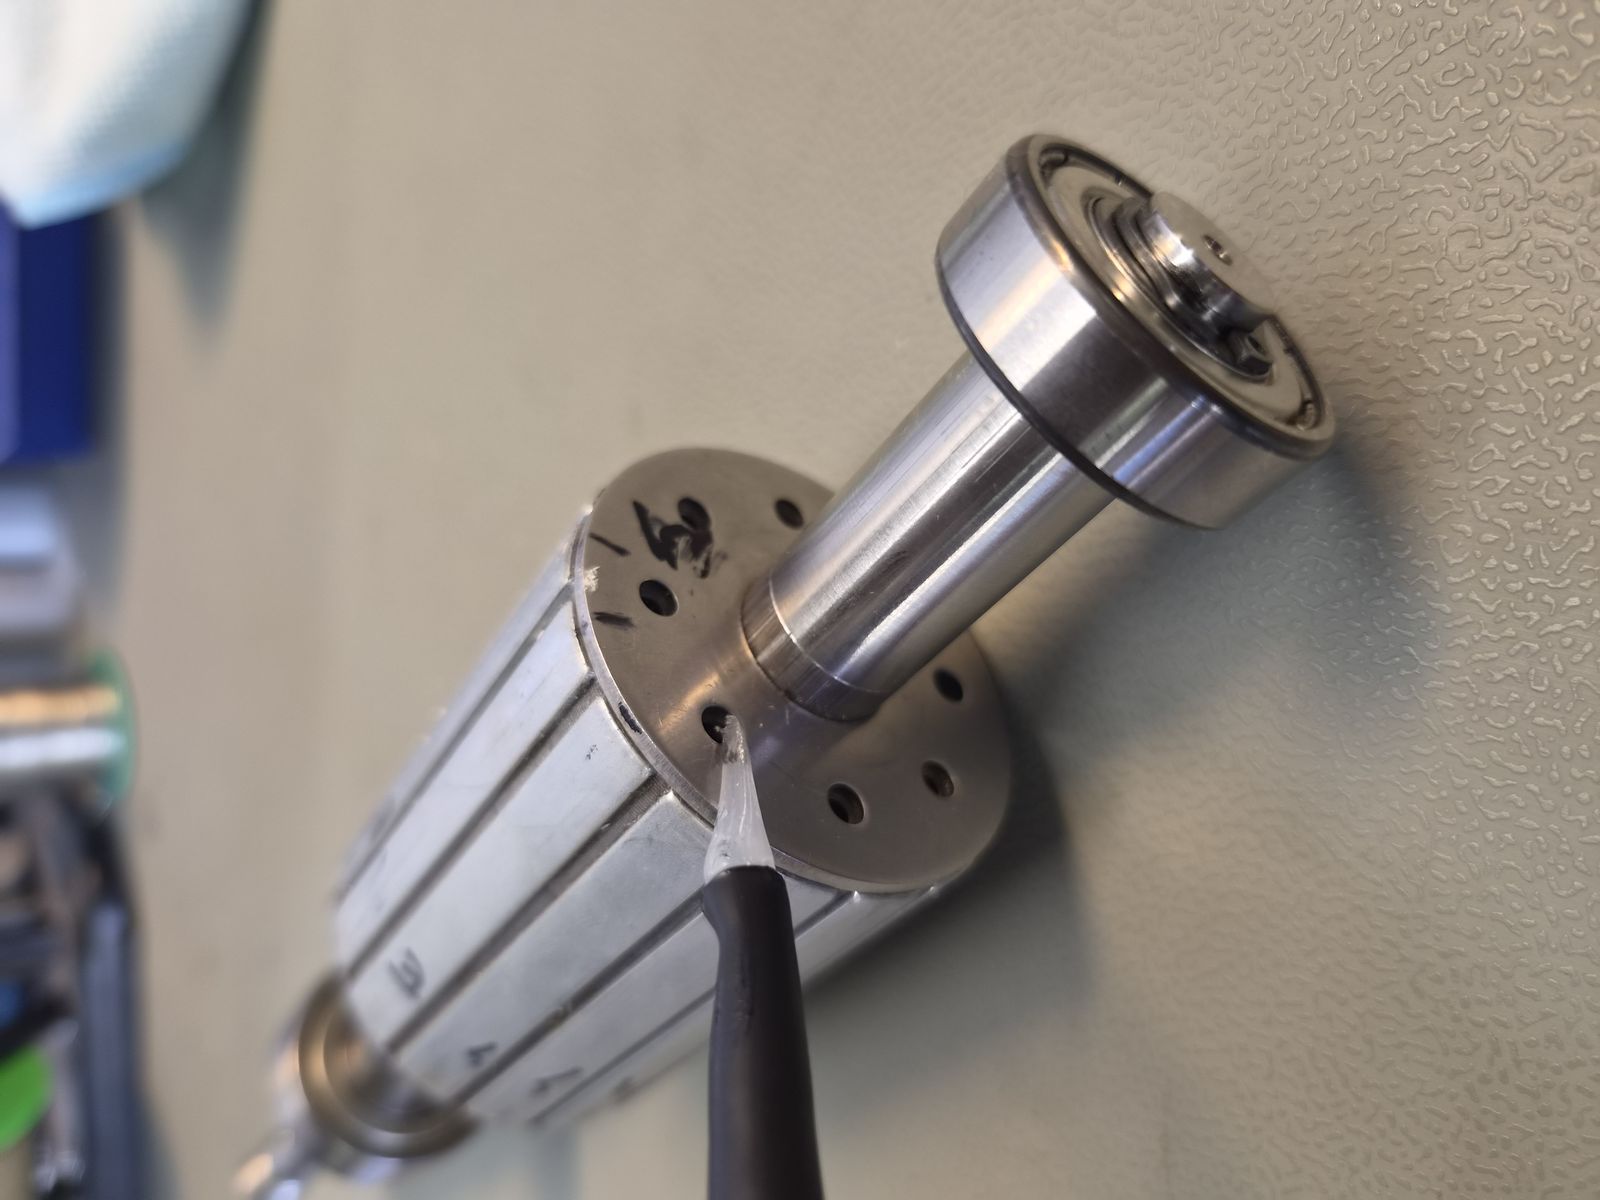
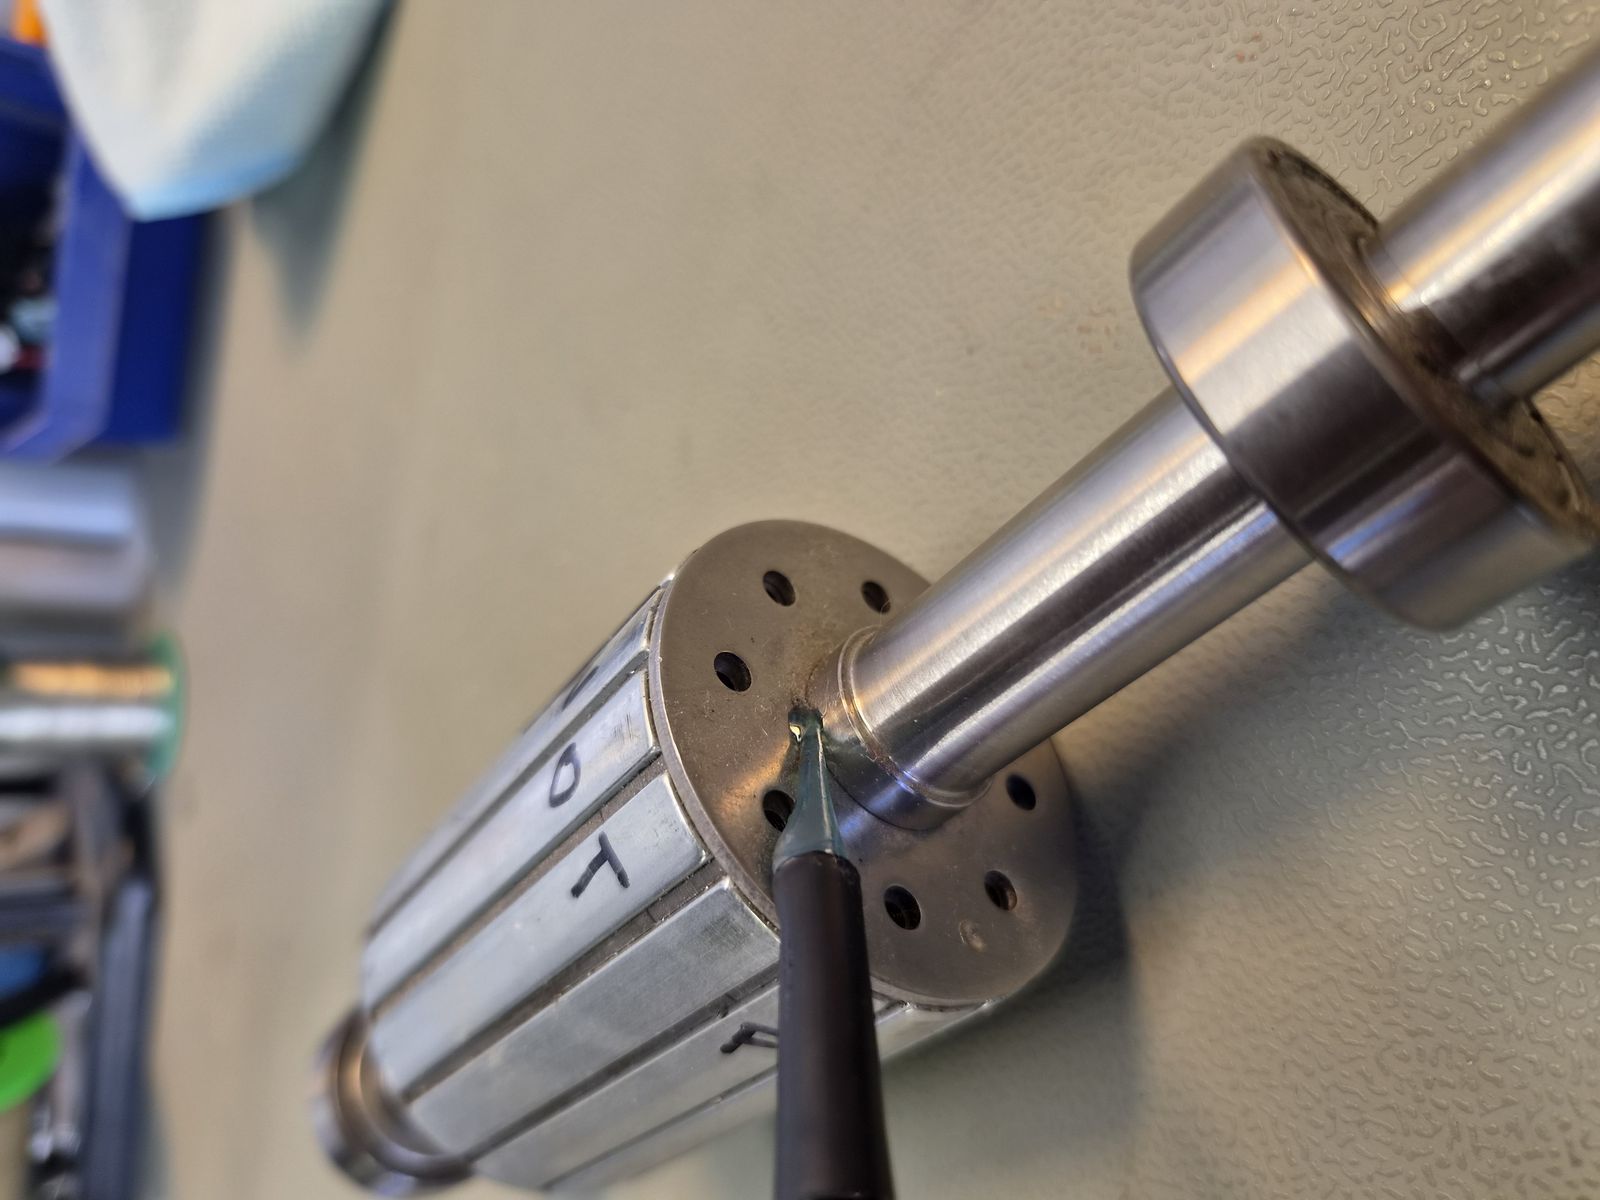
- The balancing ring is already fitted by the supplier — dispense a small amount of adhesive into the balancing ring hole(s) to additionally secure it.
WARNING
The rotor contains strong magnets. Keep fingers clear of pinch points and keep magnetic-sensitive items away from the rotor.
Link to originalTODO
Confirm the exact adhesive used and how many holes are typically filled.
DT-ASM-008 STEP 8 - Press bearing onto rotor
Tools:
Installing parts:
Procedure:
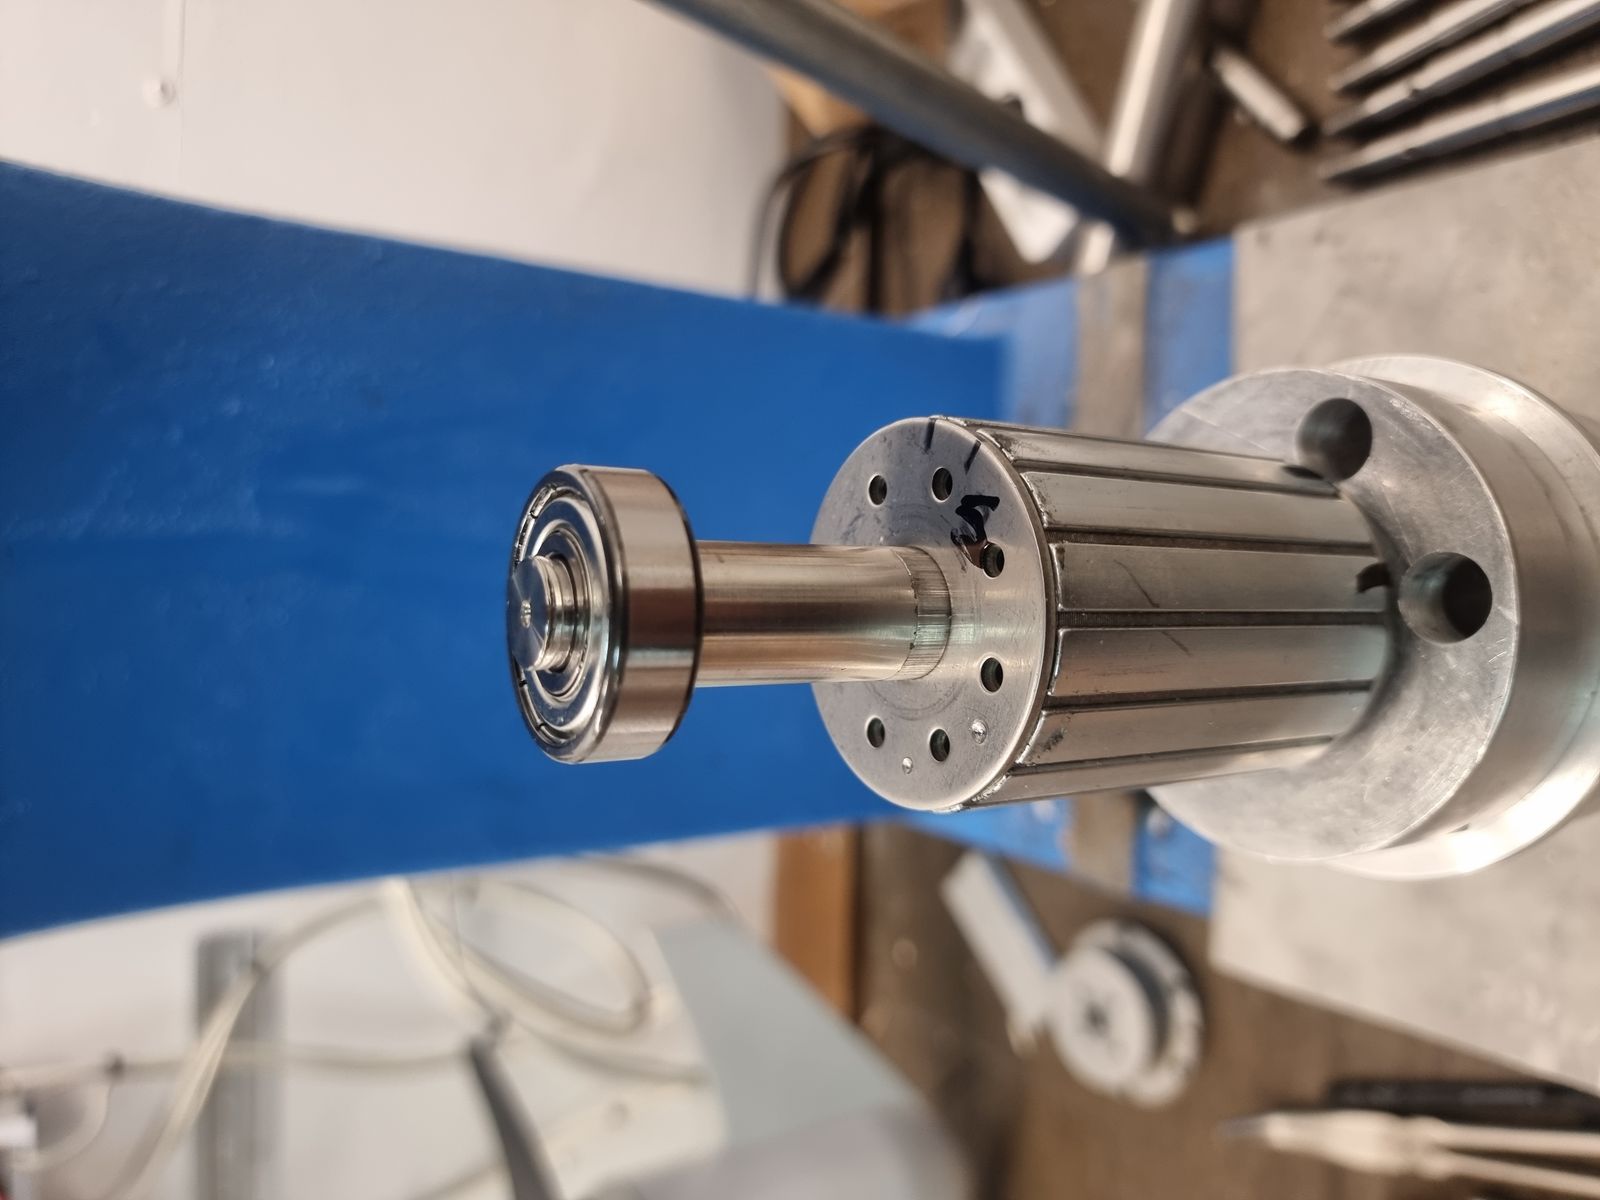
- Place the rotor with the longer side of the shaft into the pedestal.
- Use the bearing press tool to mount the bearing onto the shaft.
Link to originalCAUTION
Press only on the correct bearing ring. Incorrect pressing can damage the bearing.
DT-ASM-009 STEP 9 - Check pressed bearing position
Tools:
- No tools required.
Procedure:
Link to original
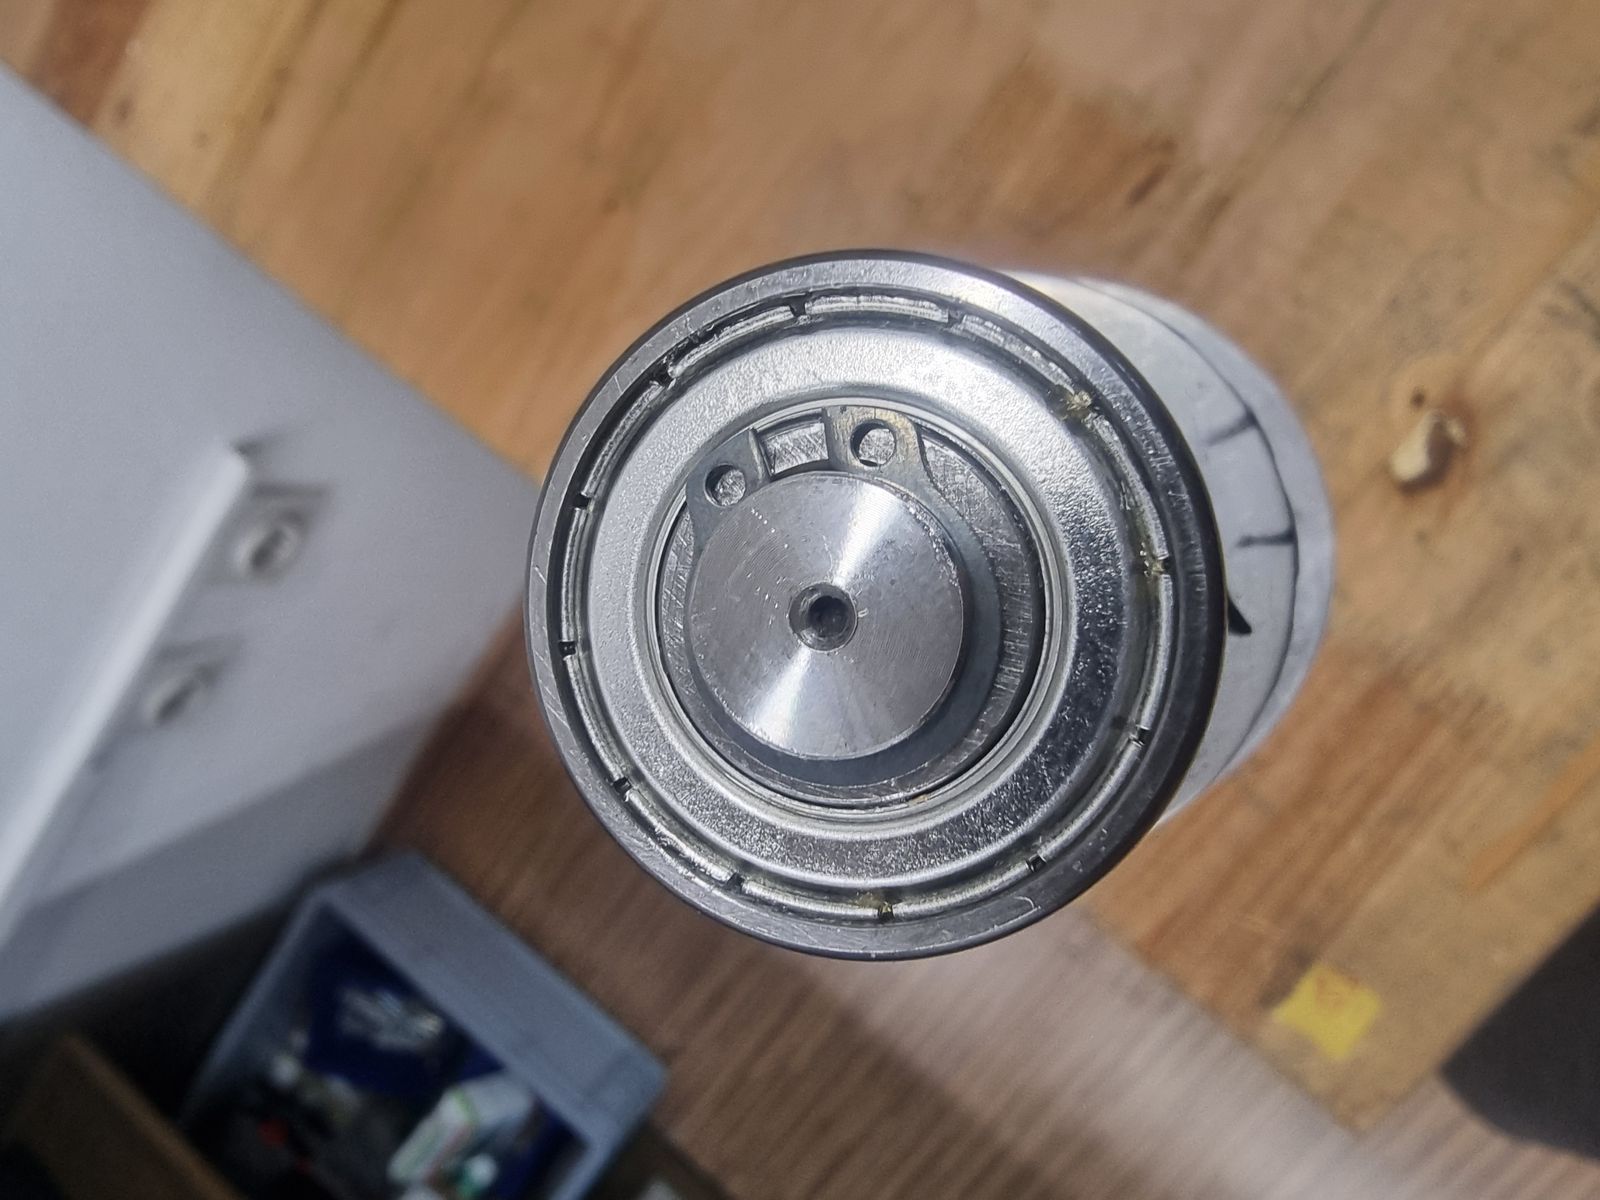
- Check that the bearing is fully pressed on.
- Make sure that the circlip slot is fully exposed.
DT-ASM-010 STEP 10 - Install external circlip
Tools:
Installing parts:
Procedure:
- Mount the circlip using circlip pliers.
- Check that the circlip is fully seated.
Link to originalCAUTION
Make sure the circlip is fully seated in the groove before continuing.
DT-ASM-011 STEP 11 - Install shim washer if required
Installing parts:
- Shim washer 25x35x0.5 DIN988 (if required)
Procedure:
- If required, place a shim washer 25x35x0.5 DIN988 at the bottom of the motor housing bearing seat before inserting the rotor.
Link to originalTODO
Define the required insertion depth and tolerance. Add measurement procedure to determine whether a shim washer is needed and specify the correct shim thickness.
DT-ASM-012 STEP 12 - Insert rotor into motor housing
Tools:
- No tools required.
Installing parts:
Procedure:
- Insert the rotor into the motor housing.
- Insert the rotor bearing into the designated hole in the bottom of the housing.
- Check the insertion depth.
- The top of the rotor magnets must be in line with the steel laminations.
Link to originalWARNING
The rotor contains strong magnets. Keep fingers clear of pinch points during insertion.
DT-ASM-013 STEP 13 - Install heat sink
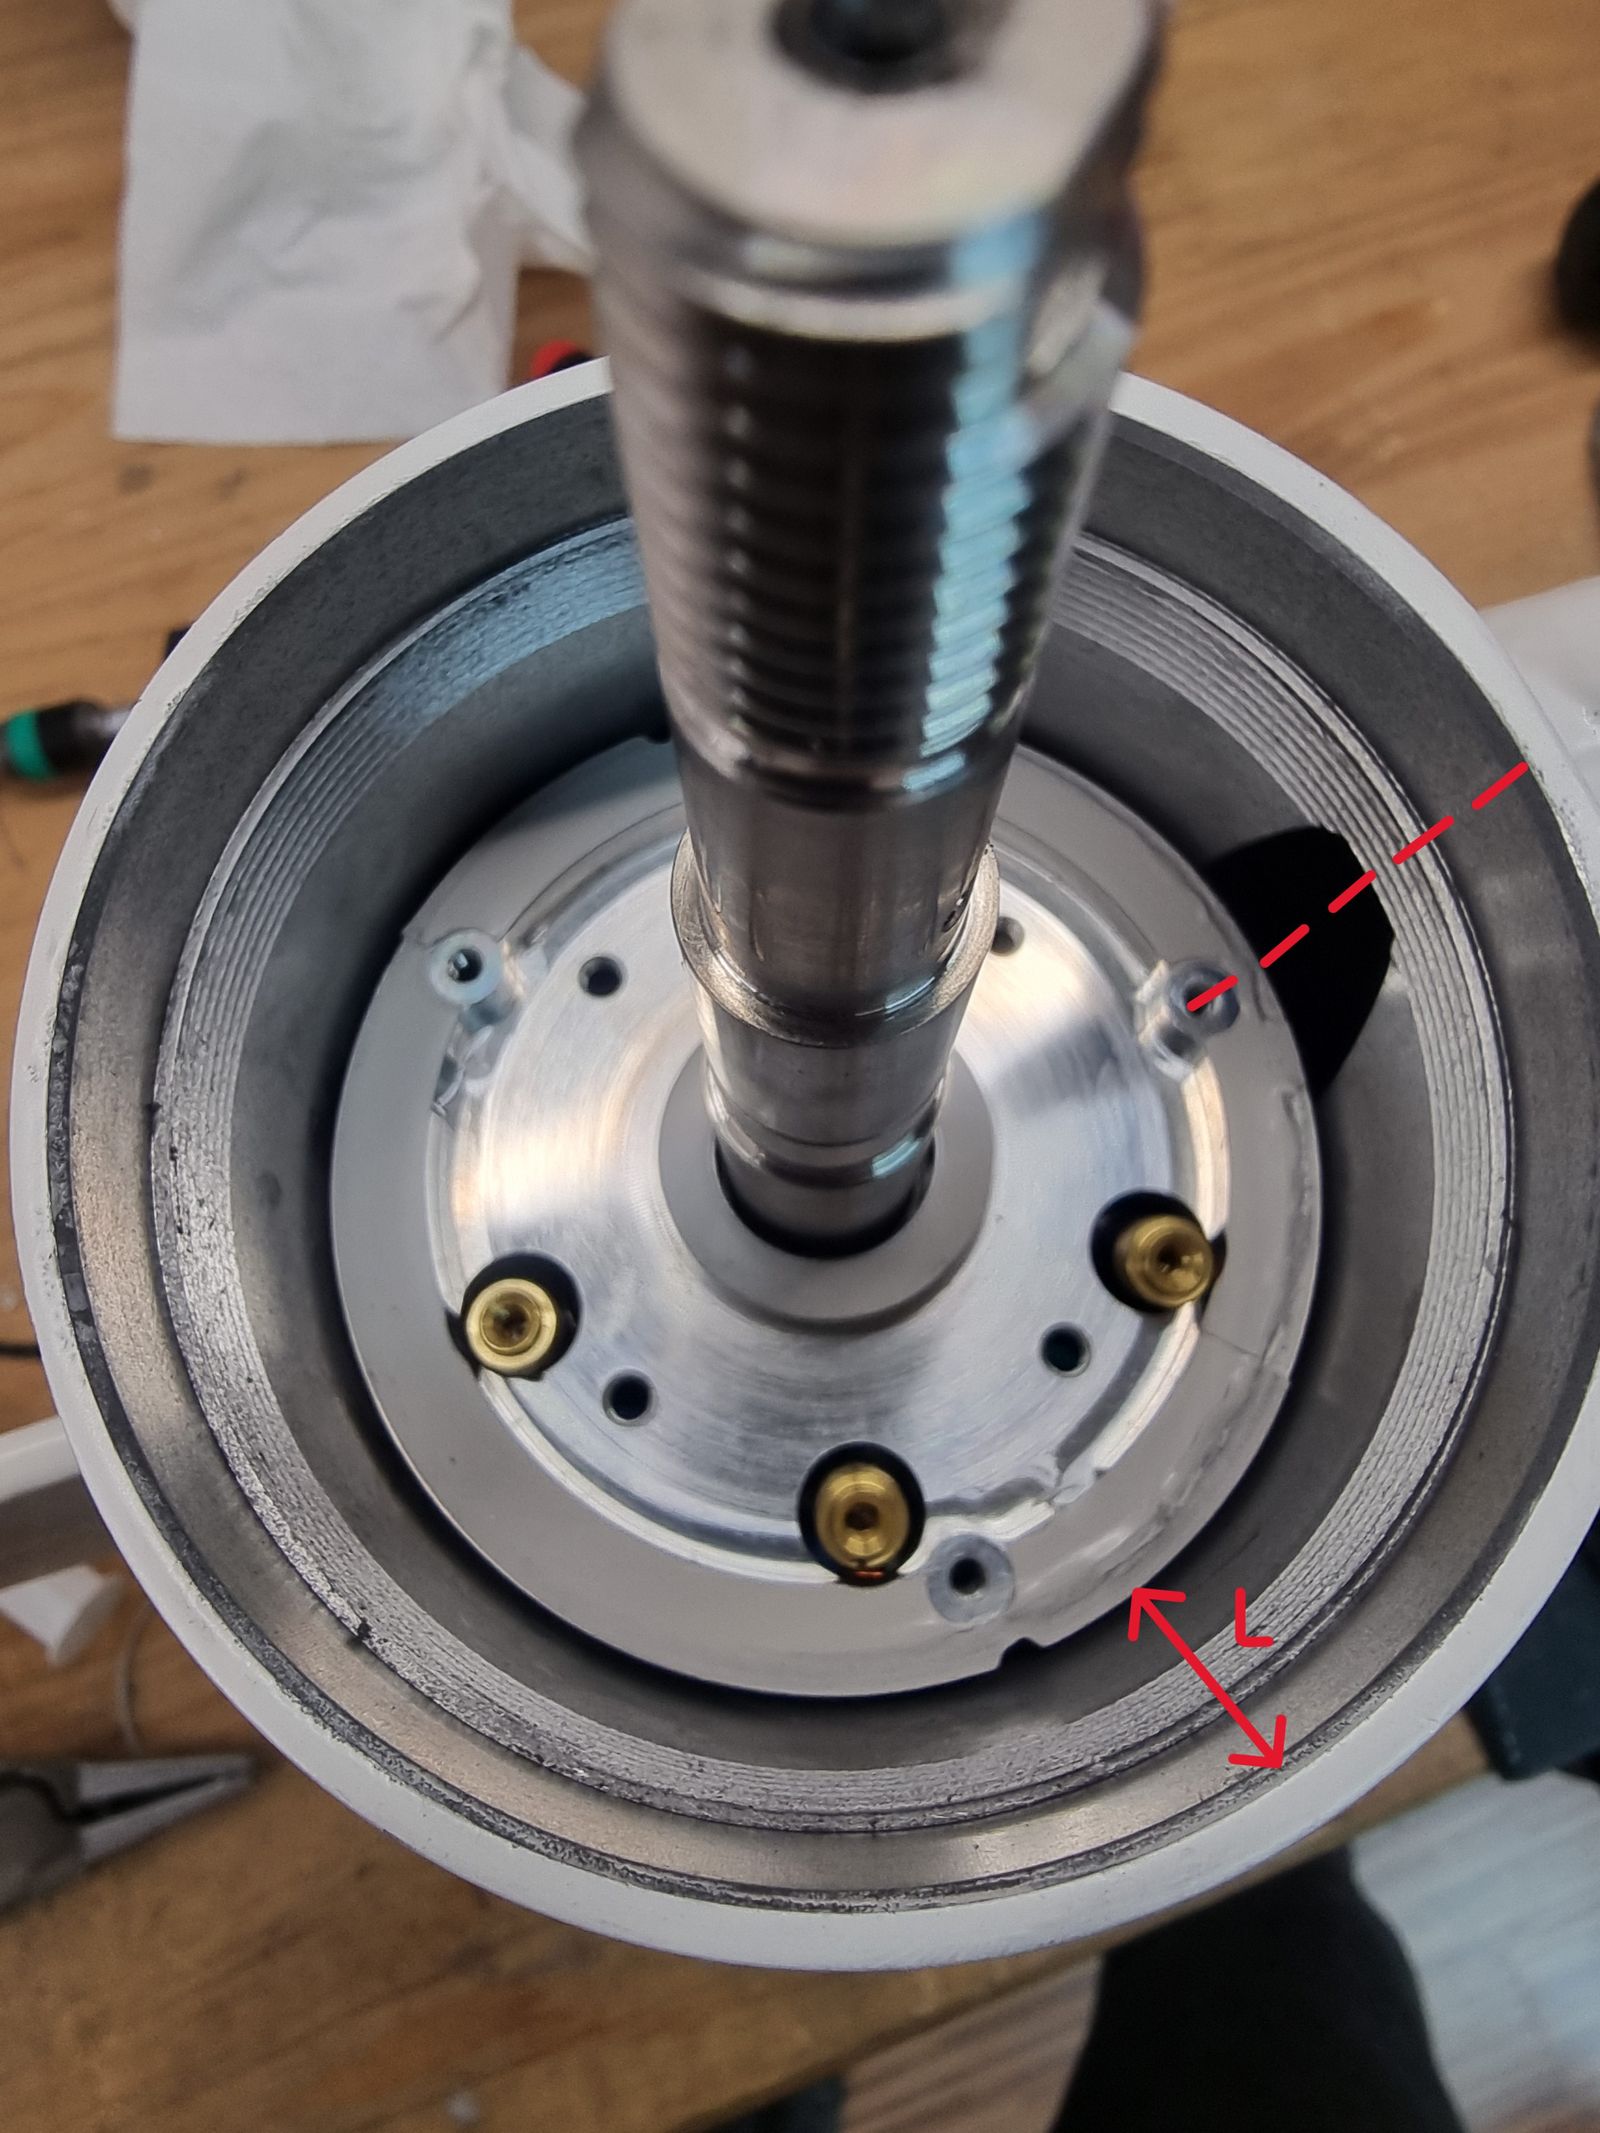
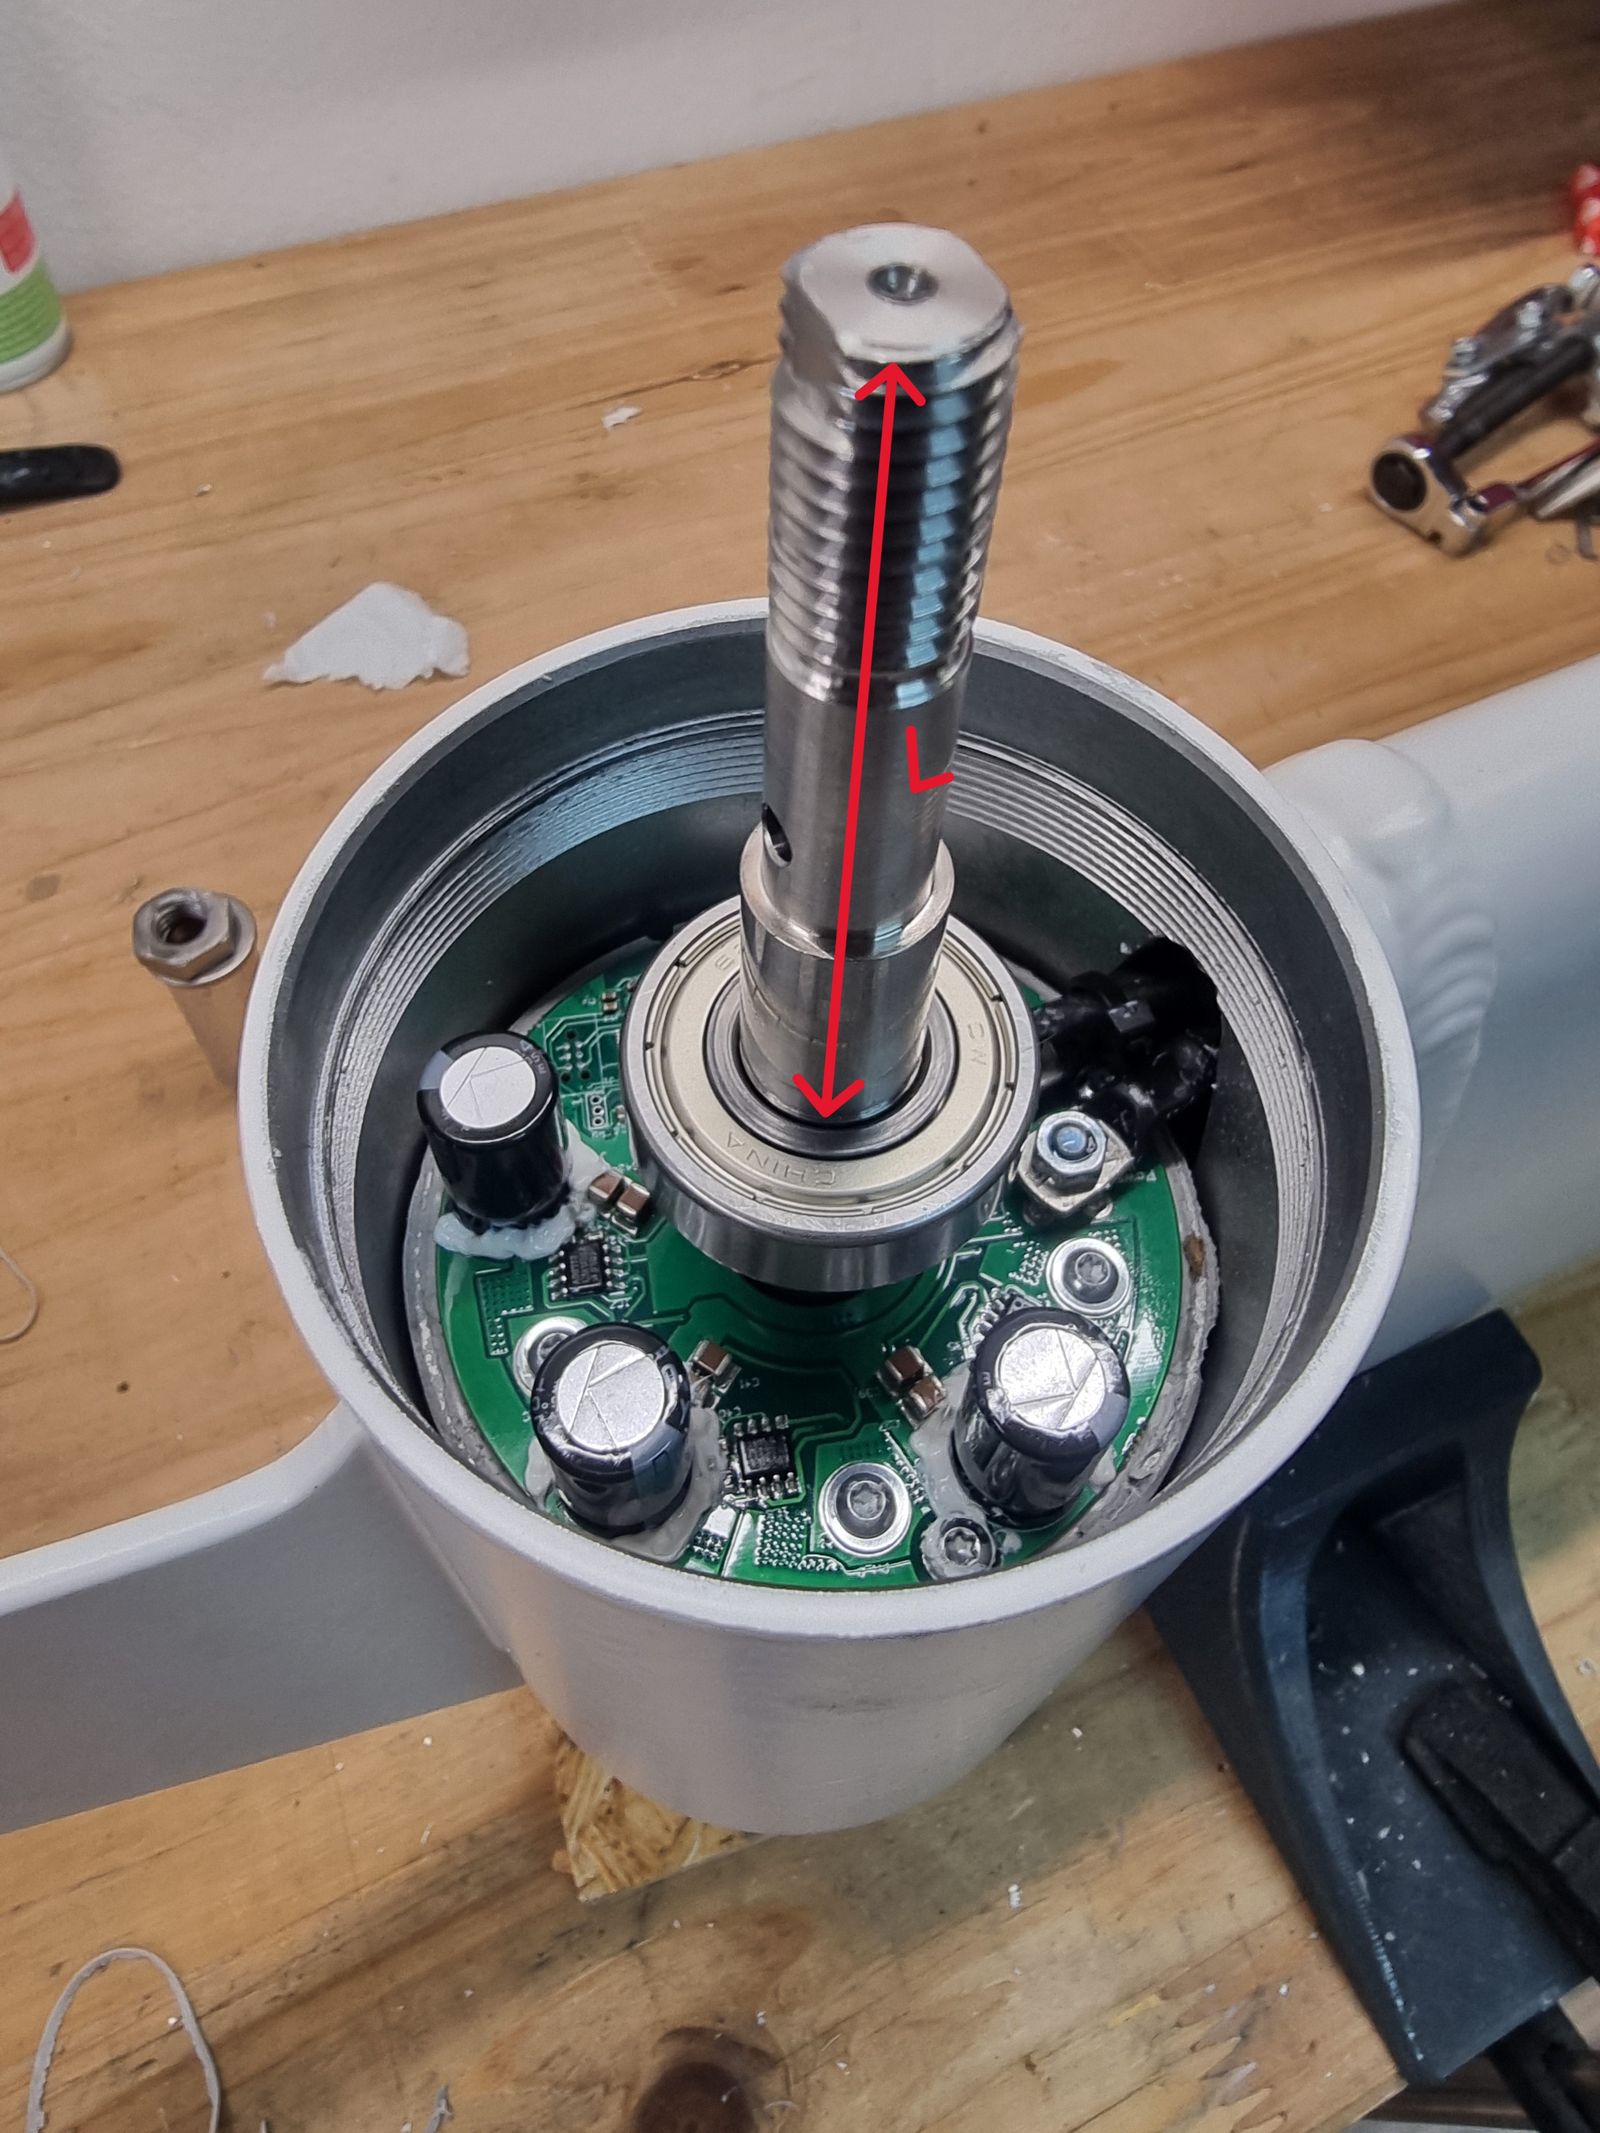
The dashed line marks the housing edge for rough alignment; L is the depth measured down to the heat sink face.
Tools:
Consumables:
Installing parts:
Procedure:
- Apply a thin coat of silicone spray to the outer diameter of the heat sink to ease installation.
- Align the heat sink holes with the phase cables.
- Insert the heat sink into the motor housing.
- Press the heat sink until it reaches L = 42,3 mm from the top edge of the housing.
Link to originalCAUTION
Check the heat sink depth with a digital caliper. Adhesive is no longer applied at this step.
DT-ASM-014 STEP 14 - Apply thermal paste to heat sink
Apply a thin, even layer of thermal paste to the flat contact surface of the heat sink before mounting the motor controller.
Tools:
- No tools required.
Installing parts:
Consumables:
Procedure:
- Apply a thin, even layer of thermal paste to the flat contact surface of the heat sink — the surface that will be in direct contact with the motor controller PCB.
- Spread the paste evenly to cover the entire contact surface.
Link to originalCAUTION
Apply thermal paste only to the flat contact surface. Keep paste away from screw holes and connector contacts.
DT-ASM-015 STEP 15 - Install motor controller
Tools:
Installing parts:
- PCBA Motor Controller (701010001)
- Screw M3x4 ZN (011010005)
- Screw M3x5 ZN (011010003)
- Washer 3,2-8-0,5 ZN (011030006)
Procedure:
- Bolt the phase terminals to the controller using M3x4 screws and washers.
- Bolt down the motor controller using M3x5 screws.
Torque specification:
- M3 screws: 1,3 Nm
Link to originalCAUTION
The motor controller must only be handled in an ESD-protected environment. Use appropriate ESD protection to prevent damage to electronic components.
DT-ASM-016 STEP 16 - Connect and secure cables
Tools:
Consumables:
Installing parts:
Procedure:
- Bolt down the power cables onto the red cube phase terminals on the motor controller PCB.
- Make sure the power cables do not touch the motor housing.
- Apply a small amount of Permabond A130 to the nut threads to secure them against vibration.
- Plug in the signal cable.
- Fix the signal cable to the GND cable using a zip tie.
Torque specification:
- Red cube (phase terminal), M4 nut: 1,2 Nm
Link to originalCAUTION
Make sure cables are routed away from sharp edges and moving parts.
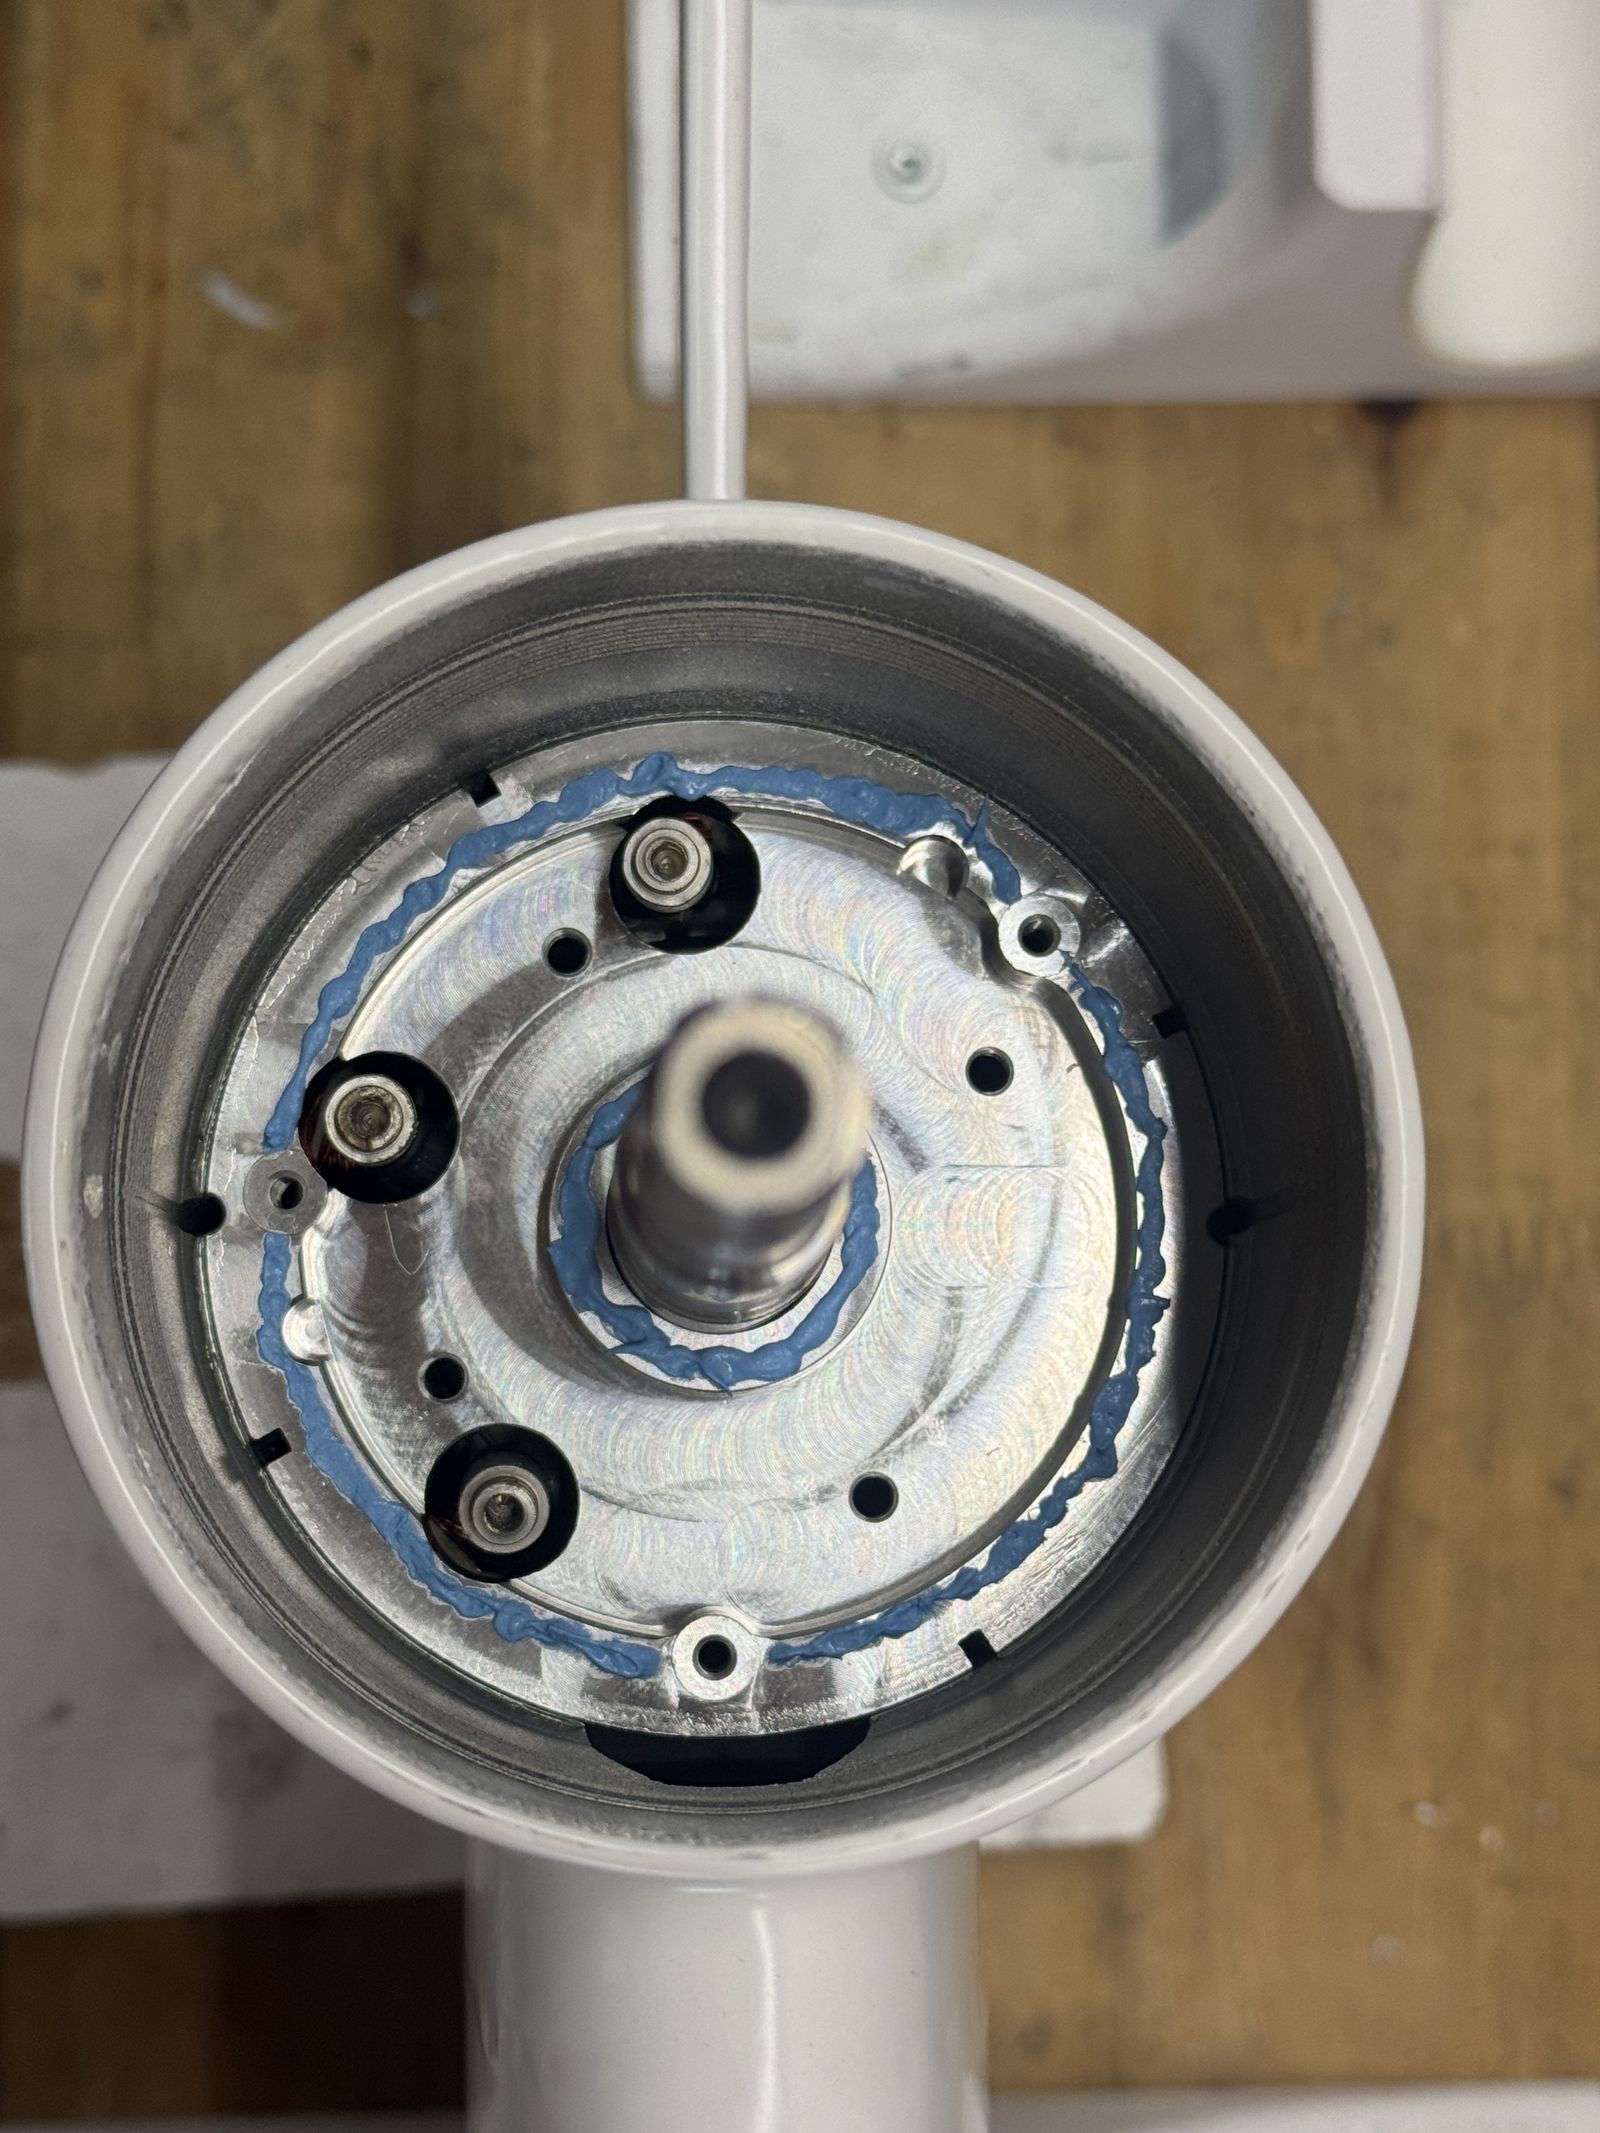
DT-ASM-017 STEP 17 - Apply silicone to PCBA area
Tools:
Consumables:
Procedure:
- Apply silicone around the electrolytic capacitors.
- Fill the smaller connector with silicone.
- Secure the signal cables to the connector with silicone.
Link to originalCAUTION
Do not apply silicone to connector contact surfaces unless specified.
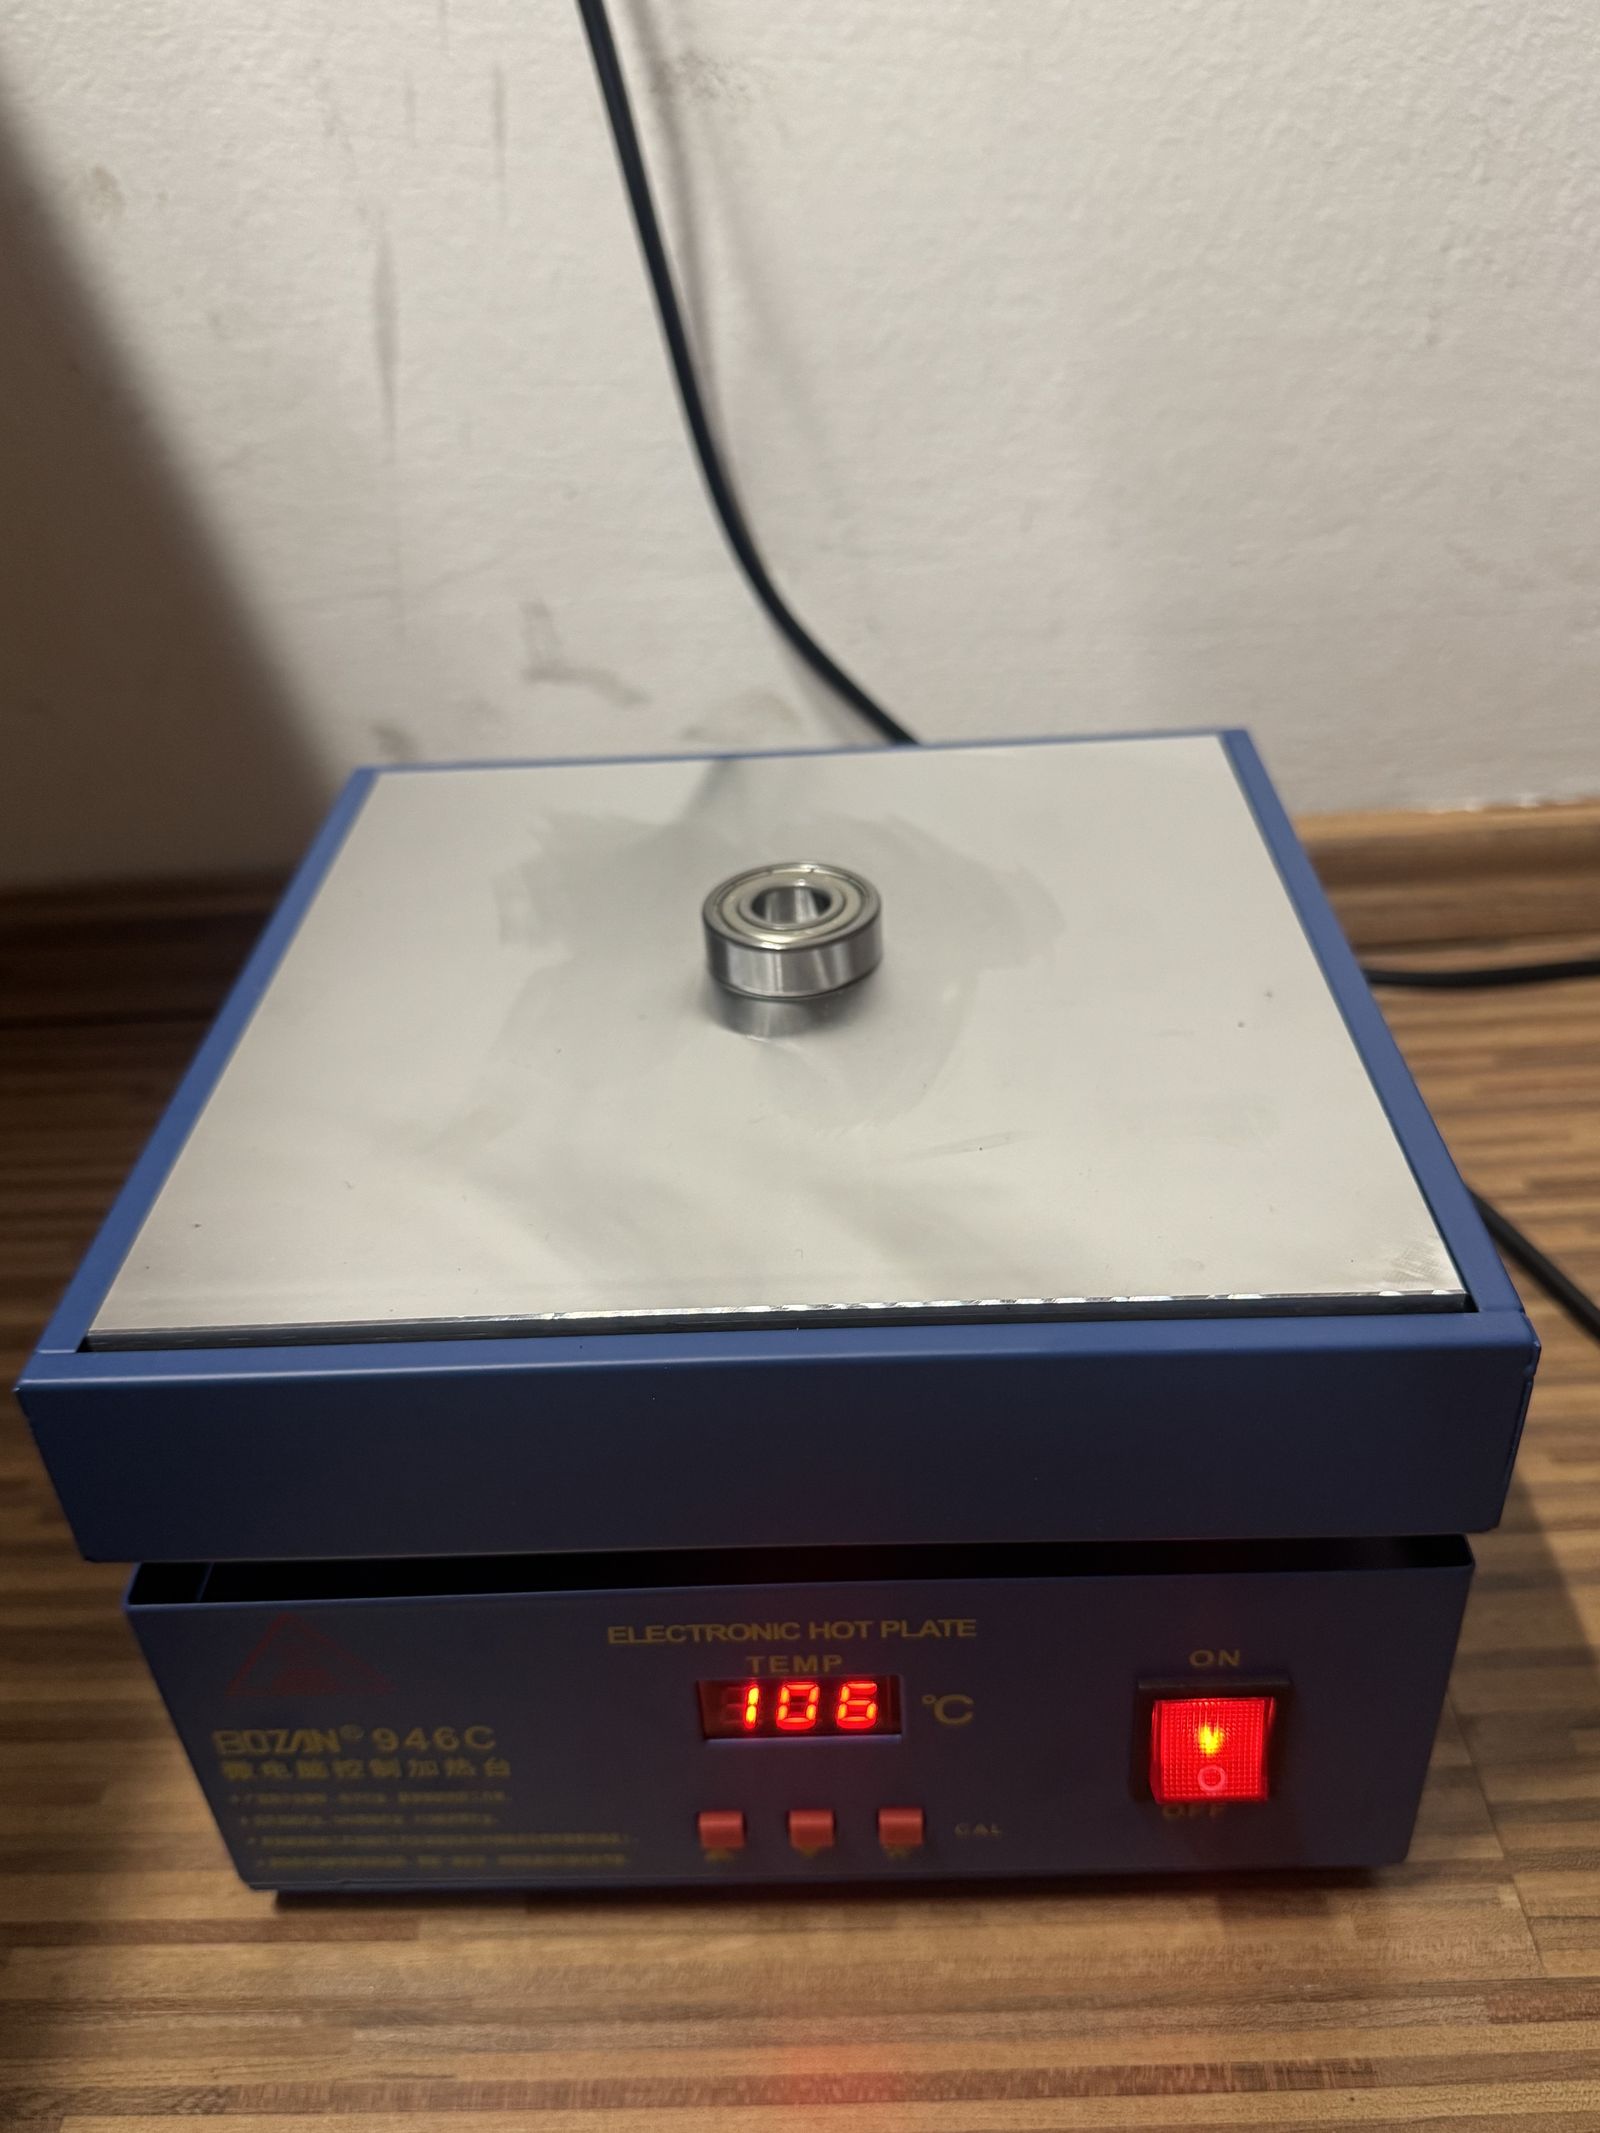
DT-ASM-018 STEP 18 - Preheat bearing
Bearing 6202 ZZ placed in the heating element set to 110 °C. Preheating expands the bearing for easier installation onto the shaft.
Tools:
Installing parts:
Procedure:
- Place the 6202 ZZ bearing into the heating element.
- Set the temperature to 110 °C.
- Allow the bearing to reach temperature before proceeding to installation.
WARNING
Preheat only the 6202 ZZ bearing — the one installed onto the shaft after the rotor is already in the housing. Do not preheat the 6201 ZZ bearing that is pressed directly onto the rotor shaft; that bearing is installed cold.
Link to originalCAUTION
Use thermal gloves when handling the heated bearing.
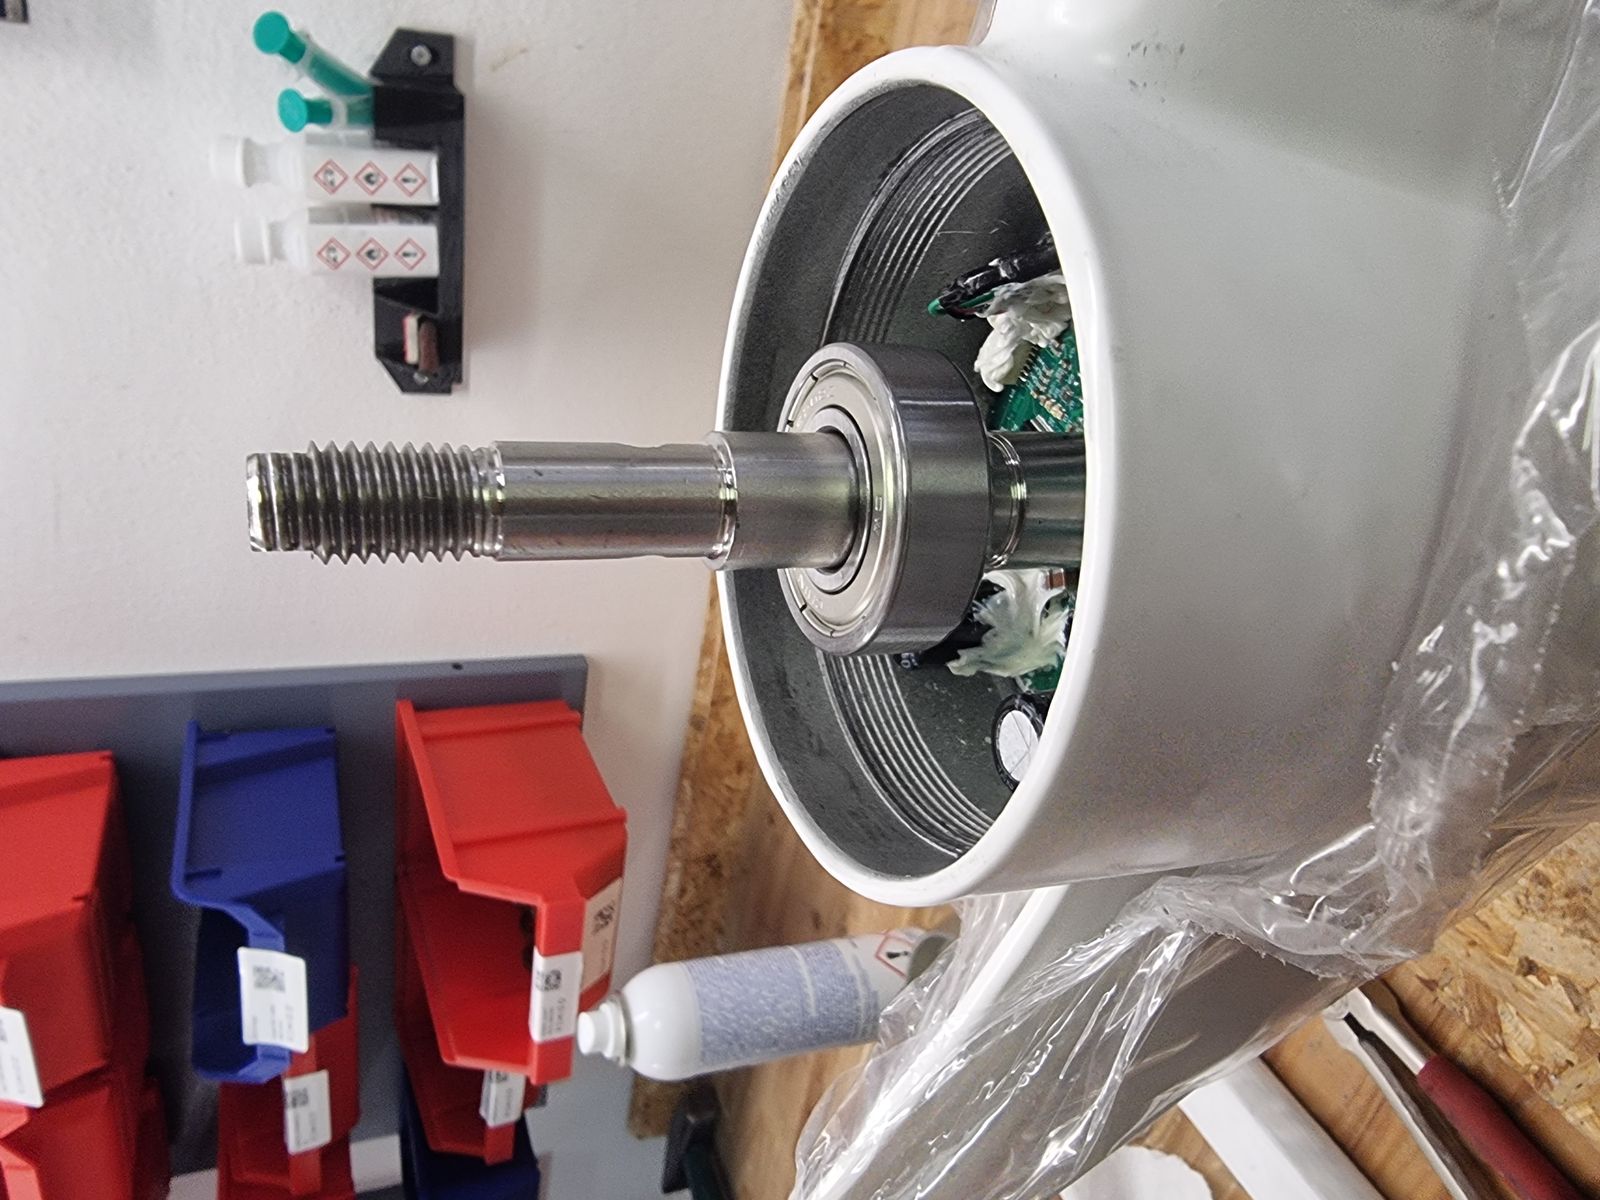
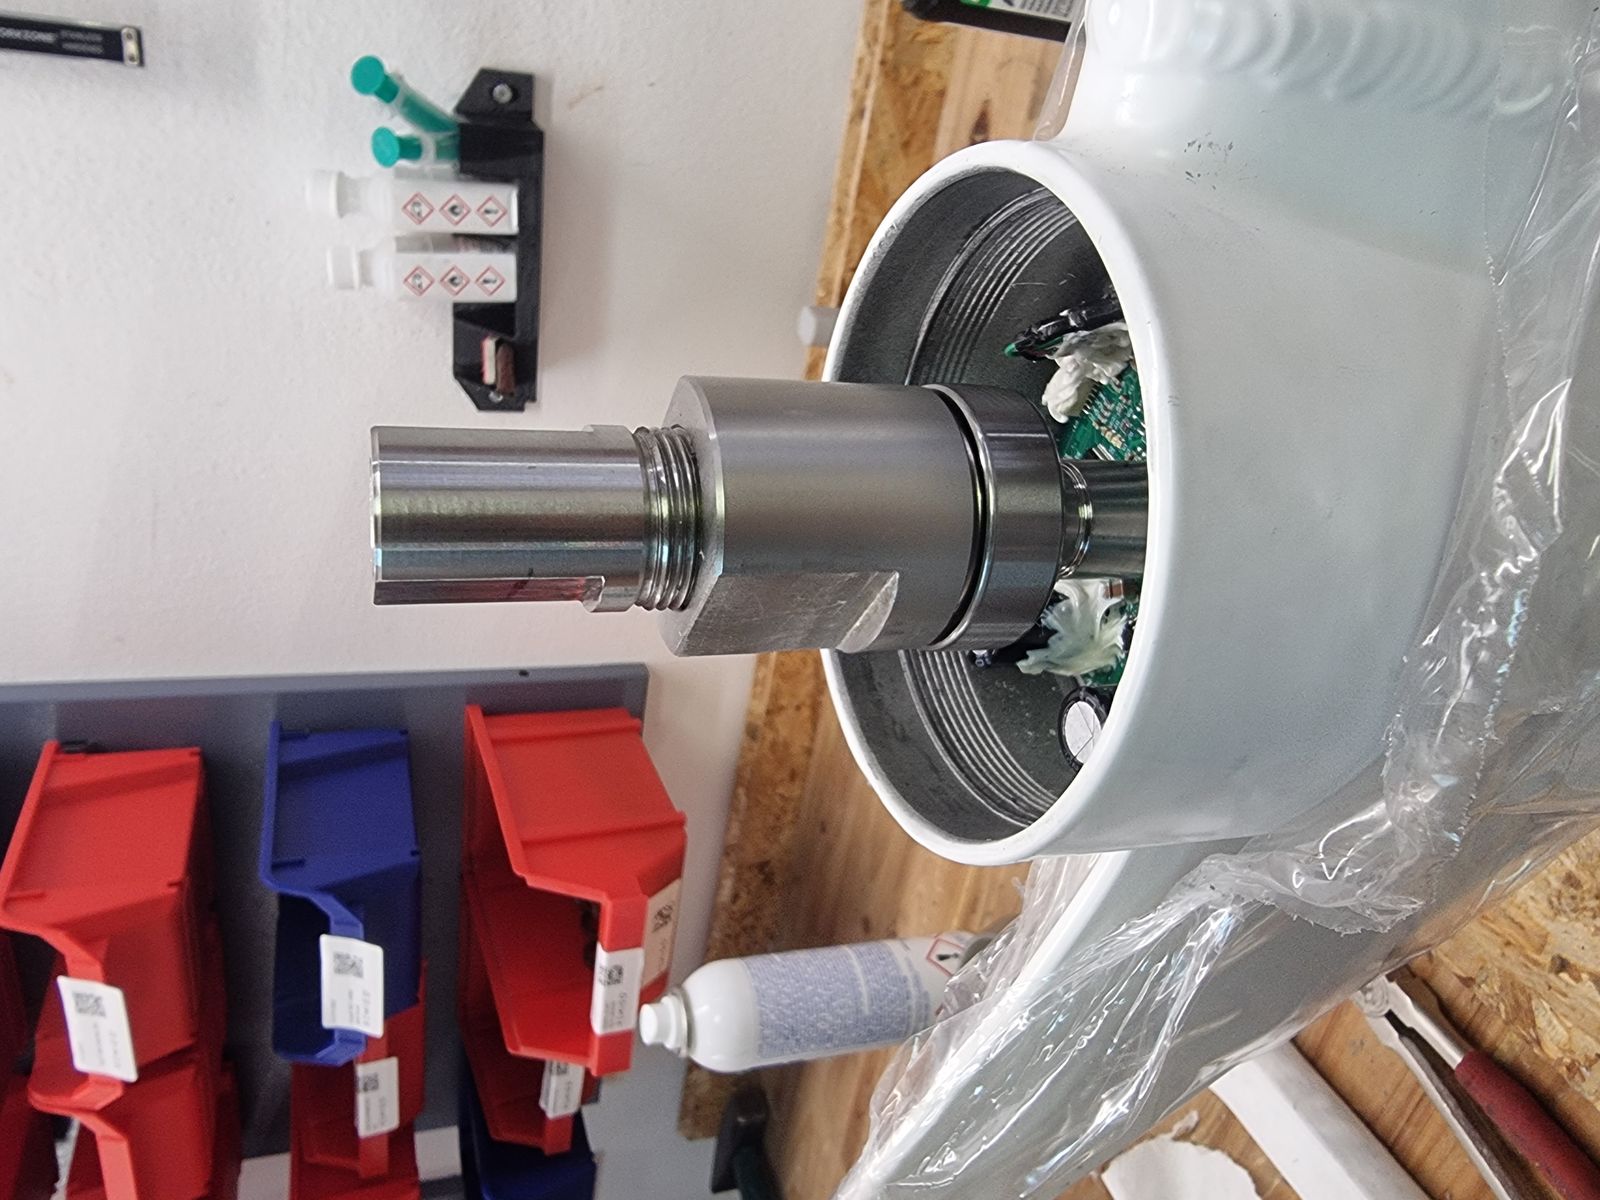
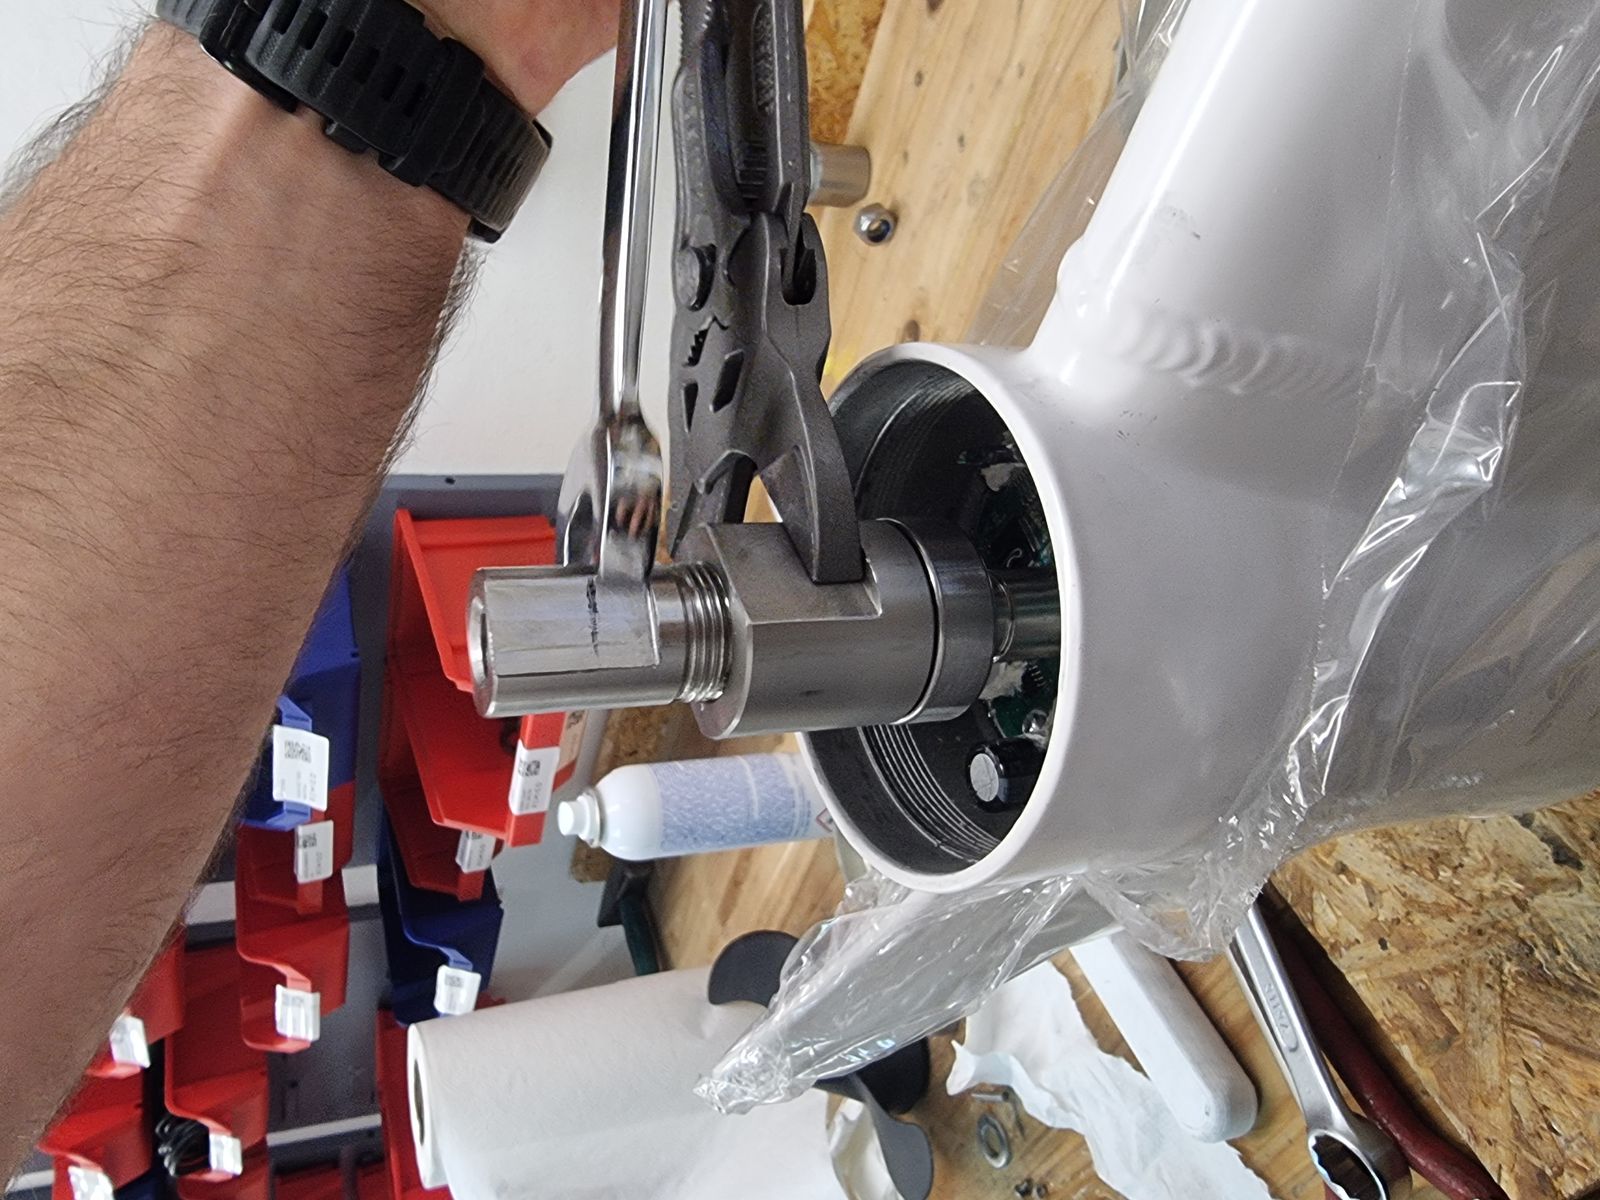
DT-ASM-019 STEP 19 - Press bearing onto shaft
Tools:
Installing parts:
Procedure:
- Position the bearing on the shaft.
- Slide the pressing sleeve over the shaft.
- Press the bearing down by threading the nut onto the shaft.
Link to originalCAUTION
Press only on the correct bearing ring. Incorrect pressing can damage the bearing.
DT-ASM-020 STEP 20 - Measure bearing depth
Tools:
Procedure:
Link to original
- Measure the bearing depth using a digital caliper.
- Bearing depth must be L = 68,2 mm.
DT-ASM-021 STEP 21 - Apply grease to bearing
Tools:
- No tools required.
Consumables:
Procedure:
Link to original
- Apply a moderate layer of grease on top of the bearing.
DT-ASM-022 STEP 22 - Install wave spring washer
Tools:
- No tools required.
Installing parts:
- Wave spring washer LMKAS 35A (011030005) (RemigoOne Go)
- Wave spring washer 35 NSSB-0138-L2 (016040003) (RemigoOne DE2)
Procedure:
Link to original
- Place the wave spring washer on the greased bearing.
DT-ASM-023 STEP 23 - Install O-ring into housing lid
Tools:
Installing parts:
- O-ring 70x4 (017010001)
- O-ring 78x1 (017010004)
- O-ring 35x2 NBR70 (017010006)
- Housing lid (040050001)
Procedure:
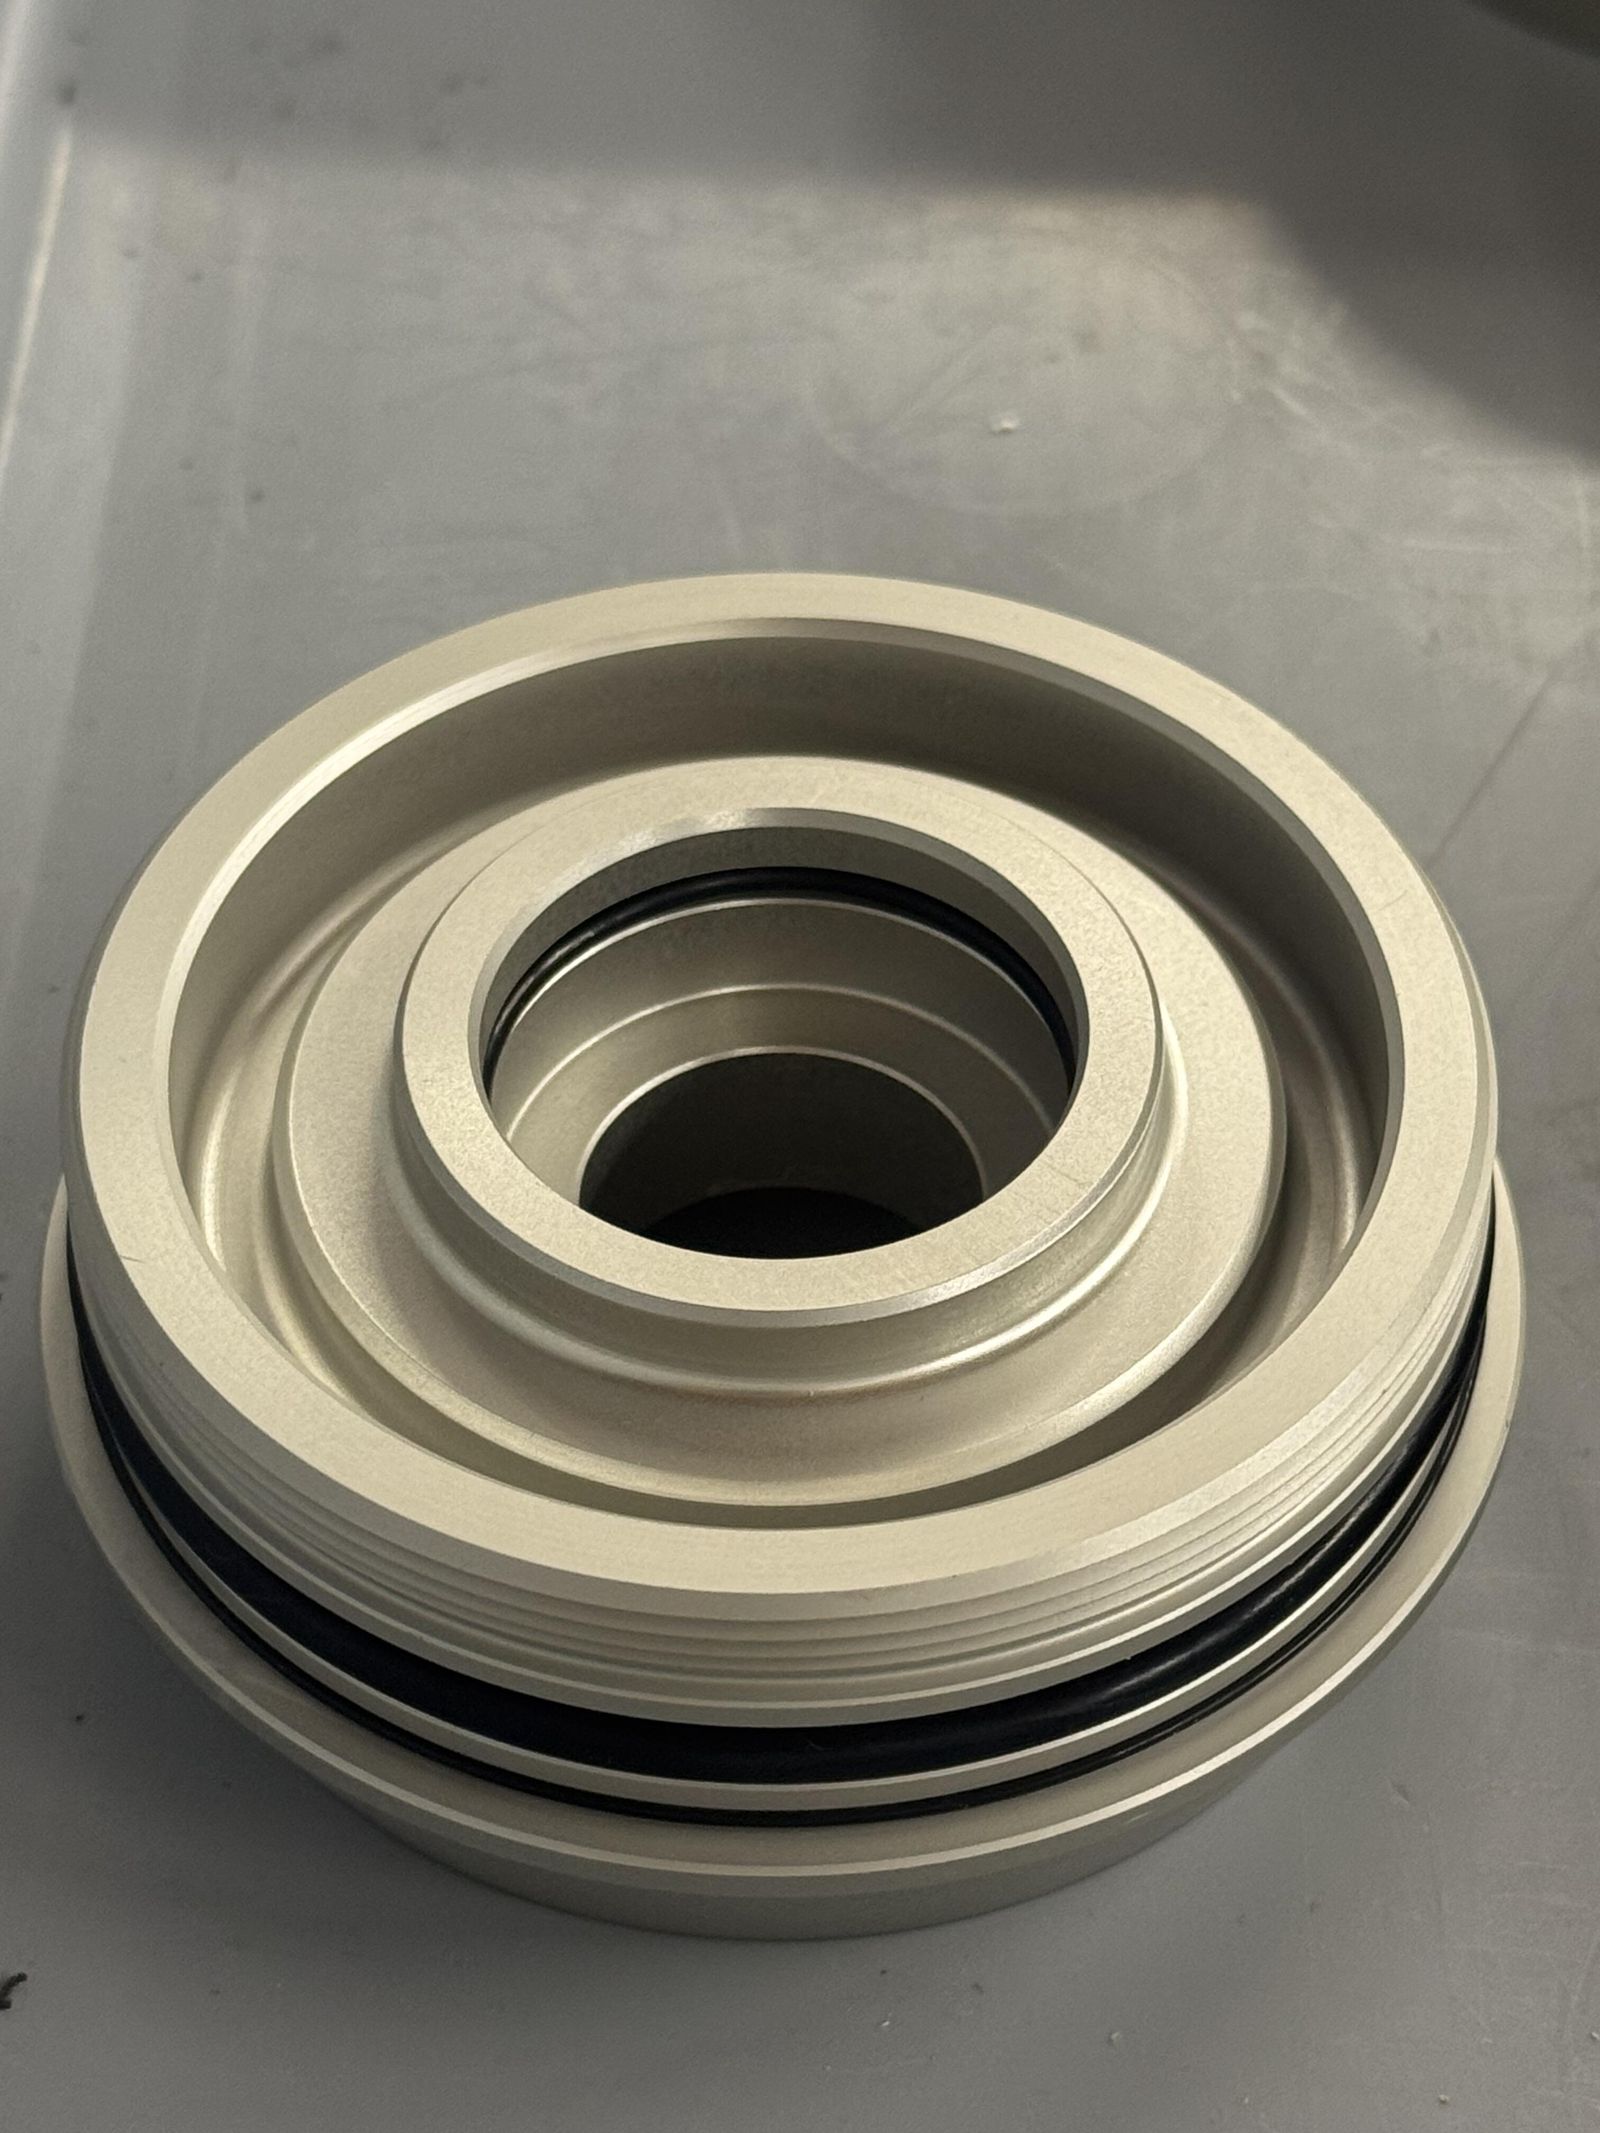
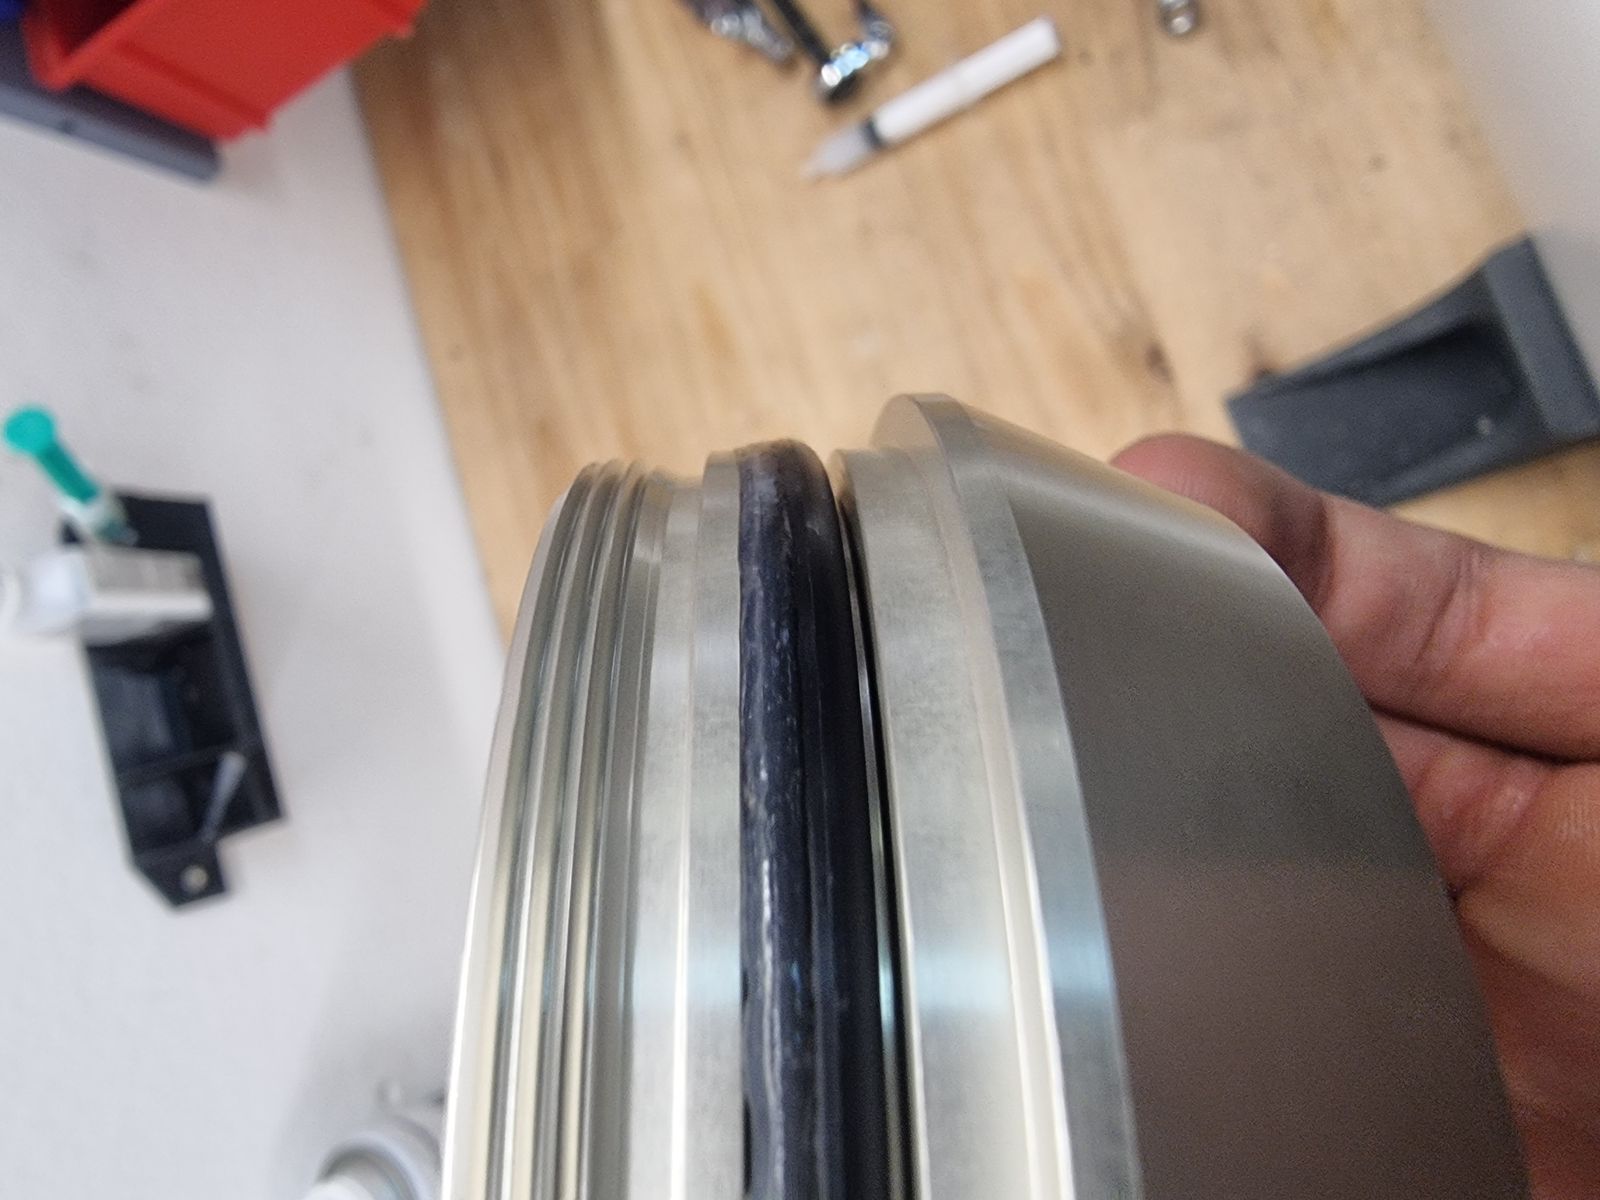
- Install O-ring 70x4 (017010001) and O-ring 78x1 (017010004) into the two grooves on the outer surface of the housing lid.
- Install O-ring 35x2 NBR70 (017010006) into the bearing seat groove on the inner surface of the housing lid.
- Use a pick for easier installation if needed.
Link to originalCAUTION
Do not cut, twist or overstretch the O-rings during installation. Make sure each O-ring is fully seated in its groove before proceeding.
DT-ASM-024 STEP 24 - Apply grease to O-ring and bearing contact surface
Tools:
- No tools required.
Consumables:
Procedure:
Link to original
- Apply a layer of grease on the bottom side of the O-ring.
- Apply a layer of grease on the bearing contact surface.
DT-ASM-025 STEP 25 - Install housing lid
Tools:
Installing parts:
Procedure:
- Align the housing lid with the motor housing and shaft.
- Use the bolting tool to align the motor lid with the threads on the housing.
- To achieve alignment, rotate the tool anticlockwise.
- Tighten until there is no gap between the lid and motor housing.
Link to originalCAUTION
Make sure the lid is correctly aligned before tightening to avoid damaging the threads.
DT-ASM-026 STEP 26 - Prepare radial shaft seals
Tools:
- No tools required.
Installing parts:
Consumables:
Procedure:
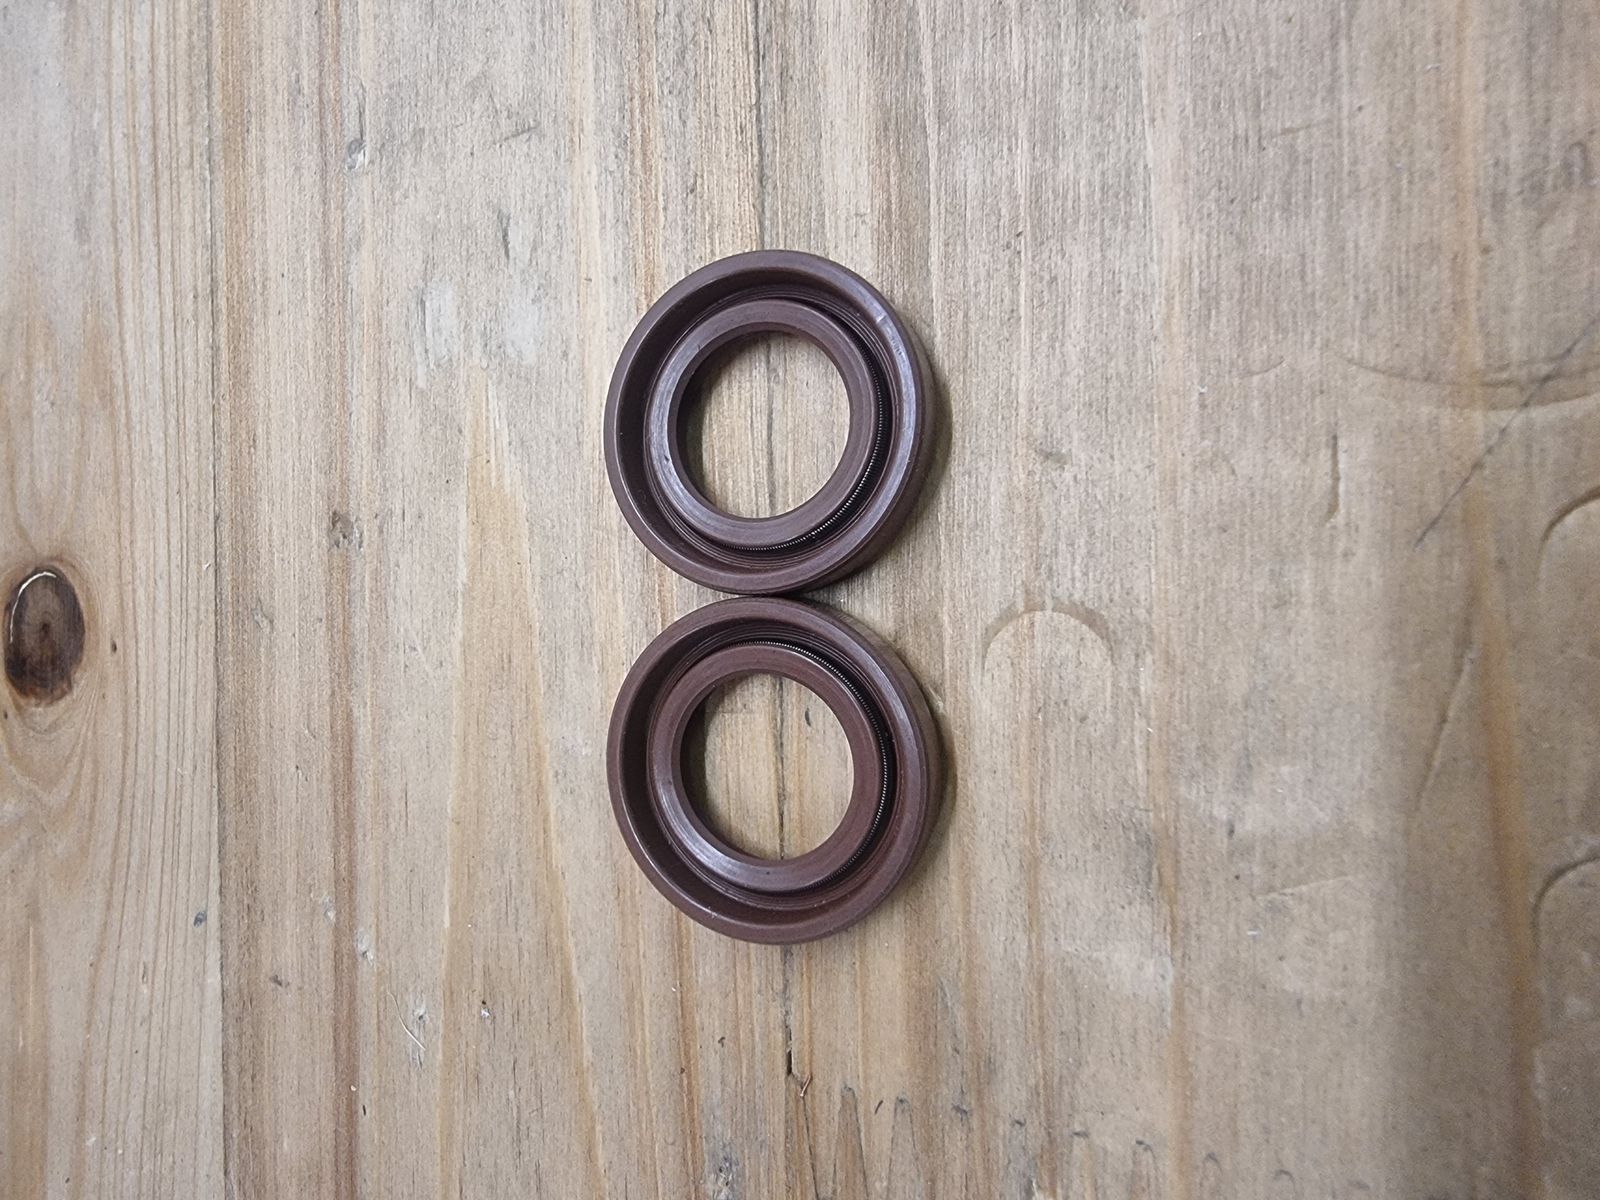
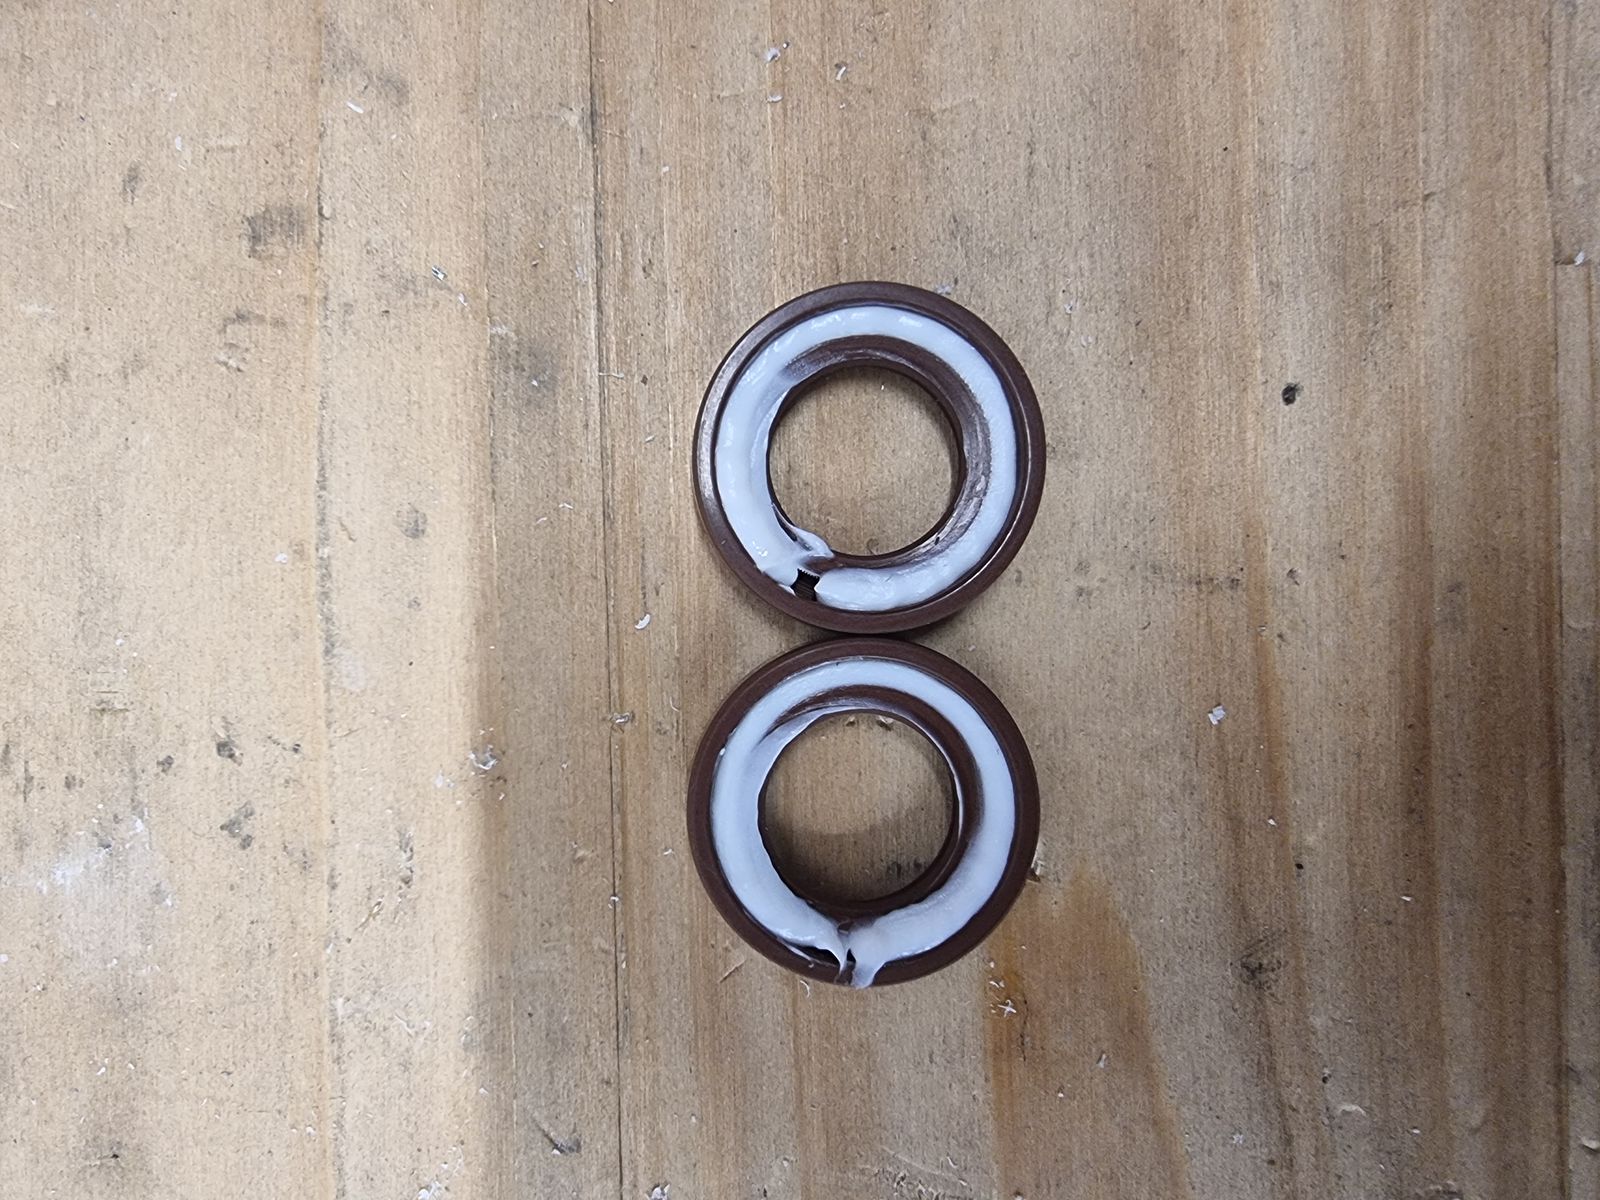
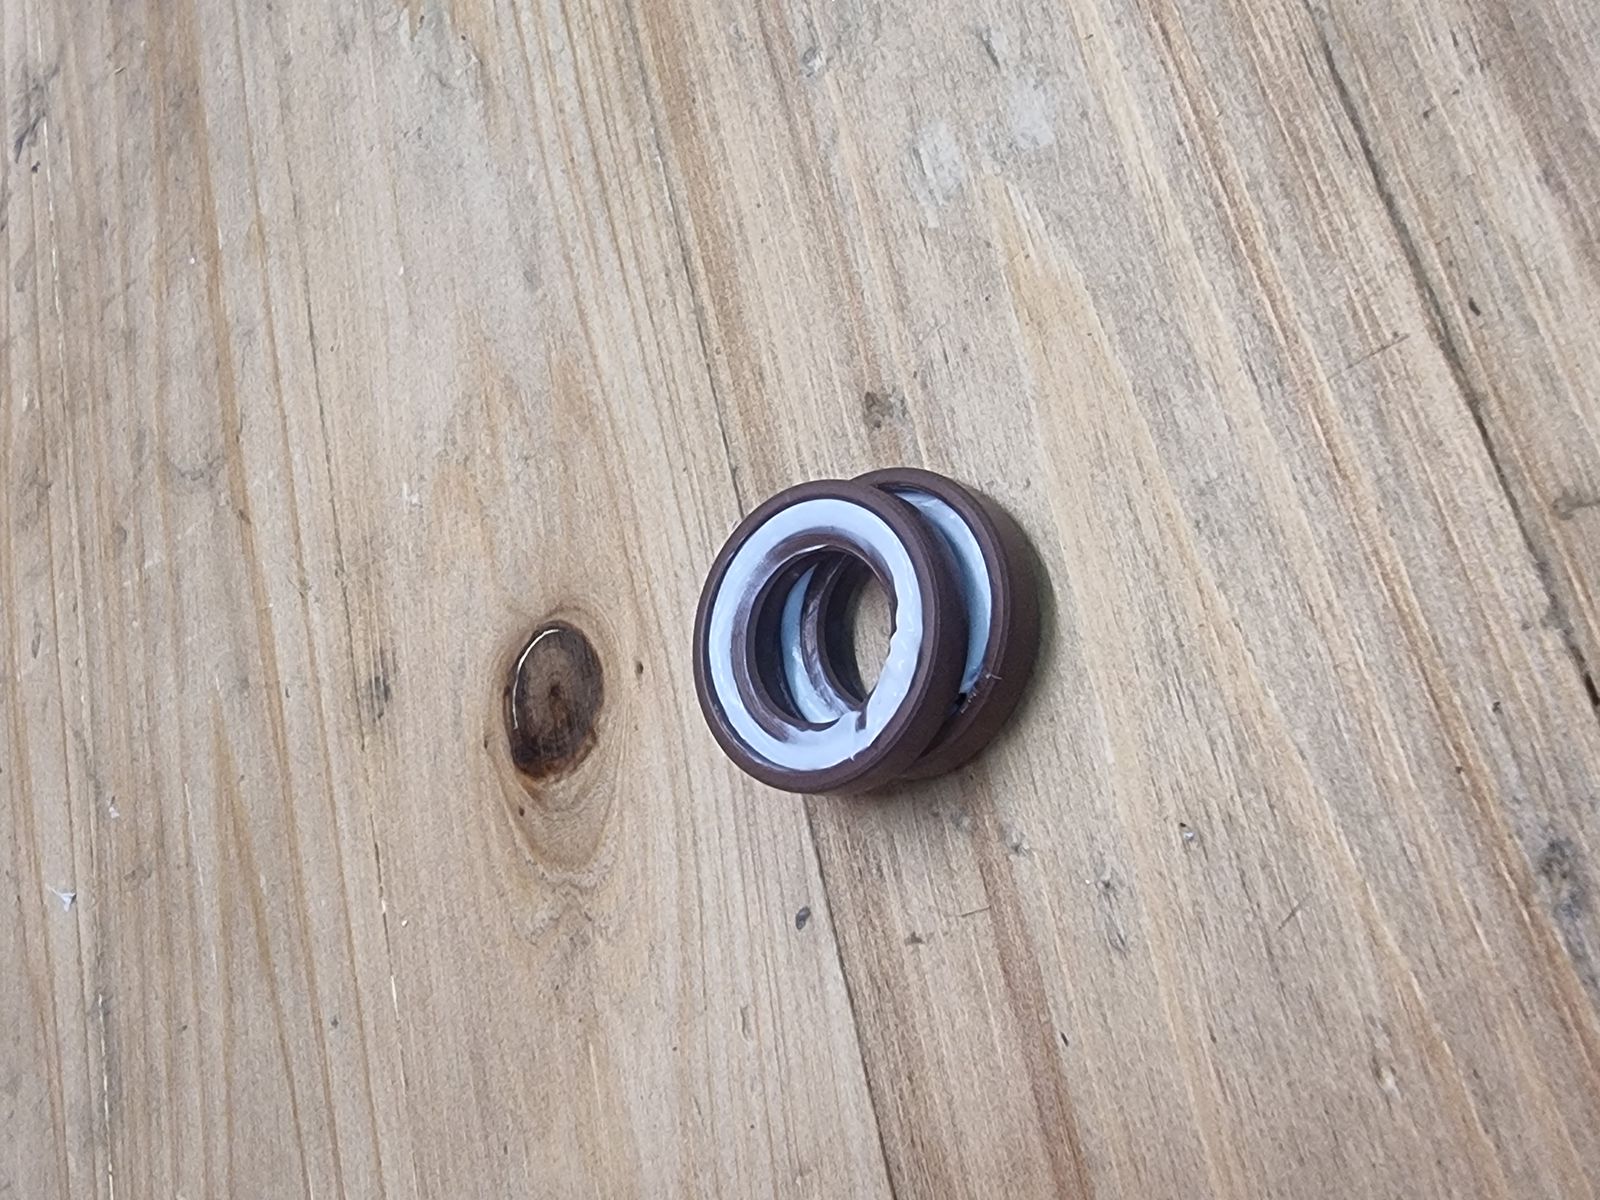
Link to original
- Apply O-ring grease to the grooved side of the radial shaft seals.
- Set the radial shaft seals in the upright position.
DT-ASM-027 STEP 27 - Check radial shaft seal orientation
Tools:
- No tools required.
Procedure:
- Make sure that the shaft seal groove is facing upwards.
Link to originalCAUTION
Incorrect shaft seal orientation can cause leakage.
DT-ASM-028 STEP 28 - Press radial shaft seals into housing lid
Tools:
Consumables:
Installing parts:
Procedure:
- Spray a small amount of silicone on the sleeve and on the outer sealing edge of the radial shaft seals.
- Slide the radial shaft seals onto the sleeve.
- Use the radial shaft seal press to push them until they are level with the housing lid.
Link to originalCAUTION
Press the radial shaft seals evenly to avoid deformation.
DT-ASM-029 STEP 29 - Inspect radial shaft seals
Tools:
- No tools required.
Procedure:
Link to original
- Visually inspect that the radial shaft seals are fully seated.
- Visually inspect that the radial shaft seals are installed in the correct orientation.
DT-ASM-030 STEP 30 - Install seal cover
Tools:
Consumables:
Installing parts:
Procedure:
- Place the seal cover in the recess of the housing lid.
- Apply one drop of Permabond A130 to the threads of each of the three screws.
- Tighten the three screws.
Torque specification:
Link to original
- Screws: 1,3 Nm
DT-ASM-031 STEP 31 - Install housing anode
Tools:
Consumables:
Installing parts:
Procedure:
- Align the housing lid and anode holes.
- Apply one drop of Permabond A130 to the threads of each of the three screws.
- Tighten the three screws.
Torque specification:
Link to original
- Screws: 1,3 Nm
DT-ASM-032 STEP 32 - Install washer and shear pin
Tools:
- No tools required.
Installing parts:
Procedure:
- Slide the washer onto the shaft with the sharp edge of the washer facing down.
- Slide the shear pin through the hole in the shaft.
Link to originalCAUTION
Make sure the shear pin is fully inserted before installing the propeller.
DT-ASM-033 STEP 33 - Install propeller and washer
Tools:
- No tools required.
Installing parts:
Procedure:
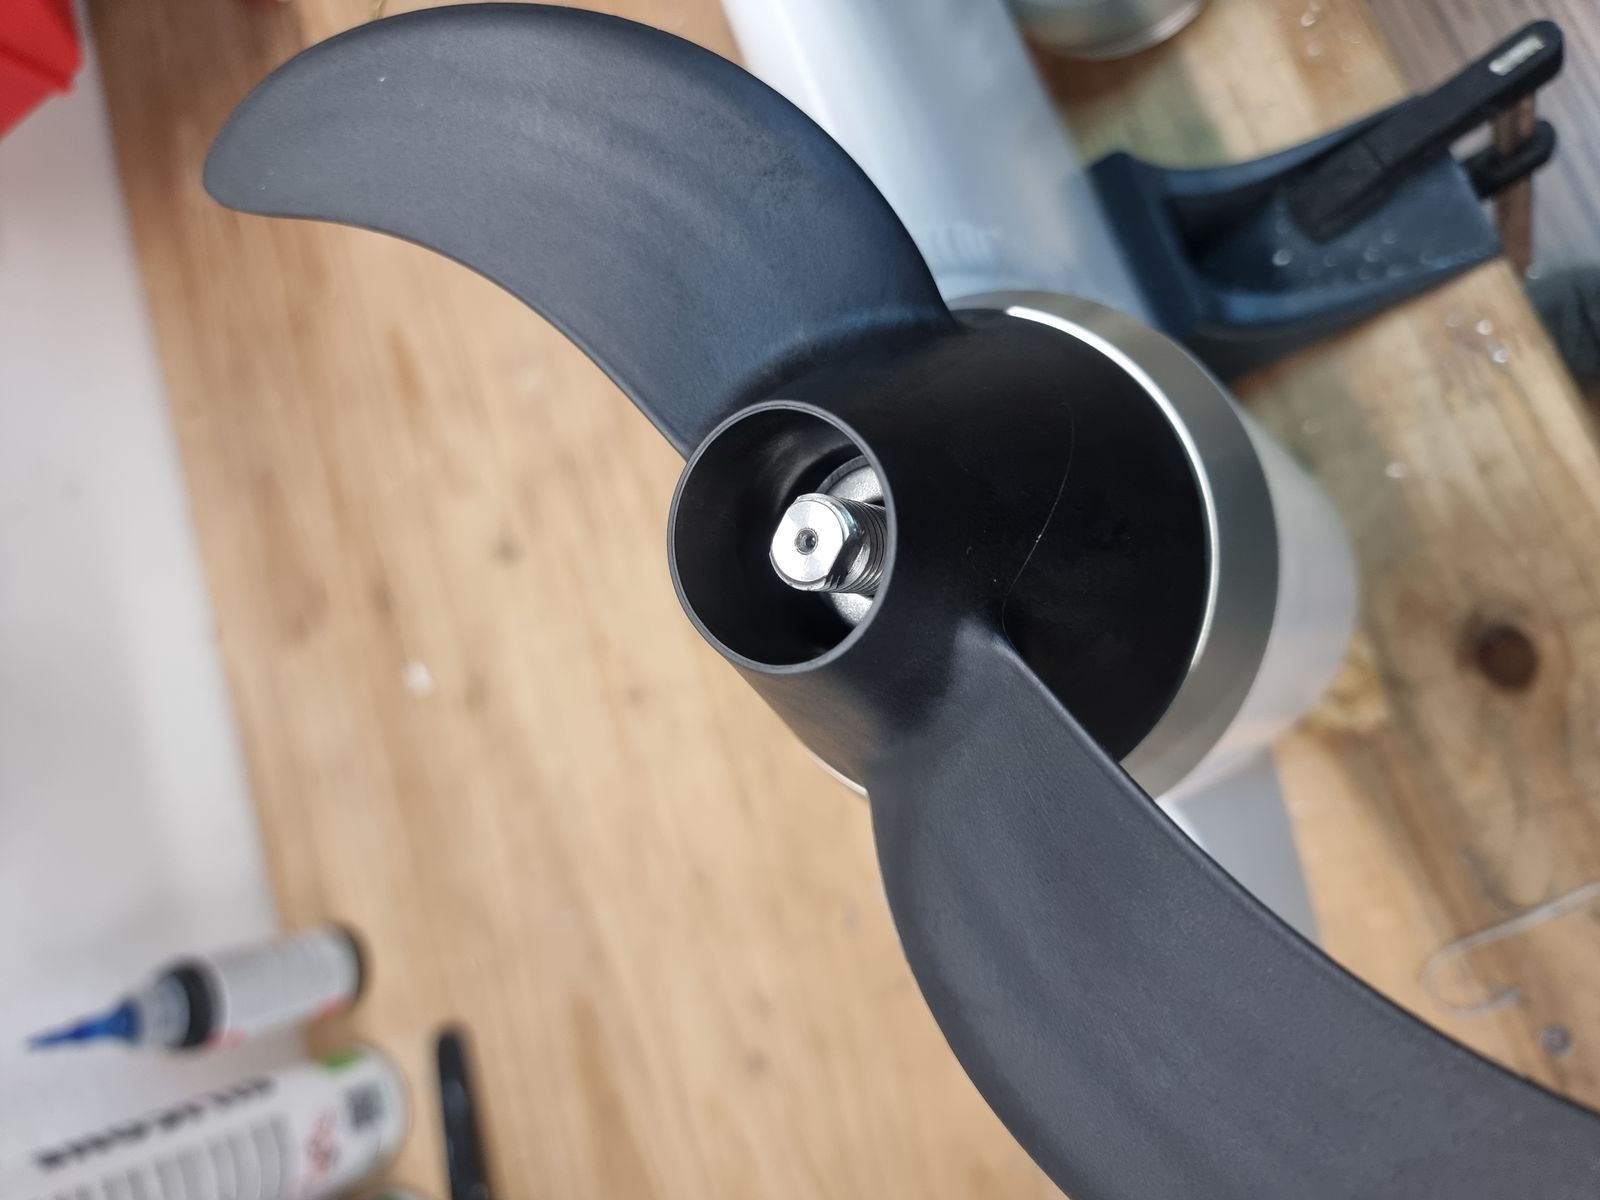
- Align the recess in the propeller with the shear pin.
- Slide the propeller onto the shaft.
- Slide the washer onto the shaft with the sharp edge of the washer facing down.
Link to originalCAUTION
Make sure the propeller is correctly seated on the shear pin before continuing.
DT-ASM-034 STEP 34 - Install safety nut and anode
Tools:
Installing parts:
Procedure:
- Install the safety nut until it bottoms out.
- Install the anode until it bottoms out.
CAUTION
Do not damage the shaft thread during installation.
The produced assembly is the Motor housing assembly.
Proceed to RemigoOne Go&DE2 Motor Assembly.
Link to original









Color key
Blue = Disassembly · Red = Check · Green = Reassembly